HeadPowder, a leading provider of industrial powder handling solutions, specializes in the design and implementation of efficient gray bin powder conveying systems. These systems are engineered to handle a wide range of bulk materials, ensuring reliable and safe material transport in various industrial applications. By integrating advanced technology with robust engineering, HeadPowder delivers systems that meet the specific needs of clients across different industries, including pharmaceuticals, chemicals, food processing, and more.
The Working Principle of Gray Bin Powder Conveying Systems
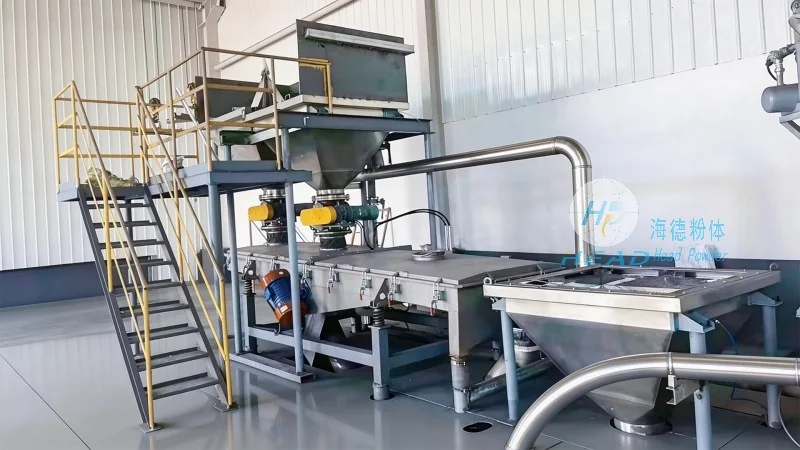
The operation of gray bin powder conveying systems is based on a systematic approach that combines mechanical and control technologies. The system typically consists of a gray bin (hopper) for material storage, a conveyor mechanism (such as screw conveyors, pneumatic conveying lines, or bucket elevators) for material transport, and a control unit for system management. The process starts with bulk materials being fed into the gray bin. The control unit then activates the conveyor, which moves the material through the system to the desired destination, such as a processing unit or storage silo. This continuous flow is maintained by the system's design, which ensures that material is consistently and evenly transported without interruption. The control unit monitors parameters like flow rate, pressure, and temperature to optimize performance and prevent issues like blockages or overloading.
Key Working Scene Characteristics of Gray Bin Powder Conveying Systems
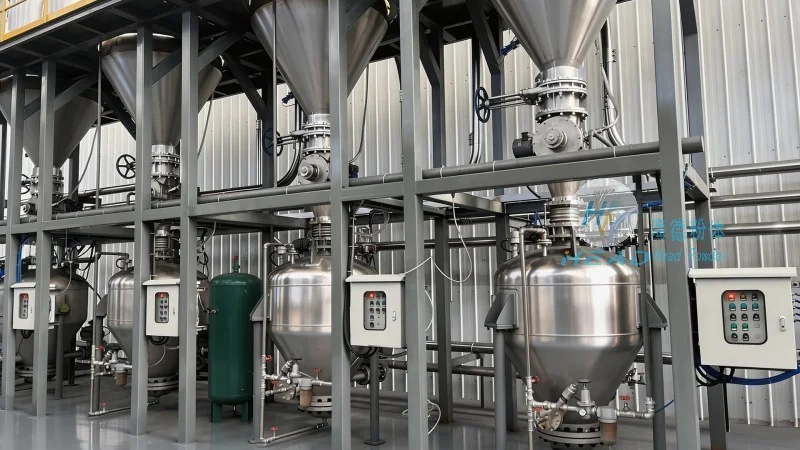
Gray bin powder conveying systems exhibit several notable characteristics that enhance their applicability in diverse industrial settings. Firstly, their compact and modular design allows for flexible installation, even in confined spaces, making them suitable for facilities with limited floor area. Secondly, the systems are equipped with advanced safety features, including overload protection, material flow sensors, and emergency stop mechanisms, to ensure operational safety and minimize the risk of accidents. Thirdly, the construction of the gray bin and conveyor components utilizes high-quality materials, such as stainless steel and corrosion-resistant alloys, which enhances durability and resistance to wear and tear, thereby extending the system's service life. Additionally, the modular nature of these systems facilitates easy integration with existing production lines and simplifies maintenance and repairs, reducing downtime and operational costs.
Application Scenarios and Benefits
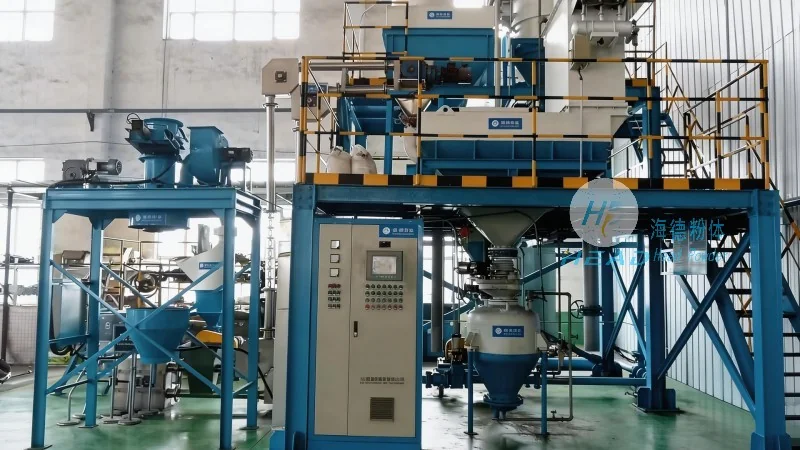
Gray bin powder conveying systems are widely used in various industrial applications due to their adaptability and efficiency. In the pharmaceutical industry, these systems are employed to handle sensitive powders, ensuring contamination-free transport and maintaining product quality. In the chemical sector, they are used to convey raw materials and finished products, supporting continuous production processes. The food processing industry also benefits from these systems, as they help maintain hygiene standards and prevent cross-contamination during material handling. The key benefits of gray bin powder conveying systems include improved operational efficiency, reduced material loss, enhanced safety, and lower maintenance costs, making them a preferred choice for businesses seeking reliable and cost-effective powder handling solutions.
Company Information
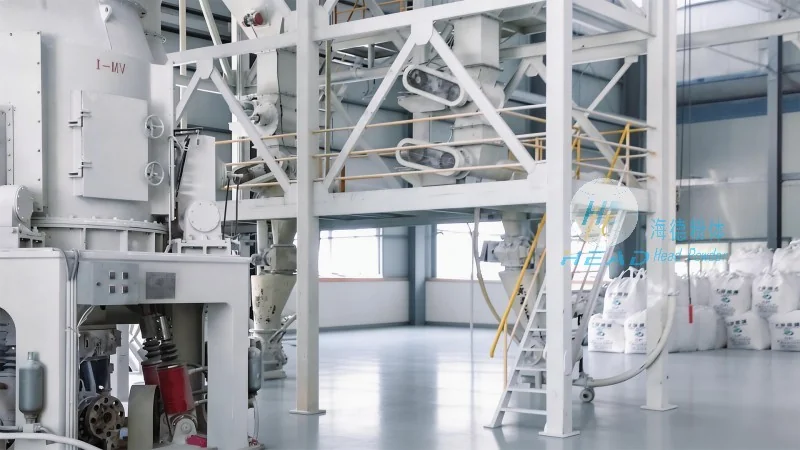
HeadPowder, the manufacturer of these systems, is a professional enterprise based in Shandong, China. As Shandong HeadPowder Engineering Co., Ltd., the company has a strong reputation for delivering high-quality industrial equipment tailored to client needs. With a focus on innovation and customer satisfaction, HeadPowder provides comprehensive solutions for powder handling, including system design, installation, and after-sales support. The company's commitment to quality and reliability has made it a trusted partner for businesses worldwide.




