Biological enzyme powder pneumatic conveying equipment is a specialized system designed for the efficient and safe transportation of powdered materials, particularly those containing biological enzymes. This equipment plays a crucial role in various industrial applications where the handling of sensitive or hygroscopic powders is required. The following sections will explore the working principle and key features of such equipment, providing insights into its functionality and benefits.
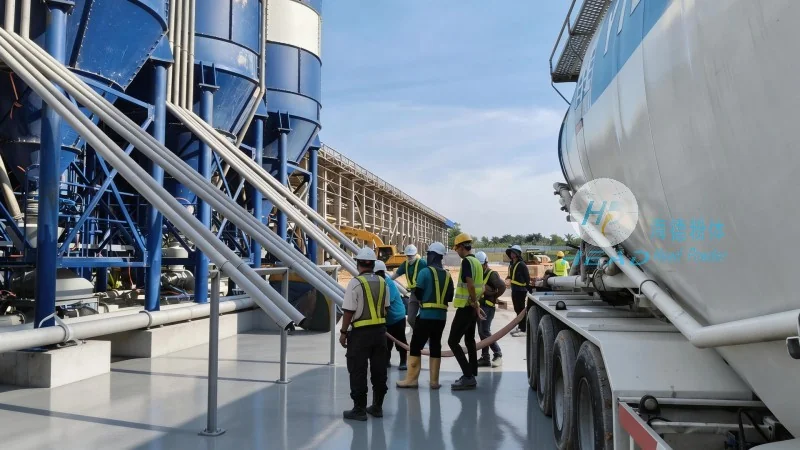
Overview of Biological Enzyme Powder Pneumatic Conveying Equipment
Biological enzyme powder pneumatic conveying equipment is engineered to transport powdered substances, especially those with biological enzymes, through a pressurized or vacuum system. The system typically consists of a hopper for material storage, a conveyor line, and a control unit that manages the flow and pressure. This equipment is widely used in industries such as pharmaceuticals, food processing, and biotechnology, where maintaining the integrity and stability of the enzyme powder is paramount.
The Working Principle of Biological Enzyme Powder Pneumatic Conveying Equipment
The core working principle of this equipment involves the use of air or gas to move the powder particles through a pipeline. The process generally operates under either positive pressure (pressure conveying) or negative pressure (vacuum conveying). In positive pressure systems, compressed air is introduced into the hopper, creating a pressure differential that forces the powder into the conveying line. The air and powder mixture then travels through the pipeline to the destination, where the powder is separated from the air and collected. In negative pressure systems, a vacuum is created at the discharge end, drawing the powder from the source into the pipeline. The air is then filtered and released, while the powder is deposited at the receiving point.
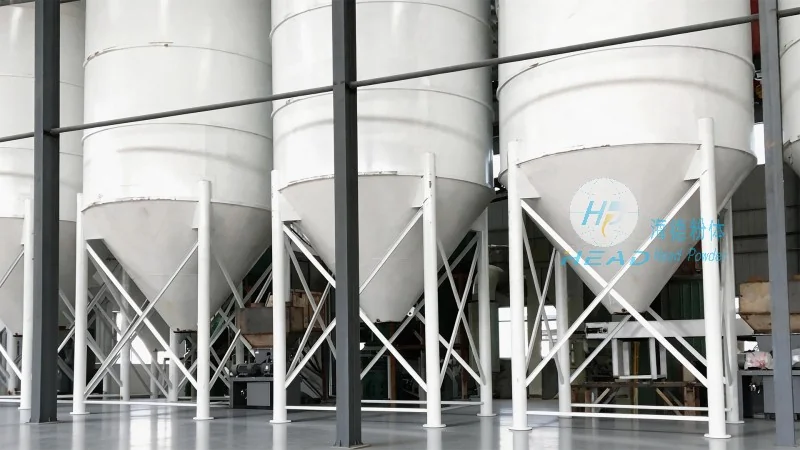
For biological enzyme powders, the conveying process must be carefully controlled to prevent degradation or contamination. The equipment is designed with materials that are non-reactive and easy to clean, ensuring that the enzyme's activity is preserved throughout the transportation process. Additionally, the system often includes temperature and humidity controls to maintain optimal conditions for the enzyme's stability.
Key Features of Biological Enzyme Powder Pneumatic Conveying Equipment
Several key features distinguish biological enzyme powder pneumatic conveying equipment from conventional systems. These features are tailored to meet the specific requirements of handling sensitive biological materials:
- Low Shear Design: The equipment is constructed with components that minimize mechanical stress on the powder particles. This is critical for maintaining the enzymatic activity of the biological material, as excessive shear can denature the enzymes.
- Airtight and Sterile Construction: The system is built with airtight seals and sterilizable materials to prevent contamination from external sources. This is essential in pharmaceutical and biotech applications where product purity is non-negotiable.
- Temperature and Humidity Control: The conveying process is often integrated with temperature and humidity control mechanisms to ensure that the enzyme powder remains within its optimal operational range. This helps in preserving the enzyme's activity and preventing moisture-related degradation.
- Flexible Conveying Paths: The equipment can be configured with flexible hoses or adjustable pipelines, allowing for complex and varied conveying routes. This flexibility is advantageous in facilities where space constraints or layout changes are common.
- Advanced Monitoring and Control: Modern systems incorporate sensors and control units that monitor parameters such as pressure, flow rate, and material level in real-time. This allows for precise control and immediate adjustments, ensuring efficient and reliable operation.
Applications and Benefits in Industrial Settings
Biological enzyme powder pneumatic conveying equipment is employed in a wide range of industrial applications where the efficient and hygienic handling of enzyme powders is essential. Some of the key benefits of using this equipment include:
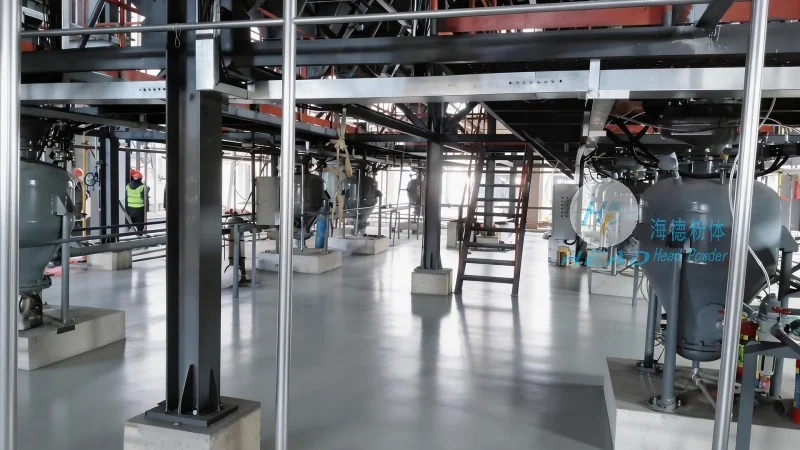
- Enhanced Product Integrity: By minimizing exposure to air, moisture, and mechanical stress, the equipment helps maintain the enzymatic activity and purity of the powder, leading to higher quality end products.
- Improved Safety and Hygiene: The sealed and sterile design reduces the risk of cross-contamination and exposure to hazardous materials, ensuring a safe working environment for operators.
- Increased Efficiency and Productivity: The automated control systems and efficient conveying processes reduce labor costs and increase throughput, contributing to higher overall productivity in industrial operations.
- Reduced Downtime and Maintenance: The robust construction and advanced monitoring features minimize equipment downtime and maintenance requirements, leading to lower operational costs over time.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer of specialized pneumatic conveying equipment for the handling of sensitive powders, including biological enzymes. With a strong commitment to quality and innovation, the company has established itself as a trusted partner in the pharmaceutical, food, and biotechnology industries. Headpowder's products are designed to meet stringent industry standards and regulatory requirements, ensuring that customers receive reliable and efficient solutions for their material handling needs.
Headpowder is headquartered in Shandong, China, and leverages advanced engineering and manufacturing capabilities to deliver high-performance equipment tailored to the unique demands of each application. The company's focus on customer satisfaction and technical excellence has earned it a reputation for delivering solutions that enhance operational efficiency and product quality.




