HeadPowder, a leading provider of industrial material handling solutions, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems. Among their product portfolio is the dry pebble powder pneumatic conveying line, a sophisticated equipment designed to efficiently transport dry pebble powders over long distances with minimal maintenance and operational costs. This article delves into the working principle and key features of this system, highlighting its advantages and practical applications in various industrial sectors.
Understanding the Working Principle of Dry Pebble Powder Pneumatic Conveying Line
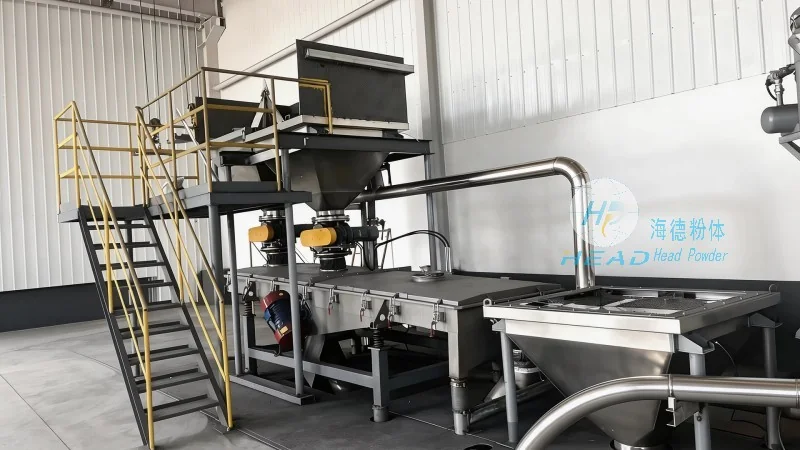
The dry pebble powder pneumatic conveying line operates on the principle of pneumatic transport, which involves the use of compressed air to move dry powders through a pipeline. The system typically consists of a hopper for material storage, a rotary valve for controlled discharge, a compressor to generate the necessary air pressure, and a pipeline network that transports the powder from the source to the destination. The process begins when the dry pebble powder is fed into the hopper. The rotary valve then regulates the flow of material into the pipeline, ensuring a consistent and controlled feed rate. Simultaneously, the compressor produces high-pressure air that is introduced into the pipeline, creating a flow that propels the powder particles forward. As the powder travels through the pipeline, it is suspended and carried by the air stream, allowing for efficient transportation without the need for mechanical components like belts or screws. The destination point, such as a silo or processing unit, is equipped with a receiver that captures the powder and releases the air, completing the cycle. This method of transport is particularly effective for dry pebble powders due to their particle size and density, which require a high-velocity air stream to maintain suspension and prevent clogging.
Key Features of the Dry Pebble Powder Pneumatic Conveying Line
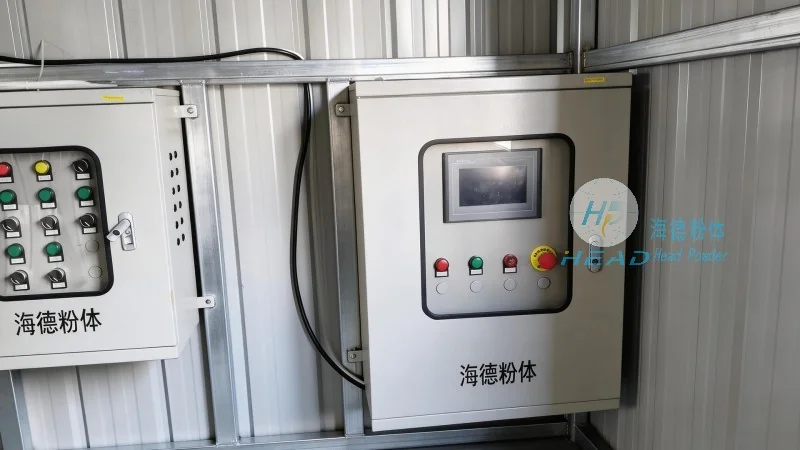
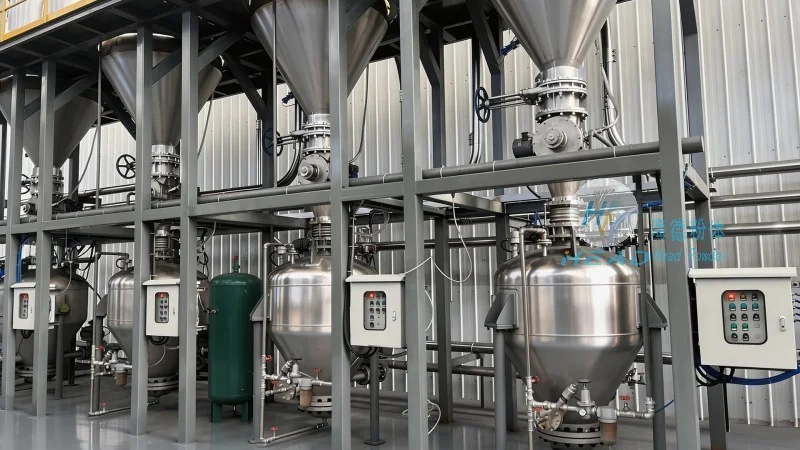
HeadPowder's dry pebble powder pneumatic conveying line is engineered with several distinctive features that enhance its performance and reliability. One of the primary features is its ability to handle a wide range of dry pebble powder types, including those with varying particle sizes and moisture content. The system is designed to maintain the integrity of the powder, preventing agglomeration or degradation during transport. Another notable feature is the adjustable air pressure and flow rate, which allows operators to optimize the conveying process based on the specific characteristics of the material being transported. This flexibility ensures efficient transport even with different powder properties. The equipment also incorporates advanced control systems that monitor pressure, flow, and material levels in real-time, providing operators with immediate feedback and enabling proactive maintenance. Additionally, the system is constructed with high-quality materials, such as stainless steel and corrosion-resistant components, to withstand the abrasive nature of pebble powders and ensure long-term durability. The modular design of the conveying line allows for easy installation and integration into existing industrial setups, reducing downtime and installation costs. Furthermore, the system is equipped with safety features, including pressure relief valves and emergency shut-off mechanisms, to prevent accidents and ensure safe operation. These features collectively make the dry pebble powder pneumatic conveying line a reliable and efficient solution for material handling in various industries.
Applications and Benefits in Industrial Settings
The dry pebble powder pneumatic conveying line is widely used in industries that require the transport of dry pebble powders, such as mining, construction, and chemical processing. In the mining industry, it is used to transport crushed pebbles from processing plants to storage facilities or to other processing units. In construction, it is employed to move pebble powders for concrete production or road construction projects. The chemical industry utilizes this system to transport pebble powders used in the manufacturing of coatings, pigments, and other chemical products. The primary benefits of this system include increased efficiency in material transport, reduced labor costs due to automated operation, and minimized environmental impact by eliminating the need for manual handling or open-air transport. Additionally, the system reduces the risk of dust exposure and contamination, as the powder is contained within the pipeline during transport. The low maintenance requirements and long service life of the equipment further contribute to cost savings for industrial operators. Overall, the dry pebble powder pneumatic conveying line offers a sustainable and efficient solution for handling dry pebble powders, meeting the demands of modern industrial operations.
About HeadPowder Engineering Co., Ltd.
HeadPowder Engineering Co., Ltd., headquartered in Shandong, China, is a reputable company specializing in the design and manufacturing of industrial material handling equipment. With years of experience in the field, HeadPowder has developed a strong reputation for delivering high-quality, reliable, and efficient pneumatic conveying systems. The company's commitment to innovation and customer satisfaction has enabled it to serve a diverse range of industries, including mining, construction, and chemical processing. HeadPowder's team of experts works closely with clients to understand their specific needs and provide tailored solutions that meet their operational requirements. The company's products, such as the dry pebble powder pneumatic conveying line, are designed to enhance productivity and reduce operational costs for industrial clients. HeadPowder's dedication to quality and customer service has made it a trusted partner for businesses seeking advanced material handling solutions. By leveraging advanced technology and rigorous quality control, HeadPowder ensures that its products meet the highest standards of performance and durability.




