Understanding the operation and advantages of corn husk powder pneumatic conveying systems is crucial for industries dealing with bulk powder handling. This article provides a detailed overview of the working principles and key characteristics of such systems, presented by Shandong HeadPowder Engineering Co., Ltd., a leading provider based in China.
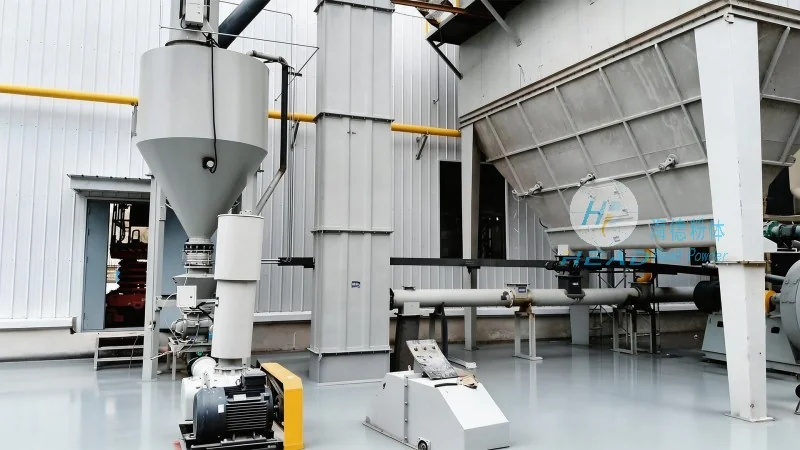
Overview of Corn Husk Powder Pneumatic Conveying Systems
Corn husk powder pneumatic conveying systems are engineered to transport dry, fine powders like corn husk through a pipeline using compressed air or other gas. These systems are widely utilized in agricultural processing, biomass energy production, and related sectors due to their efficiency and ability to handle delicate materials without causing degradation or contamination. They represent a modern alternative to traditional bulk handling methods, offering advantages in cleanliness, flexibility, and space efficiency.
Working Principle of the Pneumatic Conveying Line
The working principle of a corn husk powder pneumatic conveying line can be categorized into two main types: suction and pressure systems. In a suction system, a vacuum is created at the discharge end, drawing the corn husk powder from the feeding hopper through the pipeline. This method is ideal for short-distance transport and when the material is light and fine. Conversely, a pressure system uses compressed air to push the powder from the feeding point towards the discharge end, typically used for longer distances or when handling heavier particles. The system operates by introducing compressed air into the pipeline, which creates a pressure differential that propels the powder particles. The air velocity is carefully controlled to maintain a stable flow, ensuring that the powder remains entrained without settling or clogging the pipeline. Key components include a feeding hopper to introduce the powder, a pipeline network to guide the flow, a control valve to regulate air pressure and flow rate, and a discharge hopper to collect the material at the end of the line. The entire process is automated, with sensors monitoring air pressure, flow rate, and particle concentration to ensure consistent performance.
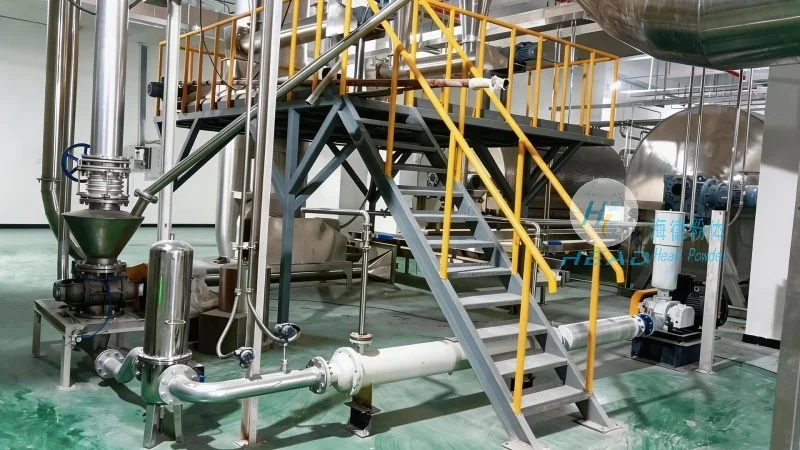
Key Features and Advantages
Several notable features distinguish corn husk powder pneumatic conveying systems from other material handling methods. First, they offer a closed-loop operation, which helps maintain product purity and prevents dust emissions into the environment. This is particularly important for corn husk powder, which can be prone to dusting and contamination if not handled properly. Second, the systems are highly flexible, allowing for changes in conveyor length, direction, and capacity by adjusting the pipeline configuration and air pressure. Third, they are relatively compact compared to traditional bulk handling equipment, making them suitable for installations with limited space. Additionally, the absence of mechanical components like belts or augers reduces maintenance requirements and extends the service life of the equipment. Another advantage is the ability to handle materials with varying particle sizes and moisture content, as the system can be adjusted to accommodate different material properties without significant modifications.
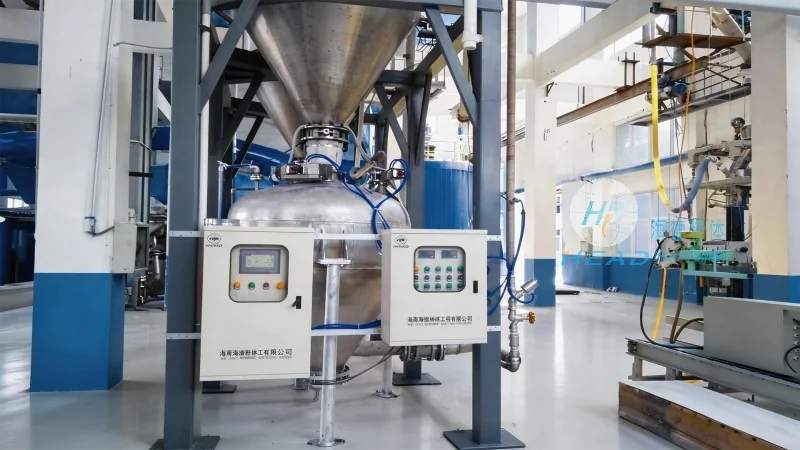
Application-Specific Considerations
When implementing a corn husk powder pneumatic conveying system, several factors must be considered to ensure optimal performance. The particle size and moisture content of the corn husk powder are critical, as they affect the air velocity required for stable transport. Larger or more moist particles may require higher air pressures to prevent settling or clogging. The system's design must also account for the specific handling environment, such as the need for explosion-proof components in areas where dust accumulation is a risk. Proper filtration and air cleaning systems are essential to maintain air quality and prevent dust buildup in the pipeline, which can reduce efficiency and cause operational issues over time. Additionally, the pipeline material and diameter must be selected based on the powder's abrasiveness and flow characteristics to minimize wear and ensure long-term durability.
Conclusion
Corn husk powder pneumatic conveying systems represent a sophisticated solution for the efficient and safe handling of agricultural byproducts. By leveraging compressed air to transport powder through a closed pipeline, these systems offer advantages in purity, flexibility, and space efficiency. As a manufacturer based in Shandong, China, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and supplying customized pneumatic conveying solutions tailored to the unique needs of corn husk processing facilities. Whether for biomass energy production, feed manufacturing, or other applications, such systems provide reliable performance and contribute to improved operational efficiency in the industry. The company's expertise in pneumatic conveying technology ensures that clients receive systems that are optimized for their specific processes, helping to enhance productivity and reduce operational costs.




