Lightweight micropowder material conveying lines are sophisticated systems designed to handle the transportation of fine, lightweight powders with precision and efficiency. These systems are crucial in various industrial applications, including pharmaceuticals, food processing, and chemical manufacturing, where the integrity and purity of the material must be maintained throughout the conveying process. The technology behind these lines combines advanced engineering principles with specialized components to ensure reliable operation under diverse operational conditions.
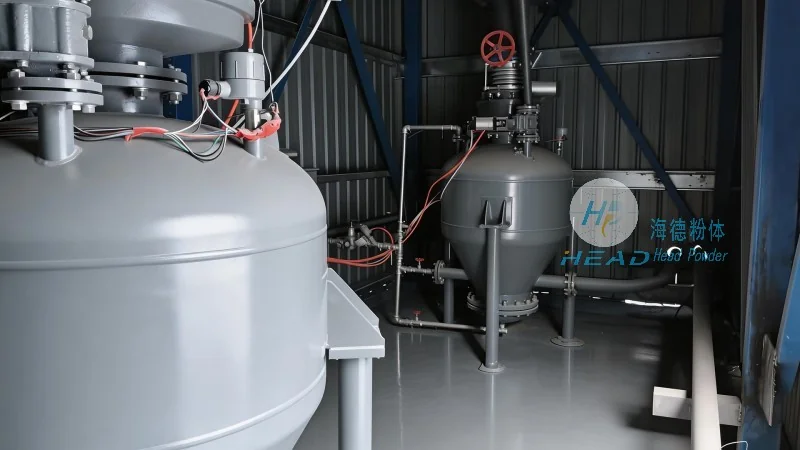
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and implementation of high-quality material handling solutions. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner in the industry, delivering tailored conveying systems that meet the unique requirements of clients worldwide. The company’s expertise lies in understanding the specific challenges associated with handling lightweight micropowders, such as dust control, material segregation, and energy efficiency, and addressing these through customized engineering solutions.
Working Principle of Lightweight Micropowder Material Conveying Lines
The core working principle of a lightweight micropowder material conveying line revolves around the use of specialized equipment to transport fine powders from one location to another while minimizing degradation or contamination. The system typically consists of several key components, including a feeding mechanism, a conveying device (such as a pneumatic or mechanical conveyor), and a control system. The feeding mechanism ensures that the micropowder is introduced into the system in a controlled manner, preventing overloading or blockages. The conveying device then uses air or mechanical force to move the material through the pipeline, maintaining a consistent flow rate. The control system monitors and adjusts the operation of the components in real-time, ensuring optimal performance and preventing operational issues such as clogging or pressure fluctuations.
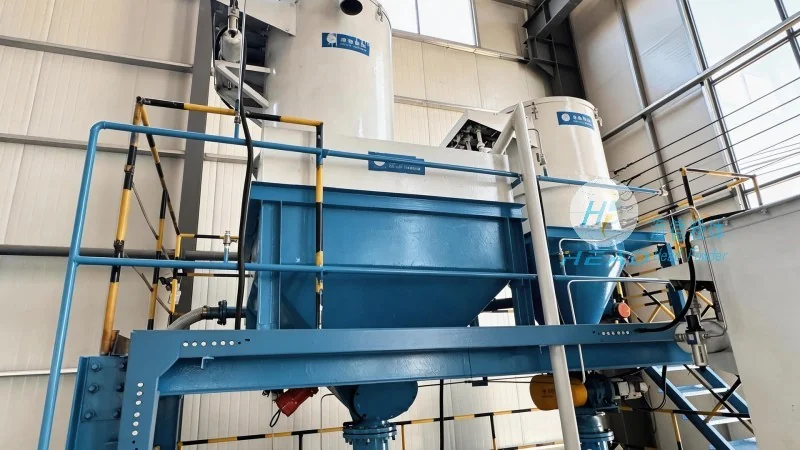
Key Features and Advantages of Lightweight Micropowder Material Conveying Lines
Lightweight micropowder material conveying lines offer several distinct features and advantages that make them ideal for demanding industrial applications. One of the primary advantages is their ability to handle fine, low-density powders without causing segregation or agglomeration. This is achieved through the use of gentle conveying methods, such as pneumatic conveying with low air velocity, which minimizes particle impact and maintains the material's uniformity. Another key feature is the system's high efficiency in terms of energy consumption, as advanced designs optimize air usage and reduce unnecessary losses. Additionally, these conveying lines are equipped with advanced filtration and dust control systems, ensuring that the material remains clean and free from contaminants, which is critical for applications where product purity is paramount. The systems also offer flexibility in terms of layout and integration, allowing them to be customized to fit existing facility configurations and operational requirements.
Technical Specifications and Performance Metrics
When evaluating lightweight micropowder material conveying lines, several technical specifications and performance metrics are crucial for understanding their capabilities. These include the conveying capacity, which is typically measured in terms of material flow rate (e.g., kg/h or ton/h), the maximum particle size that can be handled, and the system's pressure drop or energy consumption per unit of material transported. For example, a well-designed pneumatic conveying system may have a capacity of up to 10 tons per hour for certain lightweight powders, with a particle size range of 0.1 to 500 microns. The pressure drop across the system is another important factor, as it indicates the energy required to move the material through the pipeline. Modern systems often incorporate energy-saving designs, such as using pulse or dilute phase conveying methods, which reduce pressure drop and improve overall efficiency. Furthermore, the system's reliability and maintenance requirements are critical considerations, as downtime can significantly impact production schedules. HeadPowder's conveying lines are engineered with durable materials and easy-to-maintain components, ensuring long-term operational reliability and minimizing maintenance costs.
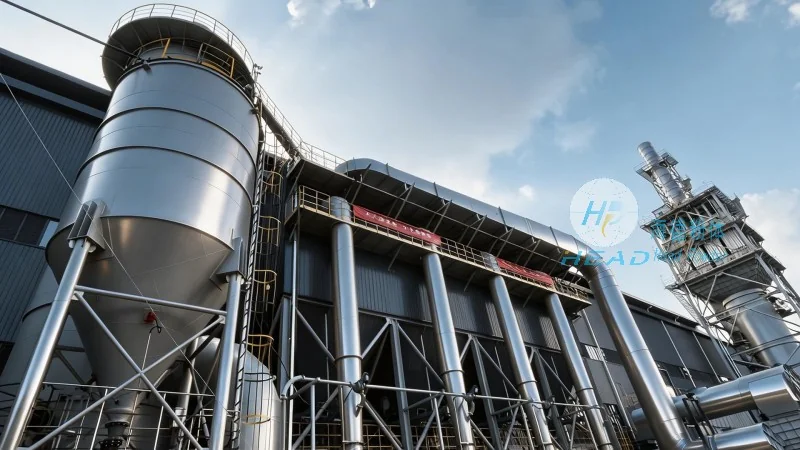
Applications and Industries Served
Lightweight micropowder material conveying lines are widely used across various industries due to their ability to handle delicate and sensitive materials. In the pharmaceutical industry, these systems are essential for transporting active pharmaceutical ingredients (APIs) and excipients, where contamination and particle degradation can affect product quality and safety. The food processing industry also relies on these lines for conveying ingredients like flour, sugar, and spices, ensuring that the final products meet strict quality and hygiene standards. In the chemical manufacturing sector, the systems are used to transport fine chemicals, pigments, and catalysts, where precise control over material flow is necessary to maintain reaction efficiency and product consistency. Additionally, these conveying lines are applied in the cosmetics industry for handling powders like talc and pigments, and in the agricultural sector for transporting fertilizers and pesticides. The versatility of the technology makes it suitable for a wide range of applications, from small-scale laboratory operations to large-scale industrial production lines.
Conclusion and Company Commitment
Lightweight micropowder material conveying lines represent a sophisticated solution for the efficient and reliable transportation of fine powders in industrial settings. By combining advanced engineering, specialized components, and rigorous quality control, these systems ensure that materials are handled with the utmost care, maintaining their purity and integrity throughout the conveying process. HeadPowder, with its headquarters in Shandong, China, continues to lead the industry in providing customized material handling solutions that meet the evolving needs of clients. The company's commitment to innovation, customer satisfaction, and operational excellence ensures that its conveying lines remain at the forefront of technology, delivering superior performance and reliability for years to come.




