Slurry and powder conveying systems are essential in various industrial applications, facilitating the efficient transport of particulate materials and liquid-solid mixtures. Understanding the core components and design principles of such systems is crucial for optimizing operational efficiency and ensuring reliable material handling. This article explores the fundamental aspects of slurry and powder conveying systems, focusing on their design considerations and the role of specialized engineering solutions.
Introduction to Slurry and Powder Conveying Systems
Slurry and powder conveying systems are engineered to transport materials that combine solid particles with a liquid medium, or purely dry powders. These systems are widely used in industries like mining, chemical processing, food production, and construction, where the movement of bulk materials is critical for production workflows. The primary goal of these systems is to move materials from one location to another with minimal loss, reduced downtime, and adherence to safety and environmental standards.
Key Components of a Slurry and Powder Conveying System
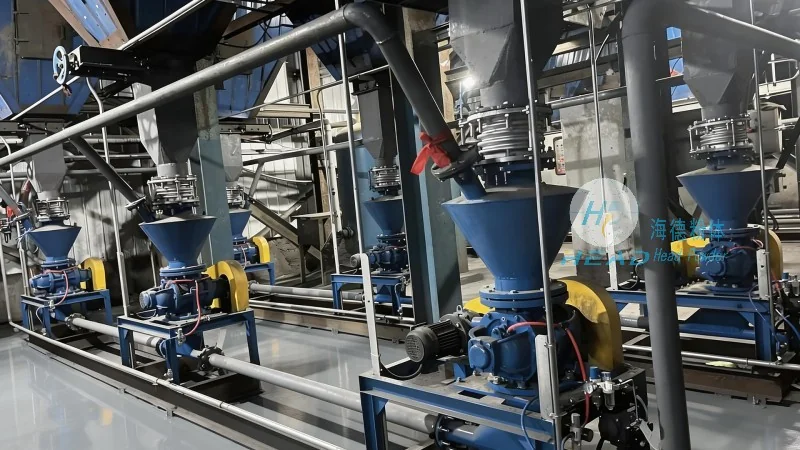
At the heart of a slurry and powder conveying system are several critical components that work in tandem to ensure smooth operation. These include the feed hopper, which holds the material to be conveyed; the pump or conveyor mechanism, which provides the necessary force to move the material; the pipeline or ductwork, which transports the material from the source to the destination; and the control system, which regulates the flow and pressure. Each component plays a vital role in maintaining the system's efficiency and reliability.
Design Principles for Optimal Performance
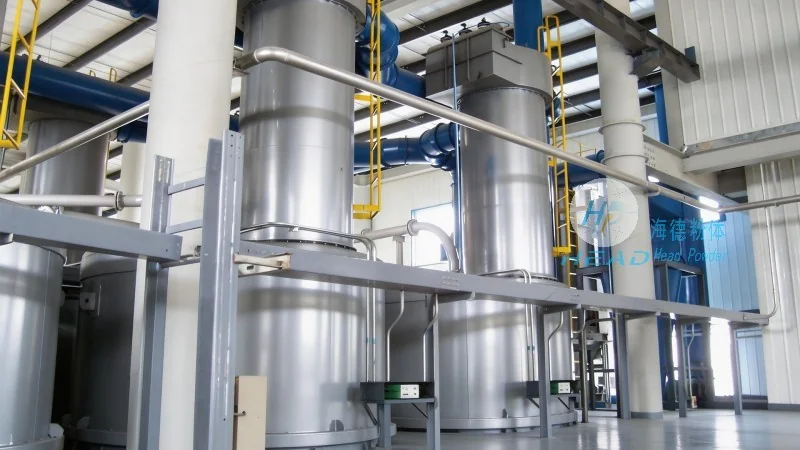
The design of a slurry and powder conveying system involves careful consideration of several factors to ensure it meets the specific requirements of the application. Key design principles include material compatibility, which ensures that the system components can withstand the chemical and physical properties of the conveyed material; flow rate optimization, which balances the speed of material transport with energy consumption; and system scalability, which allows for adjustments as production needs change. Additionally, the design must account for factors such as pressure drop, which affects the energy required to move the material, and wear resistance, which prolongs the system's lifespan.
HeadPowder Engineering's Expertise in Slurry and Powder Conveying
Shandong HeadPowder Engineering Co., Ltd., a leading provider of engineering solutions for material handling, specializes in designing and manufacturing slurry and powder conveying systems tailored to client needs. With years of experience in the industry, HeadPowder combines advanced technology with practical engineering to deliver systems that are efficient, durable, and cost-effective. The company's team of experts works closely with clients to understand their operational challenges and develop customized solutions that enhance productivity and reduce operational costs.
Customization and Integration in Slurry and Powder Conveying Systems
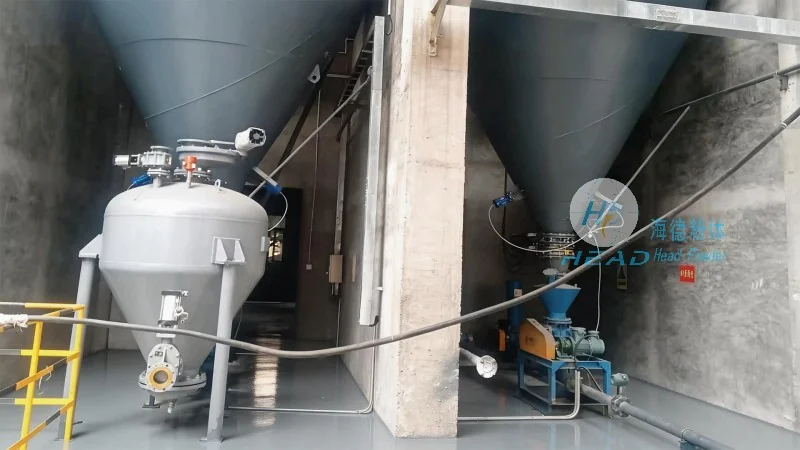
HeadPowder Engineering recognizes that each industrial application has unique requirements, which is why they offer customized slurry and powder conveying systems. These systems can be integrated with existing infrastructure or designed as standalone solutions, depending on the client's needs. The company's engineers use advanced simulation tools to model the system's performance before manufacturing, ensuring that the final product meets all specifications and performance targets. This approach minimizes risks and ensures that the system operates at peak efficiency from the start.
Benefits of Using a Professional Slurry and Powder Conveying System
Implementing a professional slurry and powder conveying system from HeadPowder Engineering offers numerous benefits. These include improved operational efficiency through optimized flow rates, reduced downtime due to reliable system performance, and lower maintenance costs thanks to durable components. Additionally, the systems are designed to minimize material loss and environmental impact, which is increasingly important in today's industrial landscape. By choosing HeadPowder Engineering, clients can expect a solution that not only meets current needs but also adapts to future growth and technological advancements.




