When it comes to handling and transporting powders in industrial settings, ensuring the integrity and quality of the material is paramount. This is where a nitrogen-protected powder handling system comes into play, offering a specialized solution to maintain the purity and stability of sensitive powders. In this article, we will explore what such a system entails and delve into its fundamental design principles.
Understanding the Nitrogen-Protected Powder Handling System
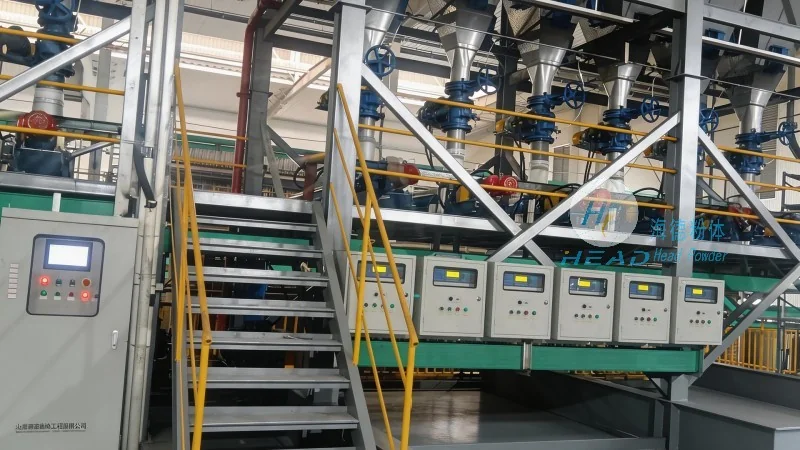
A nitrogen-protected powder handling system is a specialized setup designed to handle powders in an inert atmosphere, typically using nitrogen gas. The primary goal is to prevent contamination from oxygen, moisture, or other atmospheric elements that could degrade the powder's properties. This is especially critical for materials that are hygroscopic, oxidizable, or sensitive to environmental changes, such as pharmaceuticals, food additives, or high-value chemicals.
The Core Design Principles of the System
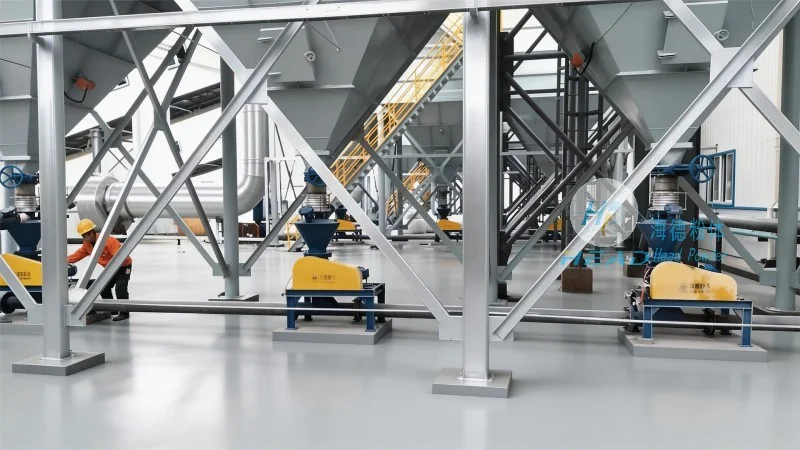
The design of a nitrogen-protected powder handling system revolves around several key principles to ensure effective operation and maintain the desired inert environment. First, the system must create and maintain a positive pressure differential, where the internal system pressure is higher than the ambient air pressure. This prevents external air from entering the system and contaminating the powder. Second, the system incorporates nitrogen gas as the inert medium, which is continuously circulated and filtered to remove any trace contaminants. Third, all components of the system, including hoppers, conveyors, and storage vessels, are designed with airtight seals and connections to minimize the risk of air infiltration. Additionally, the system may include pressure sensors and monitoring equipment to ensure the nitrogen level remains stable and within safe operating parameters.
Key Components and Their Functions
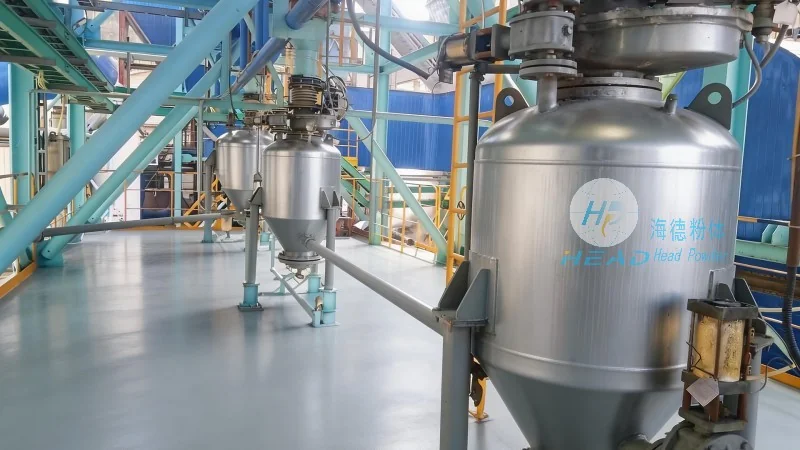
Several critical components work together to make a nitrogen-protected powder handling system effective. The storage hopper is typically equipped with a nitrogen inlet and a vent valve to maintain the inert atmosphere. The conveyor system, whether it's a screw conveyor, pneumatic conveyor, or bucket elevator, is designed to move the powder while keeping it under nitrogen pressure. The system also includes a nitrogen generator or supply unit to provide a continuous source of clean nitrogen gas. Filters and traps are installed to remove any particulate matter or moisture from the nitrogen stream, ensuring the gas remains pure. Finally, the control panel manages the entire system, monitoring pressure, flow rates, and nitrogen levels to ensure smooth and safe operation.
Benefits of Implementing a Nitrogen-Protected System
Adopting a nitrogen-protected powder handling system offers numerous advantages for industries dealing with sensitive powders. By maintaining an inert atmosphere, the system helps to preserve the powder's quality, extend its shelf life, and prevent unwanted chemical reactions. It also reduces the risk of fire or explosion in flammable powders, as the oxygen content is kept at a minimal level. Furthermore, the system enhances operational safety by minimizing exposure to hazardous materials and reducing the need for manual handling of powders. In terms of efficiency, the system can improve throughput by preventing clogging and ensuring consistent flow rates.
About Shandong HeadPowder Engineering Co., Ltd.
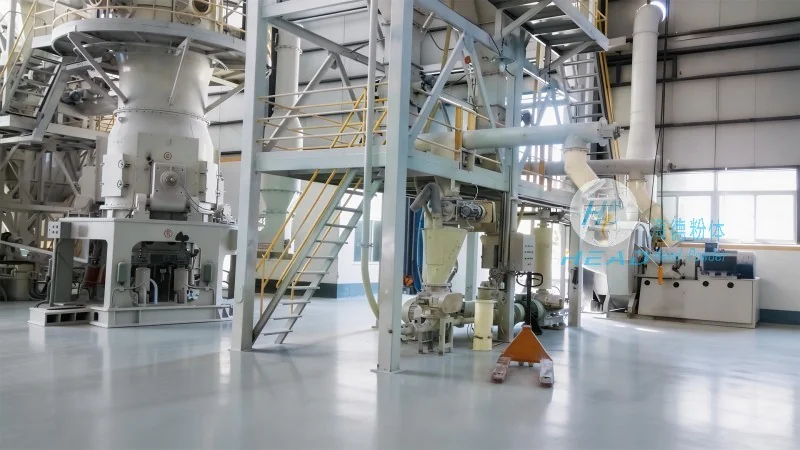
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer specializing in powder handling and processing solutions. With a focus on innovation and quality, HeadPowder provides comprehensive systems tailored to meet the specific needs of various industries. The company's headquarters is located in Shandong, China, where it leverages advanced technology and expertise to design and manufacture reliable nitrogen-protected powder handling systems. HeadPowder's commitment to customer satisfaction and product excellence has made it a trusted partner for businesses seeking to enhance their powder handling processes.




