Wheat pneumatic conveying systems are critical components in modern grain handling and processing operations. These systems efficiently transport wheat from storage silos, processing facilities, or storage areas to various points of use, such as milling plants, packaging lines, or distribution centers. The design of an effective wheat pneumatic conveying system requires careful consideration of several key factors, including material properties, system capacity, and operational efficiency. This article provides an overview of the design principles and considerations for wheat pneumatic conveying systems, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd., a leading provider in the field.
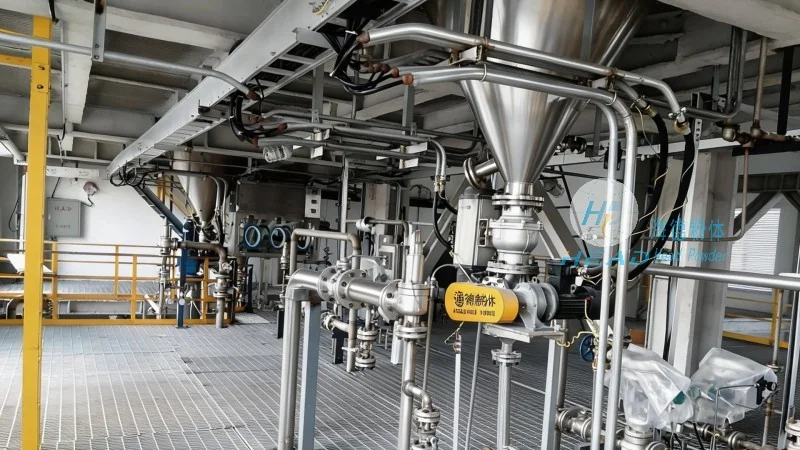
Company Overview: HeadPowder
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a renowned engineering firm specializing in the design, manufacturing, and installation of pneumatic conveying systems for the grain and food processing industries. With a strong presence in China, particularly in Shandong province, HeadPowder has built a reputation for delivering high-quality, reliable, and efficient solutions tailored to the unique needs of its clients. The company’s commitment to innovation and customer satisfaction has made it a trusted partner for businesses operating in the wheat and grain sector.
Key Design Considerations for Wheat Pneumatic Conveying
The successful design of a wheat pneumatic conveying system hinges on several critical factors. First, the physical properties of wheat, such as particle size, density, and moisture content, must be thoroughly analyzed. These characteristics influence the selection of appropriate conveying equipment, including the type of airlock, cyclone separator, and pipeline configuration. Second, the required system capacity and flow rate are essential parameters that determine the size of the blower, the diameter of the conveying lines, and the overall system layout. Third, energy efficiency is a major consideration, as pneumatic conveying systems can consume significant power. HeadPowder employs advanced engineering techniques to optimize energy usage while maintaining high conveying rates. Additionally, material handling safety and system durability are paramount, with designs that minimize wear and tear on components and ensure compliance with industry standards.
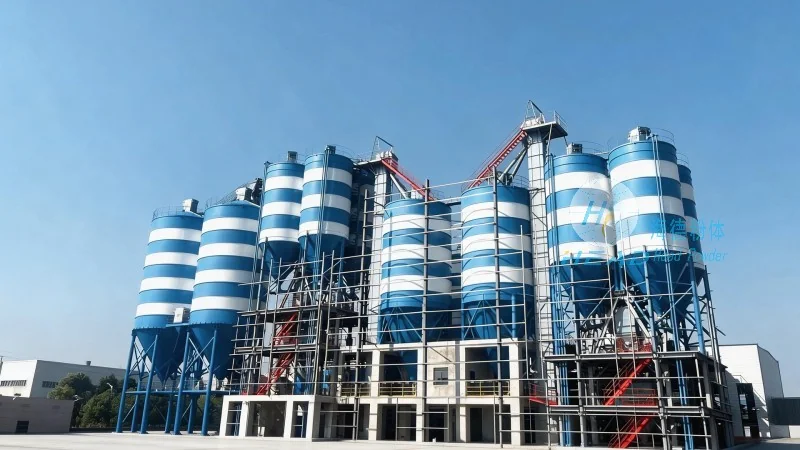
System Components and Their Functionality
A typical wheat pneumatic conveying system consists of several interconnected components, each playing a vital role in the overall operation. The primary components include a blower or fan to generate the necessary air pressure, airlocks to control the flow of wheat into the system, a conveying pipeline network to transport the material, cyclone separators to separate the wheat from the air, and a collection hopper or silo for the processed grain. The blower is responsible for creating the airflow that propels the wheat particles through the system. Airlocks, often equipped with rotary or slide gates, regulate the discharge of wheat from storage bins, preventing backflow and maintaining consistent material flow. The conveying pipeline, typically made of stainless steel or other corrosion-resistant materials, ensures the safe and efficient transport of wheat over long distances. Cyclone separators use centrifugal force to separate the wheat from the air stream, allowing the air to be recirculated or discharged while the wheat is collected in the hopper. Each component is carefully selected and sized based on the specific requirements of the wheat being conveyed and the operational parameters of the system.
Advantages of Pneumatic Conveying for Wheat Handling
Compared to traditional mechanical conveying methods, such as bucket elevators or belt conveyors, pneumatic conveying offers several advantages for wheat handling. One of the most significant benefits is the ability to transport wheat in a closed system, which minimizes dust emissions and prevents contamination from external sources. This is particularly important for food-grade wheat, where hygiene and safety are critical. Additionally, pneumatic systems can handle a wide range of particle sizes and moisture contents without causing damage to the grain. The flexibility of the system allows for easy integration with existing processing lines and can be adapted to accommodate changes in production volume. Another key advantage is the reduced need for maintenance, as the system has fewer moving parts compared to mechanical conveyors. HeadPowder’s designs incorporate durable materials and robust construction to ensure long-term reliability and minimal downtime.
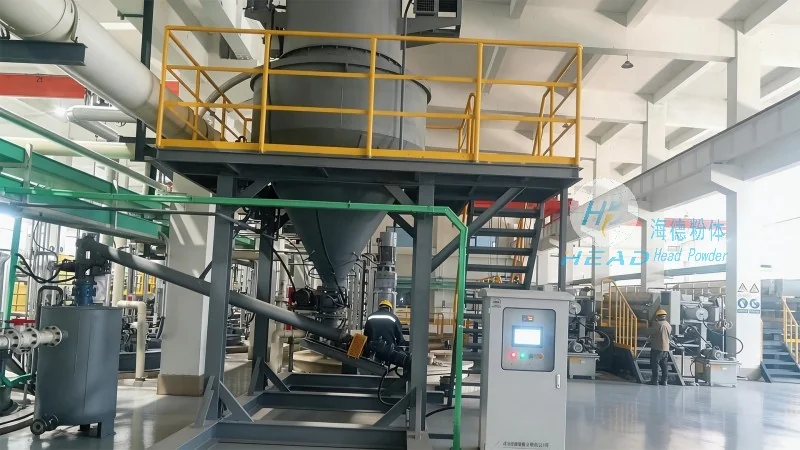
Customization and Integration Capabilities
HeadPowder understands that each wheat processing facility has unique operational requirements. Therefore, the company offers customized pneumatic conveying solutions tailored to the specific needs of its clients. Whether the goal is to increase production capacity, improve efficiency, or enhance safety, HeadPowder’s engineering team works closely with clients to develop a system that meets their exact specifications. The company’s expertise in system integration allows for seamless connection with existing equipment, such as storage silos, milling machinery, or packaging lines. This ensures a smooth transition and minimal disruption to ongoing operations. HeadPowder also provides comprehensive installation and commissioning services, ensuring that the system is properly set up and optimized for peak performance. The company’s commitment to after-sales support includes regular maintenance checks and technical assistance to address any issues that may arise during operation.
Conclusion and Contact Information
Wheat pneumatic conveying systems are essential for modern grain handling operations, offering efficiency, reliability, and safety. Shandong HeadPowder Engineering Co., Ltd. (HeadPowder) stands as a leading provider of these systems, leveraging its expertise and innovative designs to meet the diverse needs of the wheat and grain industry. By focusing on material properties, system capacity, and energy efficiency, HeadPowder delivers high-performance pneumatic conveying solutions that enhance productivity and operational excellence. For businesses seeking to optimize their wheat handling processes, HeadPowder offers customized, reliable, and efficient systems designed to meet the highest standards of quality and performance.




