This equipment is specifically designed for the efficient and reliable transportation of phenolic resin powders through pneumatic conveying systems. As a critical component in industrial material handling, it plays a vital role in processes where traditional bulk handling methods may be insufficient or impractical. The system is engineered to maintain the integrity of the phenolic resin powder, preventing agglomeration and ensuring consistent flow characteristics essential for downstream applications.
Structural Components and Working Principles
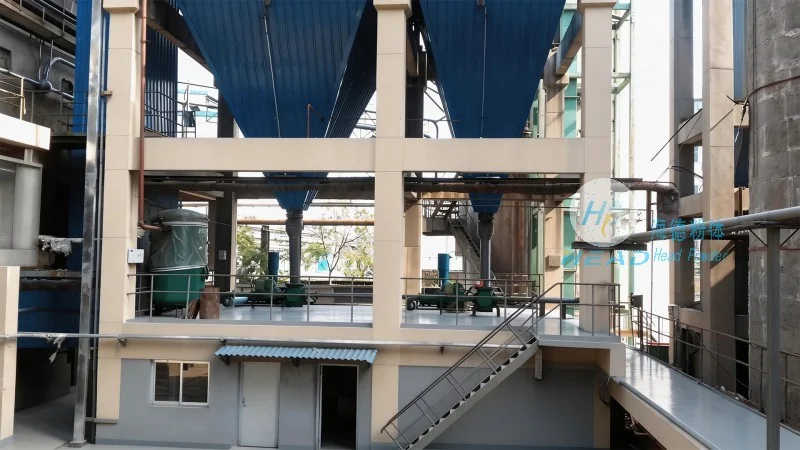
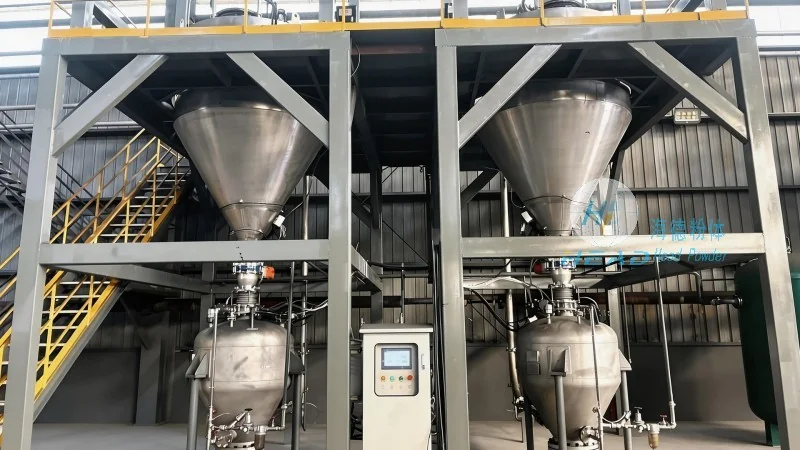
The pneumatic conveying system for phenolic resin powders typically consists of several key components, including a hopper for material storage, a rotary valve for controlled discharge, a conveying pipeline, a blower or air compressor to generate the necessary airflow, and a receiver for the delivered material. The working principle involves feeding the phenolic resin powder into the hopper, where it is then metered out by the rotary valve. The blower then introduces high-velocity air into the pipeline, creating a flow that carries the powder particles through the system. The powder is transported to the receiver, where the air is separated from the material, often through a cyclone or filter system, before the powder is collected.
Company Information and Background
HeadPowder, the manufacturer of this equipment, is a professional engineering company based in Shandong, China. With a focus on providing high-quality material handling solutions, the company specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored to various industrial needs. HeadPowder Engineering Co., Ltd. leverages advanced engineering techniques and rigorous quality control measures to ensure that its products meet the stringent requirements of the phenolic resin industry, offering durability, efficiency, and reliability in material transport operations.
Technical Specifications and Application Scenarios
The equipment is designed to handle phenolic resin powders efficiently, ensuring stable and reliable material transport. Key technical specifications may include adjustable airflow rates, variable conveying capacities, and robust construction to withstand the abrasive nature of phenolic resin powders. It is commonly used in applications such as resin storage and distribution in manufacturing plants, where the equipment facilitates seamless integration into production lines. The system's ability to maintain the purity and consistency of the phenolic resin powder makes it ideal for applications requiring high-quality material handling, such as in the production of composite materials, adhesives, and other industrial products.
Advantages and Operational Considerations
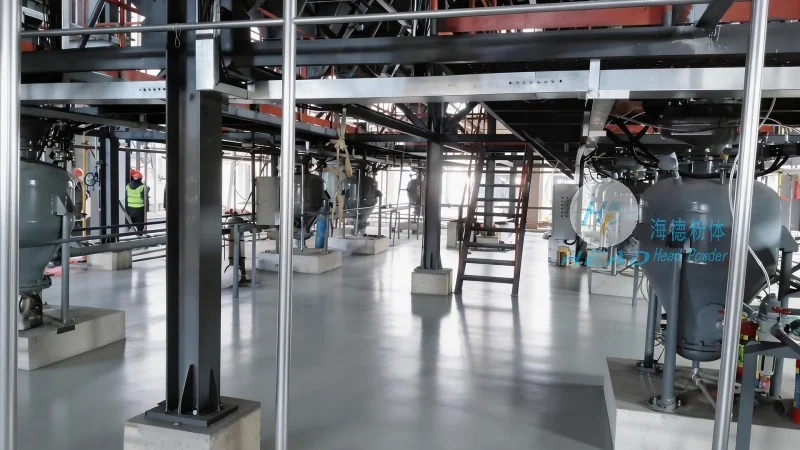
One of the primary advantages of this pneumatic conveying system is its ability to transport phenolic resin powders over long distances without the need for mechanical components like belts or chains, reducing maintenance requirements and operational costs. Additionally, the system can handle varying particle sizes and moisture content, making it versatile for different phenolic resin formulations. Operational considerations include regular maintenance of the blower and air filtration systems to prevent dust accumulation and ensure consistent airflow. Proper calibration of the rotary valve and hopper levels is also crucial to maintain stable conveying rates and prevent material blockages in the pipeline.




