HeadPowder, a leading manufacturer in the field of powder handling technology, specializes in providing advanced pneumatic conveying solutions for various industrial applications. This article focuses on the operation process and working principle of a specialized bean cake powder pneumatic conveying system, highlighting its efficiency, reliability, and key components.
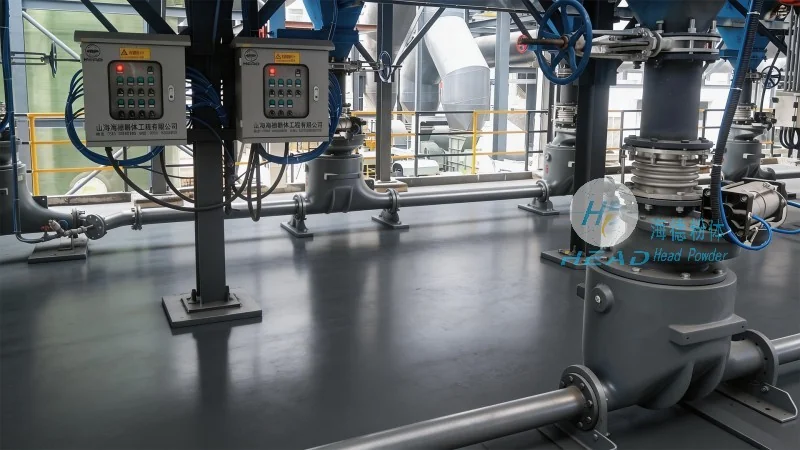
Introduction to Bean Cake Powder Pneumatic Conveying Equipment
Bean cake powder, a byproduct commonly used in the food and agricultural industries, requires efficient and hygienic handling to maintain product quality and prevent contamination. Pneumatic conveying systems offer a cost-effective and flexible solution for transporting such powders over short to medium distances. The equipment from Shandong HeadPowder Engineering Co., Ltd. is designed to meet these demands, ensuring smooth and controlled material transfer.
Key Components of the Pneumatic Conveying System
The bean cake powder pneumatic conveying system typically consists of several critical components that work in tandem to achieve effective material transport. These include a hopper for material storage, a rotary valve or feeder to control the flow rate, a compressor or blower to generate the air pressure, a pipeline network for conveying the material, and a receiver or discharge unit for the final product. Each component plays a vital role in the overall operation, contributing to the system's performance and durability.
Working Principle of the Pneumatic Conveying Process
The operation of the bean cake powder pneumatic conveying system is based on the principle of air suspension, where the material is lifted and transported through the pipeline by the force of compressed air. The process begins with the material being fed into the hopper from the source. The rotary valve then regulates the flow of the powder into the pipeline, ensuring a consistent and controlled discharge rate. Simultaneously, the compressor generates high-pressure air, which is introduced into the pipeline at the inlet of the hopper. As the air flows through the pipeline, it creates a low-pressure zone that draws the powder particles into the air stream. The air and powder mixture then travels through the pipeline to the discharge point, where the material is separated from the air using a cyclone separator or a filter system. The separated powder is collected in the receiver, while the air is either vented to the atmosphere or recycled back into the system for energy efficiency.
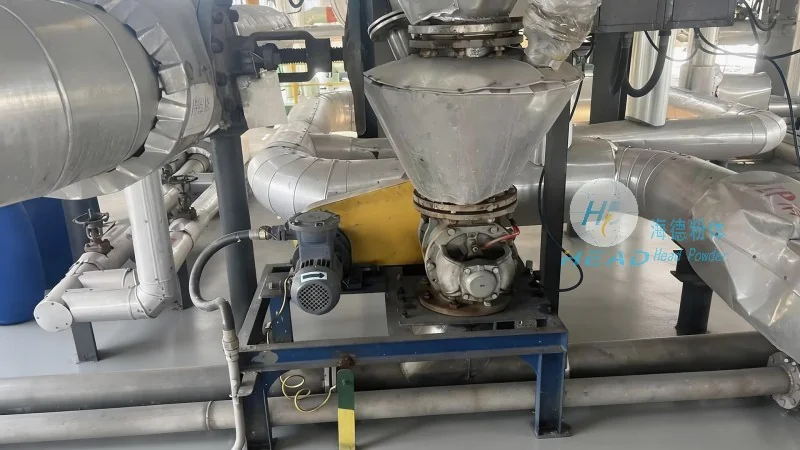
Operation Process: Step-by-Step Overview
The operation process of the bean cake powder pneumatic conveying equipment involves several sequential steps that ensure smooth and continuous material transfer. The first step is the preparation phase, where the hopper is filled with the bean cake powder, and the system is checked for any leaks or obstructions. The second step is the start-up phase, where the compressor is activated, and the air pressure is adjusted to the optimal level for conveying the powder. The third step is the material feeding phase, where the rotary valve is set to the desired flow rate, and the powder is fed into the pipeline. The fourth step is the conveying phase, where the air and powder mixture travels through the pipeline to the discharge point. The fifth step is the separation and collection phase, where the powder is separated from the air and collected in the receiver. The final step is the shutdown phase, where the system is turned off, and the remaining powder is emptied from the hopper and pipeline.
Advantages of Using Pneumatic Conveying for Bean Cake Powder
Compared to traditional mechanical conveying methods, pneumatic conveying offers several advantages for handling bean cake powder. These include reduced product contamination due to the enclosed system, lower maintenance costs as there are fewer moving parts, and the ability to transport materials over longer distances with minimal loss. Additionally, the system can be easily integrated with other processing equipment, such as mixers or classifiers, to form a complete production line. The flexibility of the system allows for adjustments in flow rate and pressure to accommodate different material characteristics and production requirements.
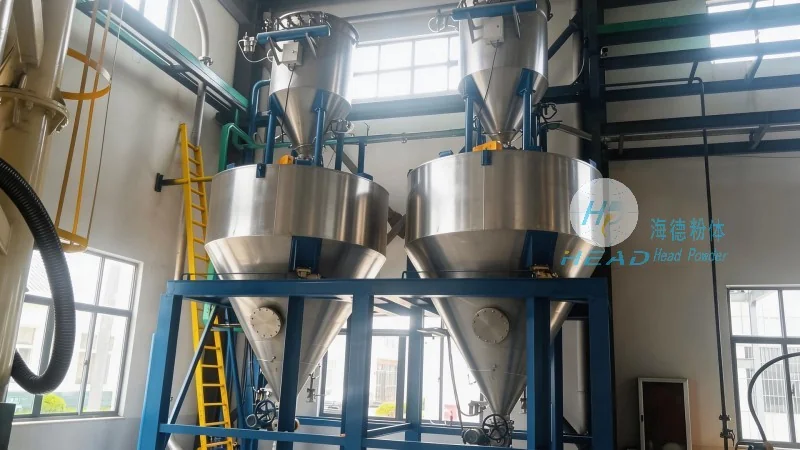
Applications and Industries
The bean cake powder pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is widely used in various industries that require the handling of fine powders. These include the food processing industry, where bean cake powder is used as a raw material for animal feed or human consumption; the agricultural industry, where it is used as a fertilizer or soil conditioner; and the chemical industry, where it is used as a raw material for the production of other products. The equipment is also suitable for use in pharmaceutical and cosmetic industries, where the powder needs to be handled in a clean and hygienic environment.
Maintenance and Safety Considerations
To ensure the long-term performance and safety of the bean cake powder pneumatic conveying system, regular maintenance and proper safety measures are essential. Regular inspections should be conducted to check for any leaks in the pipeline or components, and the rotary valve and compressor should be lubricated as per the manufacturer's recommendations. The system should also be equipped with safety features, such as pressure relief valves and emergency shut-off switches, to prevent accidents and ensure the safety of the operators. Additionally, the powder should be stored in a dry and clean environment to prevent caking and blockages in the system.
Conclusion
In conclusion, the bean cake powder pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is an efficient and reliable solution for handling fine powders in various industrial applications. The system's operation process and working principle are based on proven technology, ensuring smooth and controlled material transfer. With proper maintenance and safety measures, the equipment can provide long-term performance and contribute to the overall productivity of the production line. HeadPowder continues to innovate and provide advanced powder handling solutions to meet the evolving needs of the industry.




