HeadPowder, a leading provider in the field of industrial dust collection and material handling, specializes in advanced pneumatic conveying systems designed for efficient and reliable powder transport. The pulse dust collector powder pneumatic conveying system is a sophisticated solution that integrates dust filtration with material transport, offering a compact and effective approach to handling powders in various industrial applications. This system is engineered to meet the demands of modern manufacturing processes, ensuring high efficiency, low maintenance, and optimal performance.
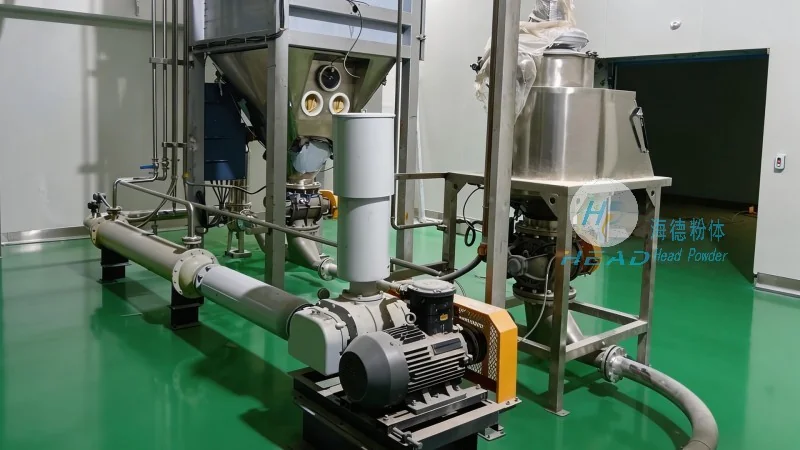
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder is a professional enterprise based in Shandong, China, dedicated to the research, development, and manufacturing of industrial dust collection and material conveying equipment. With years of experience in the industry, the company has established itself as a trusted partner for businesses seeking reliable solutions for dust management and powder handling. The company's commitment to quality, innovation, and customer satisfaction has enabled it to serve a wide range of industries, including chemical, pharmaceutical, food processing, and more. HeadPowder's products are designed to enhance operational efficiency, reduce downtime, and improve overall productivity for its clients.
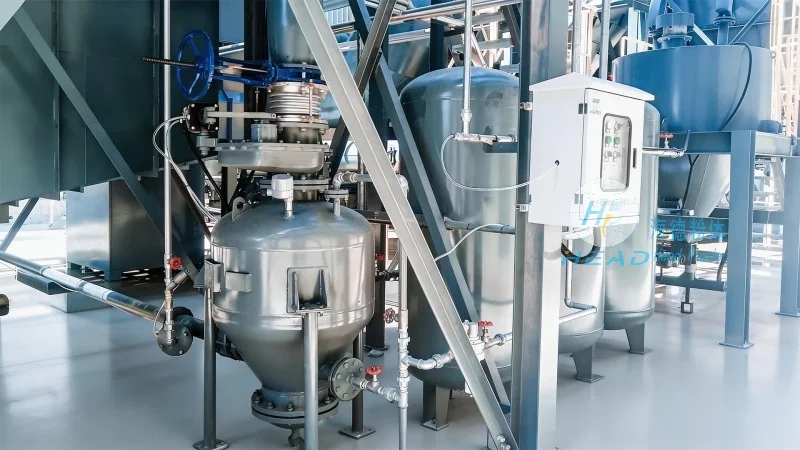
Working Principle of the Pulse Dust Collector
The pulse dust collector is a critical component of the pneumatic conveying system, responsible for capturing and filtering airborne dust particles before they are released into the environment. It operates on the principle of reverse air cleaning, where compressed air is pulsed through the filter bags to dislodge accumulated dust. This process ensures that the filter media remains clean and effective, maintaining high filtration efficiency. The collector features a series of filter bags housed in a cylindrical housing, with an inlet for dusty air and an outlet for clean air. As contaminated air enters the collector, it passes through the filter bags, where dust particles are trapped. The clean air then exits the collector, while the collected dust is periodically discharged through a hopper at the bottom.
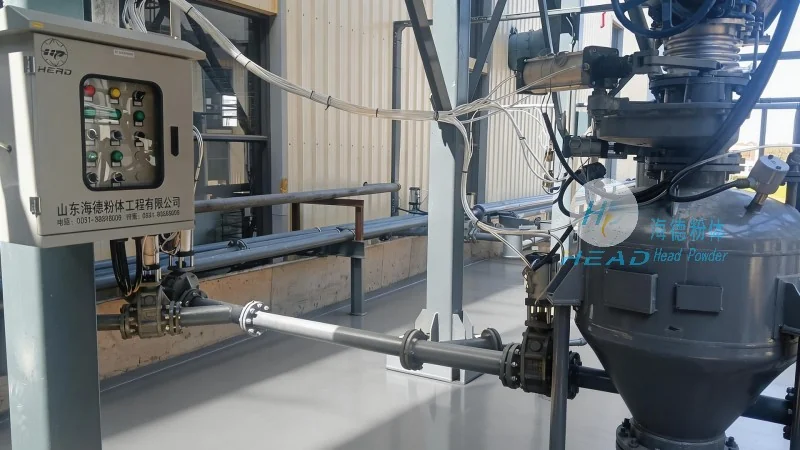
Operation Process of the Pneumatic Conveying System
The pneumatic conveying system utilizes a combination of positive and negative pressure to transport powders from a source to a destination. The process begins with the powder being fed into the system, either manually or through an automated feeder. The powder is then drawn into the conveying line by a vacuum or pressure source, depending on the system configuration. The pulse dust collector is integrated into the system to ensure that the transported powder remains clean and free from contaminants. The system operates by creating a pressure differential between the source and destination, allowing the powder to be moved through the pipeline. The conveying line is typically made of stainless steel or other corrosion-resistant materials to withstand the abrasive nature of the powder and the cleaning process. The system is equipped with sensors and controls to monitor pressure, flow rate, and other parameters, ensuring smooth and efficient operation.
Key Features and Benefits
The pulse dust collector powder pneumatic conveying system offers several key features that make it an ideal choice for industrial applications. These include high filtration efficiency, low maintenance requirements, and compact design. The system is designed to handle a wide range of powder types, from fine powders to bulk materials, with minimal loss or degradation. The pulse cleaning mechanism ensures that the filter bags are cleaned regularly, preventing clogging and maintaining consistent performance. The system also features automatic control systems that adjust the cleaning cycle based on the dust load, optimizing energy consumption and reducing operational costs. Additionally, the system is equipped with safety features such as pressure relief valves and overcurrent protection to ensure safe and reliable operation.
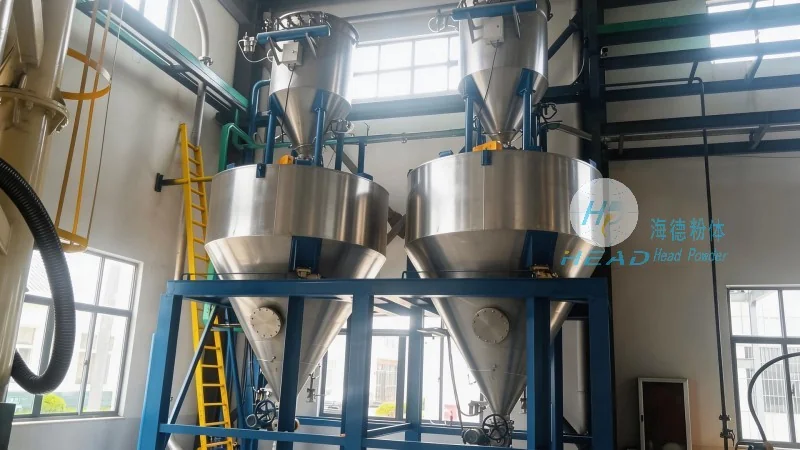
Applications and Industries
The pulse dust collector powder pneumatic conveying system is widely used in various industries, including chemical manufacturing, pharmaceutical production, food processing, and mining. In chemical plants, the system is used to transport powders such as pigments, catalysts, and raw materials, ensuring that the process remains clean and efficient. In pharmaceutical facilities, the system is used to handle powders like active pharmaceutical ingredients (APIs) and excipients, maintaining strict hygiene standards. In food processing industries, the system is used to transport powders such as flour, sugar, and spices, ensuring that the products remain free from contaminants. The system's ability to handle different powder types and its compact design make it suitable for a wide range of applications, from small-scale operations to large-scale industrial plants.




