High-calcium powder material handling systems are critical components in industrial operations, particularly in sectors that require the efficient and safe transport of calcium-rich powders. These systems are designed to manage the flow of high-calcium powders from storage to processing or packaging units, ensuring minimal loss, contamination, and operational downtime. The operation process and working principle of such systems involve several key stages and mechanisms that work in tandem to achieve optimal performance. Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-performance material handling systems tailored to the unique needs of high-calcium powder applications. Their systems are engineered with precision and durability to ensure reliable operation in demanding industrial environments.
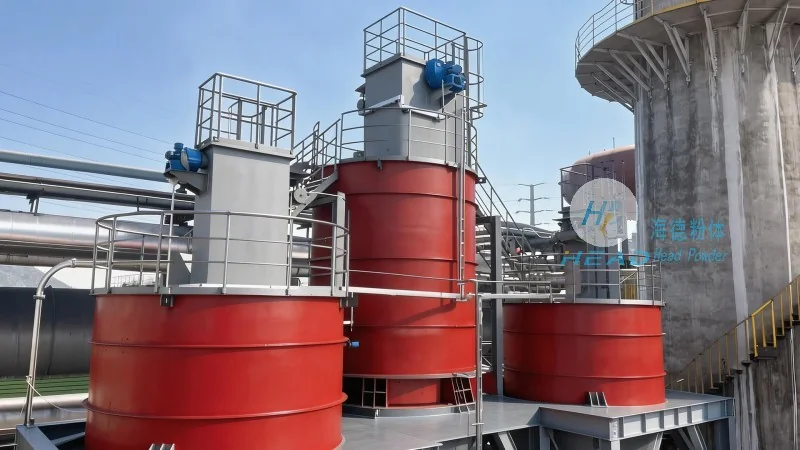
System Overview and Core Components
At the heart of a high-calcium powder handling system lies a combination of specialized equipment tailored to the unique properties of high-calcium powders. These materials often exhibit high moisture content, abrasive characteristics, or tendency to agglomerate, which necessitates the use of robust and efficient conveying technologies. The system typically includes components such as hoppers for material storage, feeders to control the flow rate, conveying mechanisms (like screw conveyors, pneumatic systems, or bucket elevators), and control panels for automated operation. Each component is selected based on the specific characteristics of the high-calcium powder, such as particle size, density, and flowability. The company’s engineering team at Shandong HeadPowder Engineering Co., Ltd. carefully evaluates these factors to design systems that maximize efficiency and minimize maintenance.
Working Principle: The Step-by-Step Operation Process
The operation of a high-calcium powder material handling system follows a systematic sequence that ensures consistent and reliable material transport. The process begins with the loading of high-calcium powder into the hopper, where the material is stored under controlled conditions to prevent caking or degradation. A feeder, often a rotary valve or a mass flow feeder, then regulates the flow of powder from the hopper into the conveying system. This controlled feeding is crucial to maintain a steady flow rate, which is essential for preventing blockages and ensuring the smooth operation of downstream equipment. The feeders are designed with adjustable speed controls, allowing operators to match the flow rate to the processing capacity of the system.
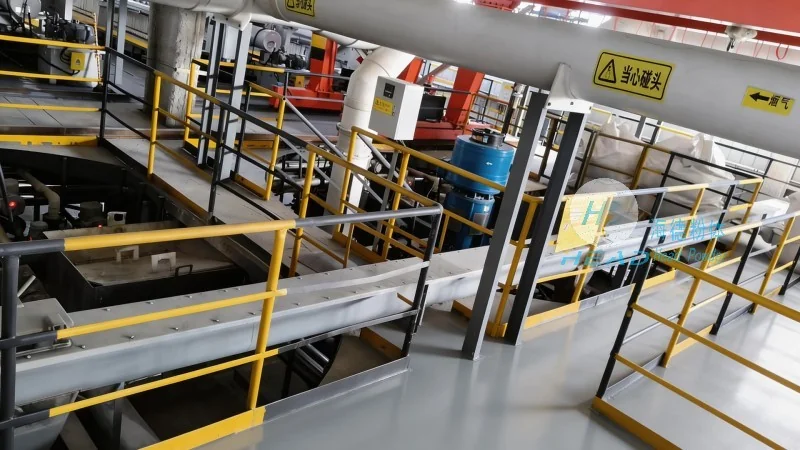
Once the powder is fed into the conveying mechanism, it is transported to the next stage of the process. For example, a screw conveyor uses rotating screws to push the powder forward, while a pneumatic system uses compressed air to create a flow of powder through a pipeline. The choice of conveying method depends on factors like the distance to be covered, the required flow rate, and the need for dust control. The conveying system is equipped with features such as airtight seals and dust collection systems to minimize environmental impact and maintain product quality. The company’s systems incorporate advanced filtration and collection technology to ensure compliance with environmental regulations and to protect the working environment from dust exposure.
Key Features and Advantages of High-Calcium Powder Handling Systems
High-calcium powder handling systems are engineered with several features that enhance their performance and reliability. One of the primary advantages is the ability to handle abrasive and high-density materials without significant wear on the equipment. The use of high-quality materials for the hopper and conveyor components, such as stainless steel or wear-resistant alloys, ensures long service life and minimal maintenance. Additionally, the systems are designed for easy cleaning and maintenance, which is critical for maintaining product purity and compliance with industry standards. The company’s systems include quick-release mechanisms and easy-to-access components, simplifying the cleaning process and reducing downtime.
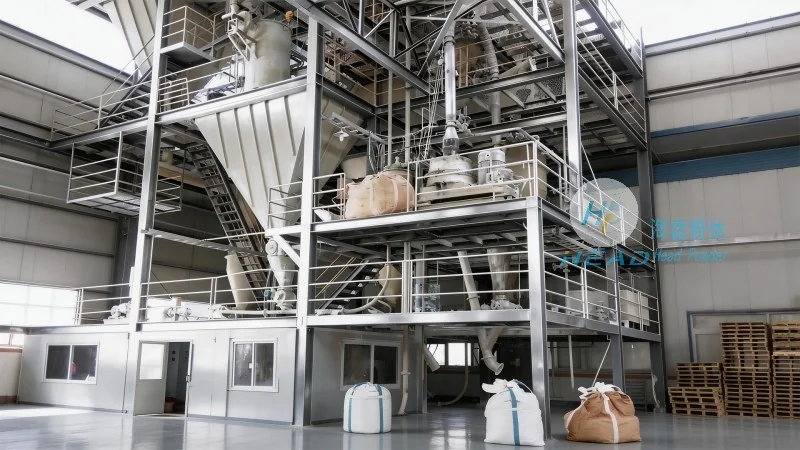
Another key feature is the integration of advanced control systems that allow for real-time monitoring and adjustment of the operation. These systems can include sensors to detect material levels, flow rates, and pressure, providing operators with immediate feedback to address any issues. The automation capabilities of modern high-calcium powder handling systems reduce the need for manual intervention, leading to increased efficiency and reduced labor costs. Furthermore, the systems are designed to comply with safety regulations, including explosion-proof features for handling potentially flammable powders or dust, ensuring a safe working environment. The company prioritizes safety in their design, incorporating features like emergency stop buttons and interlocks to prevent accidents.
Application and Industry Relevance
High-calcium powder handling systems are widely used in various industries, including food processing, pharmaceuticals, and chemical manufacturing. In the food industry, high-calcium powders are often used as nutritional supplements or fortifiers in products like dairy, beverages, and baked goods. The efficient handling of these powders is essential to maintain product quality and consistency. In the pharmaceutical sector, high-calcium powders are used in the formulation of supplements and medications, where precision and purity are paramount. The systems ensure that the powders are transported without contamination, preserving their efficacy and safety.
In the chemical industry, high-calcium powders are used in the production of cement, concrete, and other construction materials. The handling systems in this sector must be capable of handling large volumes of material and operating under high pressure and temperature conditions. The robust design of these systems ensures that they can withstand the demanding conditions of chemical processing while maintaining the quality of the high-calcium powder. The company’s systems are customized to meet the specific requirements of each industry, providing tailored solutions that enhance operational efficiency.
Maintenance and Operational Considerations
Proper maintenance is crucial to ensure the long-term performance and reliability of high-calcium powder handling systems. Regular inspections of the hopper, conveyor, and control systems are necessary to identify and address any issues before they lead to system failure. The use of high-quality spare parts and adherence to manufacturer guidelines for maintenance schedules are essential for minimizing downtime and extending the service life of the equipment. Additionally, operators should be trained to recognize signs of wear or malfunction, such as increased noise or reduced flow rate, and take appropriate action to resolve the issue. The company provides comprehensive maintenance services and training programs to support their clients in maintaining optimal system performance.
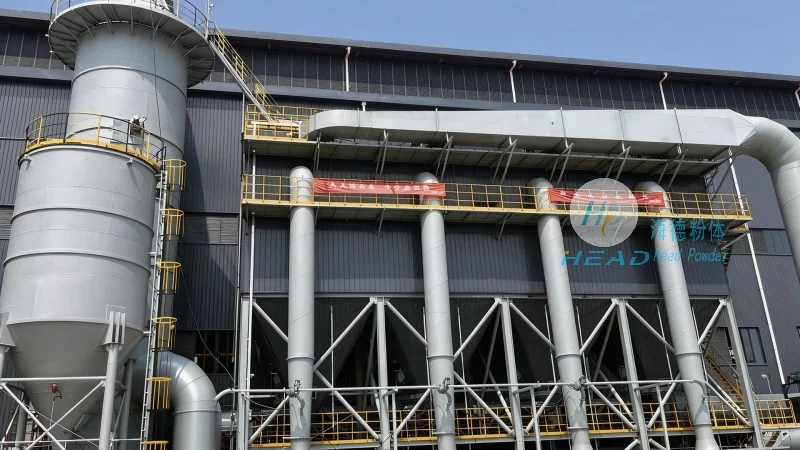
Environmental considerations also play a significant role in the operation of high-calcium powder handling systems. The systems are equipped with dust collection and filtration systems to minimize the release of powders into the environment, ensuring compliance with environmental regulations. Proper ventilation and cleaning procedures are also important to maintain a safe and healthy working environment for personnel. By addressing these operational and environmental factors, high-calcium powder handling systems can operate efficiently and sustainably over their service life. The company emphasizes sustainability in their product design, incorporating energy-efficient components and recyclable materials to reduce the environmental impact of their systems.




