Biocatalyst material handling systems represent a sophisticated approach to transporting and managing materials in industrial processes, particularly those involving enzymatic reactions. These systems are designed to enhance efficiency, precision, and safety in the handling of biocatalysts, which are enzymes or other biological catalysts used to accelerate chemical reactions in various applications such as pharmaceuticals, food processing, and biofuels. The integration of advanced engineering principles with biological catalysts has led to the development of specialized systems that optimize material flow while maintaining the integrity and activity of the biocatalysts.
Working Principle of Biocatalyst Material Handling Systems
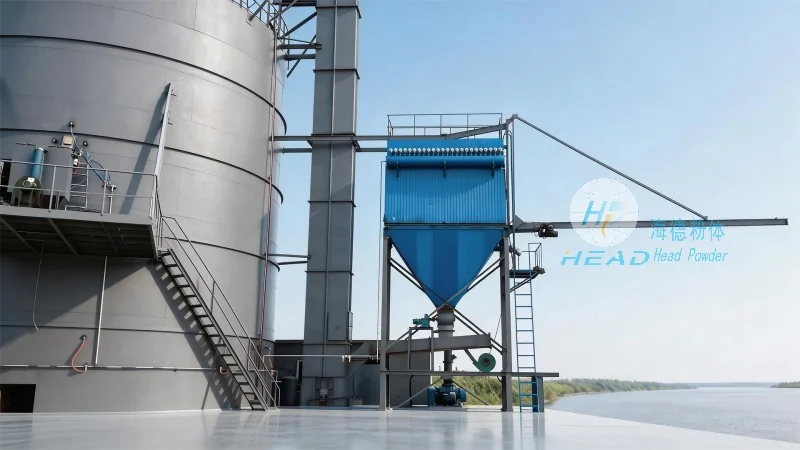
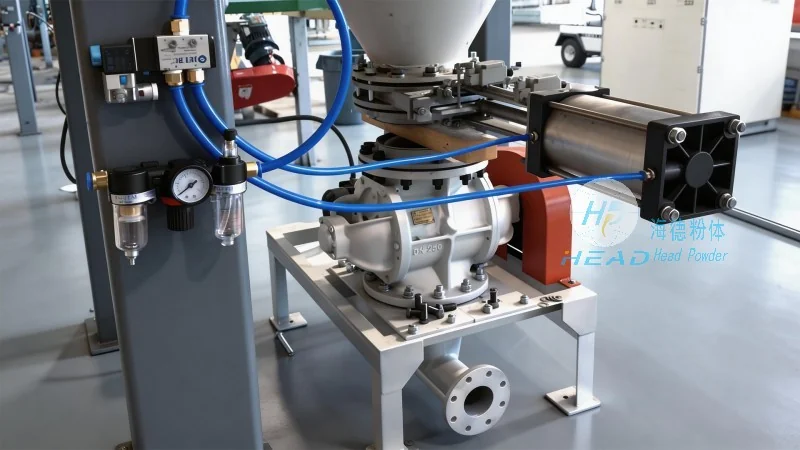
The core working principle of biocatalyst material handling systems revolves around the seamless integration of mechanical components with biocatalyst compatibility features. These systems typically consist of a series of components, including pumps, conveyors, and storage tanks, all engineered to minimize exposure to conditions that could denature or deactivate the biocatalysts. For instance, many systems employ gentle handling mechanisms, such as peristaltic pumps or low-shear conveyors, to prevent shear stress that could damage enzyme structures. Additionally, temperature and pH control systems are integrated to maintain optimal conditions for the biocatalysts during transport. The system operates by receiving biocatalyst materials from a source, processing them through the handling components, and delivering them to the next stage of the production process. This process ensures that the biocatalysts remain active and effective throughout the material handling phase, which is critical for maintaining the efficiency of downstream reactions.
Key Features of Biocatalyst Material Handling Systems
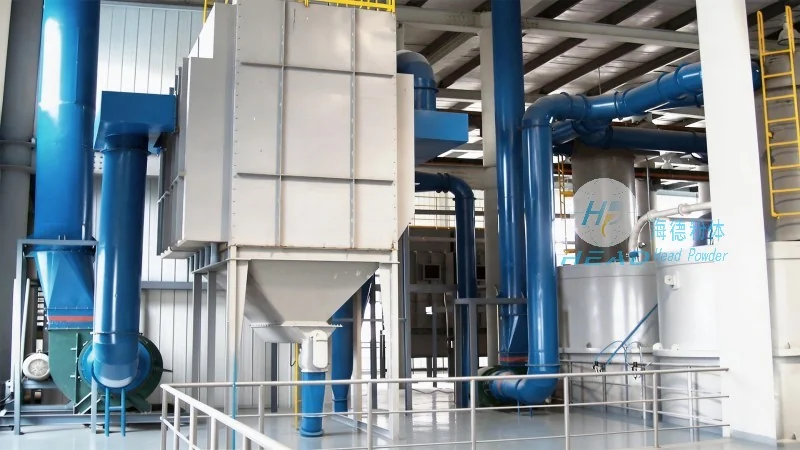
Biocatalyst material handling systems are characterized by several key features that distinguish them from conventional material handling equipment. Firstly, they prioritize biocompatibility, ensuring that all materials in contact with the biocatalysts are non-toxic and do not interfere with the enzymatic activity. This includes the use of food-grade or biocompatible materials for components like pipes, valves, and containers. Secondly, these systems are designed for gentle handling, minimizing mechanical stress and shear forces that could degrade the biocatalysts. Features such as low-speed rotation in conveyors and soft-seal pumps help preserve the structural integrity of enzymes. Thirdly, advanced monitoring and control systems are incorporated to maintain consistent conditions. Sensors for temperature, pH, and flow rate allow real-time adjustments to keep the biocatalysts within their optimal operational range. This proactive control helps prevent degradation and ensures consistent performance. Fourthly, the systems often include modular designs, allowing for easy customization and scalability to accommodate different production volumes and biocatalyst types. This flexibility makes them suitable for a wide range of industrial applications, from small-scale laboratory processes to large-scale manufacturing.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading provider of specialized engineering solutions for the biocatalyst industry. With a focus on innovation and precision, the company has developed advanced biocatalyst material handling systems that meet the stringent requirements of modern industrial applications. HeadPowder's expertise lies in the integration of mechanical engineering with biological science, ensuring that their systems not only handle materials efficiently but also preserve the activity and stability of biocatalysts. The company's facilities are located in Shandong, China, where they leverage local resources and expertise to deliver high-quality products and services. By adhering to rigorous quality standards and continuous research, headpowder has established itself as a trusted partner in the biocatalyst processing sector, helping clients optimize their production processes and enhance overall efficiency.




