HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced material handling systems tailored for industrial applications. This article provides an in-depth exploration of the working principle and key features of a desulfurization sodium bicarbonate material handling system, highlighting how such systems enhance operational efficiency and reliability in chemical processing environments.
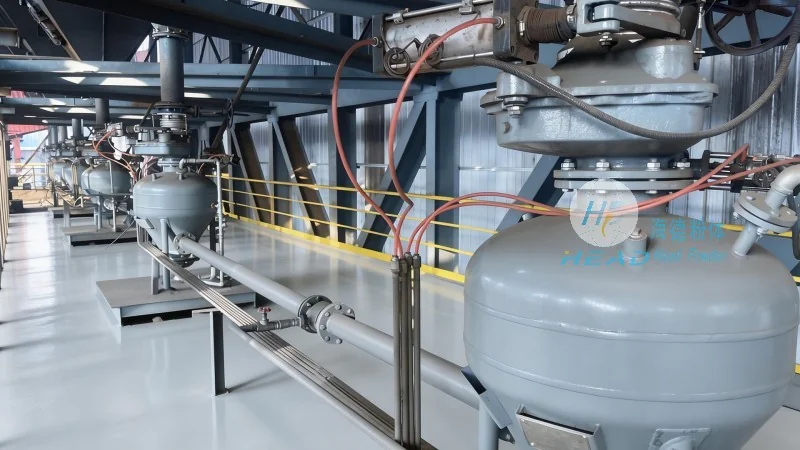
Working Principle of the Desulfurization Sodium Bicarbonate Material Handling System
The desulfurization sodium bicarbonate material handling system is engineered to efficiently transport sodium bicarbonate, a critical reagent in flue gas desulfurization processes, from storage to processing units. The system typically operates through a combination of mechanical components and control mechanisms that ensure precise material flow and minimal loss. At its core, the system involves several key stages: material storage, feeding, conveying, and distribution. The storage silo or hopper holds the sodium bicarbonate, which is then fed into a conveyor system—often a screw conveyor or pneumatic conveyor—based on the specific requirements of the plant. The conveyor transports the material to the processing equipment, such as desulfurization reactors or scrubbers, where it is introduced into the flue gas stream to neutralize sulfur compounds. The control system monitors the flow rate, pressure, and level of the material, ensuring consistent performance and preventing overfilling or underflow. This integrated approach minimizes downtime and maximizes the system's effectiveness in maintaining the desired desulfurization efficiency.
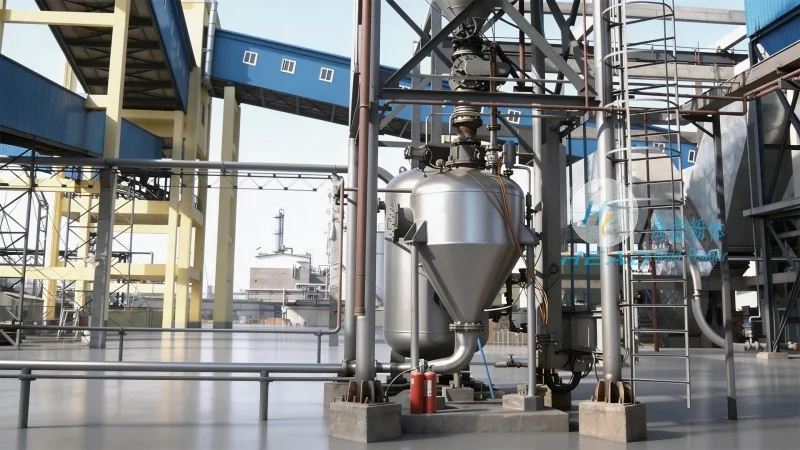
Key Features of the Desulfurization Sodium Bicarbonate Material Handling System
HeadPowder's desulfurization sodium bicarbonate material handling system is designed with several distinct features that set it apart in the industry. Firstly, the system incorporates advanced material handling technology, including high-capacity conveyors and precise feeding mechanisms, which ensure reliable and continuous operation. The use of durable materials, such as stainless steel, in the construction of the system components enhances longevity and resistance to corrosion, a critical factor in chemical processing environments. Secondly, the system features an intelligent control system that allows for real-time monitoring and adjustment of the material flow. This control system integrates sensors and automation technology to optimize performance, reduce energy consumption, and minimize maintenance requirements. Thirdly, the system is modular and scalable, enabling it to be customized to fit the specific needs of different industrial plants. Whether for small-scale or large-scale desulfurization operations, the system can be adjusted to handle varying material volumes and processing speeds. Additionally, the system is equipped with safety features, such as overload protection and emergency stop mechanisms, to ensure the safety of operators and equipment. These features collectively contribute to the system's high efficiency, low maintenance, and long service life, making it a preferred choice for industrial applications.
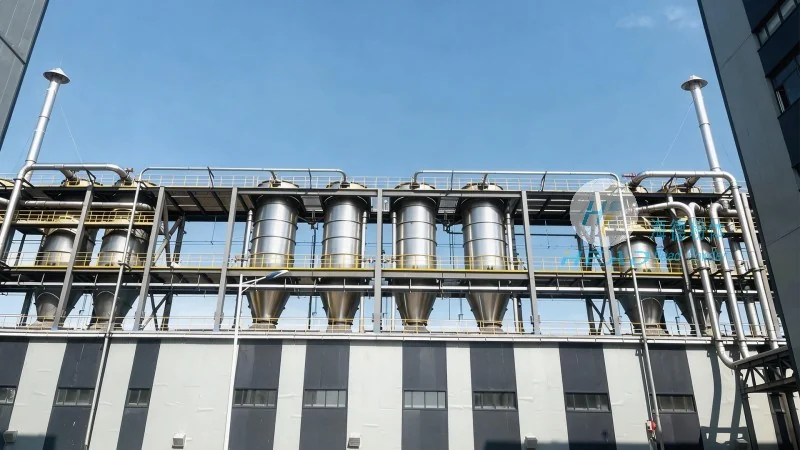
Conclusion and Application Benefits
HeadPowder's desulfurization sodium bicarbonate material handling system exemplifies the company's commitment to providing innovative and reliable solutions for industrial material handling challenges. By combining advanced technology with robust engineering, the system ensures efficient transportation of sodium bicarbonate, a vital component in flue gas desulfurization processes. The system's features, including its intelligent control, durability, and scalability, make it suitable for a wide range of industrial applications. As a result, the system not only improves operational efficiency but also contributes to the overall sustainability and environmental compliance of the plants it serves. HeadPowder's expertise in engineering and material handling ensures that clients receive a system that meets their specific needs while adhering to industry standards and safety regulations.




