Foam pneumatic conveying has emerged as a highly effective method for transporting bulk materials over significant distances. This technology leverages a mixture of air and foam to create a stable, low-pressure conveying system that can handle a wide range of materials, from fine powders to granules. The core principle involves generating a foam medium by injecting air into a liquid carrier, which then carries the material through pipelines. This approach offers several advantages over traditional pneumatic conveying systems, including reduced material degradation, lower energy consumption, and enhanced safety. As a result, foam pneumatic conveying is increasingly being adopted in industries such as pharmaceuticals, food processing, and chemical manufacturing, where material integrity and process efficiency are critical.
How Foam Pneumatic Conveying Works
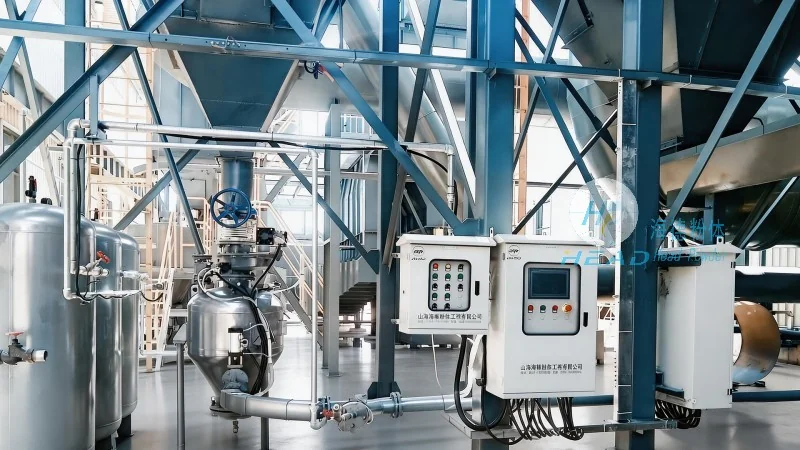
The process begins with the preparation of the foam solution. A liquid carrier, typically water, is mixed with a small amount of surfactant to create a stable foam. This foam is then introduced into the conveying line along with the material to be transported. The foam acts as a carrier, entraining the particles and moving them through the pipeline. The system operates at low pressures, typically ranging from 0.5 to 2 bar, which minimizes the risk of material degradation and equipment wear. The foam also helps to lubricate the pipeline, reducing friction and energy requirements. The material is discharged at the receiving end by allowing the foam to collapse, releasing the material into a collection hopper or silo. This gentle discharge process ensures that the material remains intact, preserving its quality and properties.
Key Advantages of Foam Pneumatic Conveying
One of the primary benefits of foam pneumatic conveying is its ability to handle materials that are difficult to transport using conventional methods. For example, fine powders and cohesive materials often experience issues such as blockages and material degradation in traditional systems. Foam pneumatic conveying mitigates these problems by providing a stable, low-energy environment. The low pressure and gentle flow of the foam prevent particle agglomeration and reduce the risk of dust generation. Additionally, the system is highly flexible, allowing for changes in material type or flow rate without significant modifications to the equipment. This adaptability makes it suitable for a variety of applications, from short-distance transfers to long-distance transportation over several hundred meters. Another advantage is the reduced energy consumption compared to high-pressure pneumatic systems. The low-pressure operation of foam conveying systems results in lower operational costs and less wear on components, leading to longer equipment life and lower maintenance requirements.
Applications in Various Industries
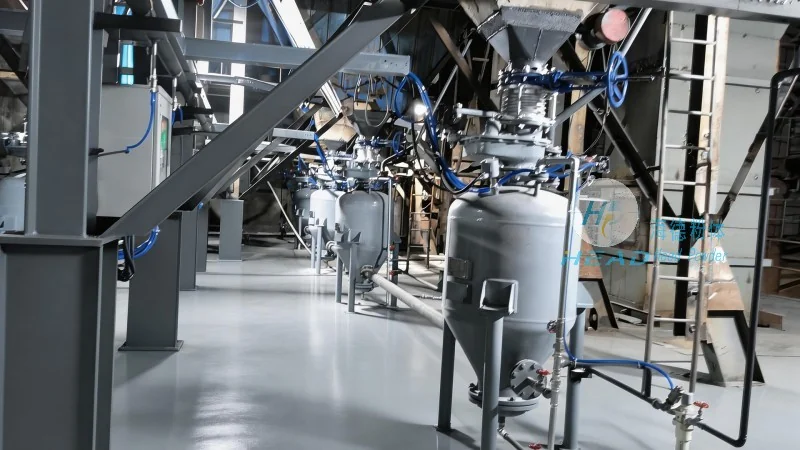
Foam pneumatic conveying is widely used across multiple industries due to its versatility and effectiveness. In the pharmaceutical industry, it is employed to transport active pharmaceutical ingredients (APIs) and other sensitive materials, ensuring that the product remains free from contamination and maintains its potency. The gentle handling of the foam system prevents the degradation of heat-sensitive or moisture-sensitive compounds, which is crucial for maintaining product quality. In the food processing sector, foam conveying is used to handle powders such as flour, sugar, and spices. The system's ability to handle fine powders without generating dust makes it ideal for food-grade applications, where hygiene and product integrity are paramount. The chemical industry also benefits from foam pneumatic conveying, particularly when transporting chemicals that are corrosive or reactive. The system's low pressure and controlled environment minimize the risk of chemical reactions and equipment damage, ensuring safe and efficient material handling. Furthermore, the technology is suitable for handling materials that are prone to caking or agglomeration, such as certain types of minerals and fertilizers. By maintaining a consistent flow and preventing material buildup, foam conveying helps to ensure smooth operations and reduce downtime in processing plants.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
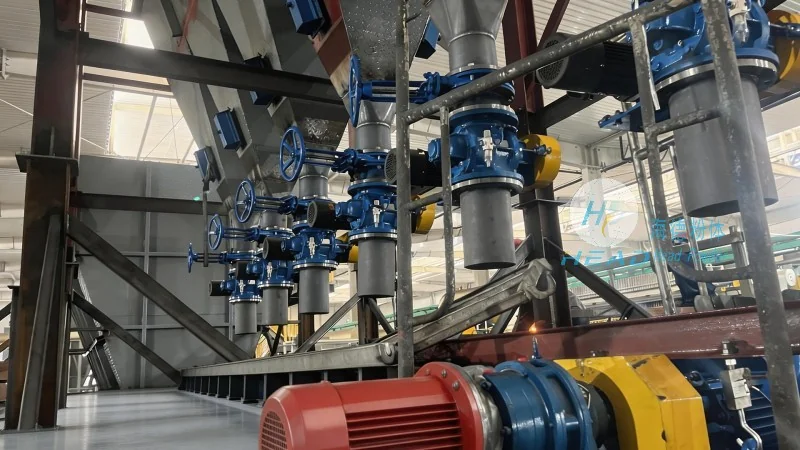
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of foam pneumatic conveying solutions. The company specializes in designing, manufacturing, and installing customized conveying systems tailored to the specific needs of its clients. With a strong focus on innovation and quality, HeadPowder has developed advanced technologies that enhance the efficiency and reliability of foam conveying systems. The company's team of engineers and technicians brings extensive experience in material handling and process optimization, ensuring that each project is executed with precision and care. HeadPowder's commitment to customer satisfaction is reflected in its comprehensive after-sales support, including maintenance services, technical assistance, and system upgrades. The company operates from its headquarters in Shandong, China, where it has established a robust manufacturing and research facility. This location allows HeadPowder to leverage local resources and expertise while serving clients globally. The company's products are designed to meet international standards and are suitable for a wide range of industrial applications, from small-scale operations to large-scale manufacturing facilities.
Conclusion: The Future of Material Handling with Foam Pneumatic Conveying
As industries continue to demand more efficient and sustainable material handling solutions, foam pneumatic conveying is poised to play an increasingly important role. The technology's ability to overcome distance limitations while maintaining material integrity makes it an attractive option for many applications. With ongoing advancements in foam generation and pipeline design, the efficiency and effectiveness of foam conveying systems are expected to improve further. Companies like Shandong HeadPowder Engineering Co., Ltd. are at the forefront of this technological evolution, developing innovative solutions that address the evolving needs of the market. By leveraging the benefits of foam pneumatic conveying, industries can enhance their operational efficiency, reduce costs, and improve product quality. As the technology continues to mature, it is likely to become a standard solution for long-distance material transport, particularly for sensitive and difficult-to-handle materials. The future of material handling looks promising with the continued development and adoption of foam pneumatic conveying systems.




