Phenolic powder, also known as Bakelite powder, is a critical material in various industrial applications, including electronics, automotive, and manufacturing sectors. The efficient and reliable transportation of this powder is essential for maintaining production efficiency and product quality. This article introduces the pneumatic conveying solutions tailored for phenolic powder, highlighting the technical aspects, benefits, and implementation strategies provided by Shandong HeadPowder Engineering Co., Ltd.
Understanding Phenolic Powder Properties and Challenges in Conveying
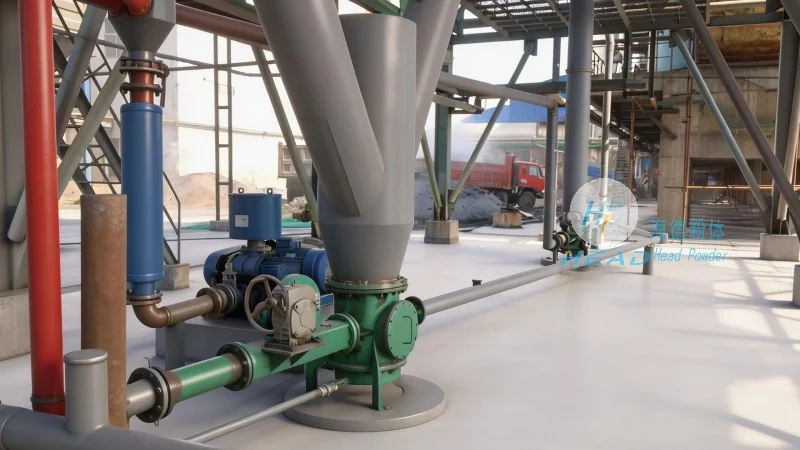
Phenolic powder is characterized by its fine particle size, high density, and potential for static charge accumulation. These properties pose unique challenges during material handling. Traditional methods like bucket elevators or belt conveyors may not be suitable due to the risk of dust explosion, material degradation, or inefficient transfer. Pneumatic conveying offers a solution by utilizing air to transport the powder in a sealed system, minimizing exposure to the environment and reducing the risk of contamination. The headpowder team at Shandong HeadPowder Engineering Co., Ltd. specializes in designing systems that address these challenges effectively.
Key Components of a Phenolic Powder Pneumatic Conveying System
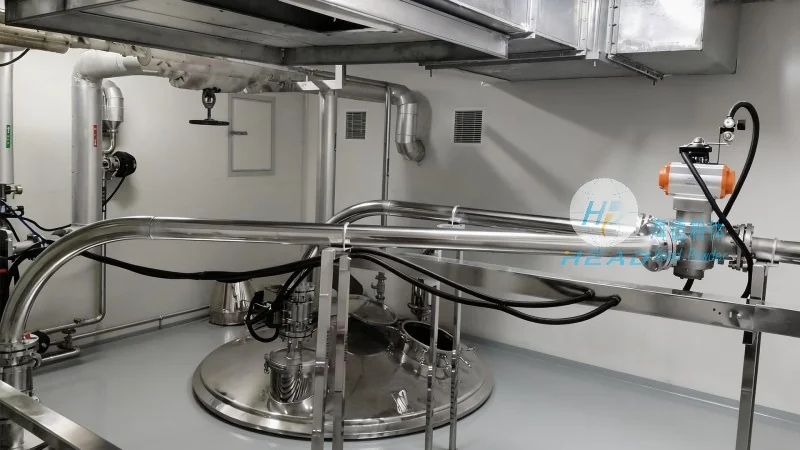
A pneumatic conveying system for phenolic powder typically consists of several key components. These include a material feeder to control the flow rate, a conveying line (either positive or negative pressure depending on the application), a filter system to capture fine particles and prevent dust emissions, and a receiver or discharge unit for the final material storage. The system may also incorporate equipment such as rotary valves, airlocks, and pressure vessels to ensure smooth operation and safety. Shandong HeadPowder Engineering Co., Ltd. designs customized solutions that integrate these components based on the specific requirements of the client, including the volume of material, distance to be conveyed, and environmental regulations.
Benefits of Using Pneumatic Conveying for Phenolic Powder
Implementing a pneumatic conveying system for phenolic powder offers numerous advantages. Firstly, it provides a dust-free and clean transfer process, which is crucial for maintaining product purity and compliance with environmental standards. Secondly, the sealed system reduces the risk of static discharge and dust explosions, enhancing workplace safety. Thirdly, pneumatic conveying can handle high volumes of material with minimal maintenance compared to other bulk material handling methods. Additionally, the system allows for precise control over the flow rate, ensuring consistent product quality and reducing waste. For businesses in the phenolic powder industry, these benefits translate into improved operational efficiency, lower costs, and enhanced product reliability.
Customization and Integration Services by HeadPowder
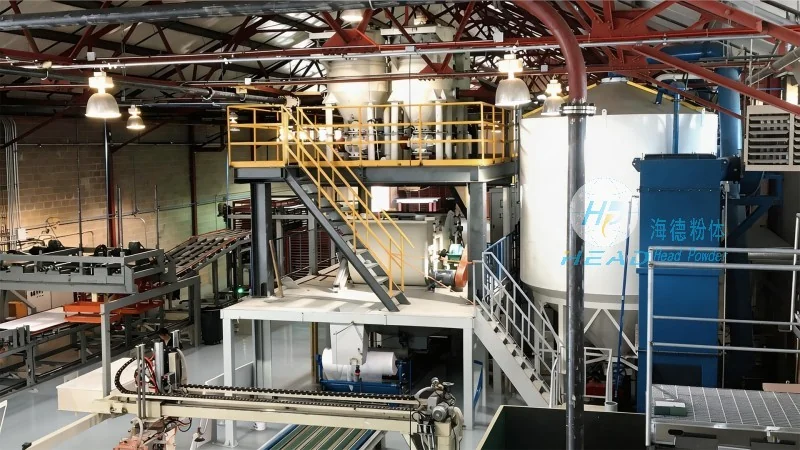
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, offers comprehensive customization and integration services for phenolic powder pneumatic conveying systems. The company works closely with clients to understand their specific operational needs, process parameters, and production goals. Through detailed site surveys and technical consultations, headpowder engineers design systems that are tailored to the unique characteristics of each application. This includes selecting the appropriate conveying method (e.g., dilute phase or dense phase), determining the optimal air pressure and flow rates, and specifying the necessary equipment for filtration and material handling. The company also provides installation, commissioning, and after-sales support to ensure the system operates at peak efficiency throughout its lifecycle. By leveraging their expertise and experience, headpowder helps clients achieve seamless material transfer, minimize downtime, and maximize productivity.
Case Studies and Real-World Applications
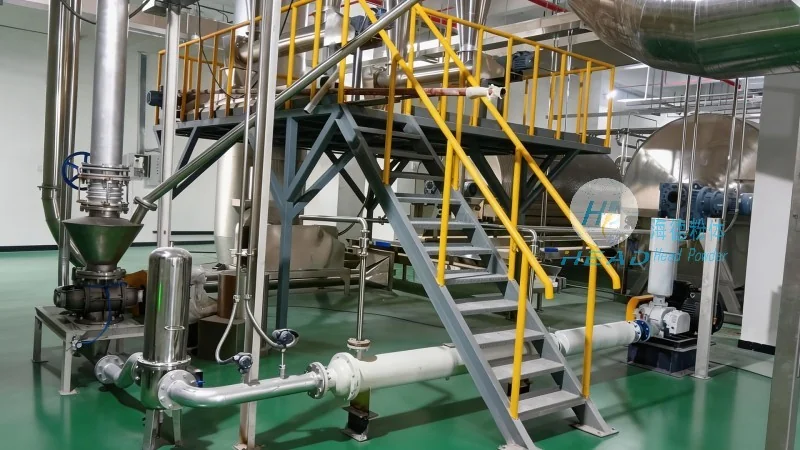
HeadPowder has successfully implemented phenolic powder pneumatic conveying solutions for a wide range of clients across different industries. For example, in an electronics manufacturing facility, the company designed a positive pressure system to transport fine phenolic powder from a storage silo to a mixing unit, ensuring minimal dust generation and precise control over the material flow. In another case, a automotive parts manufacturer benefited from a dense phase conveying system that efficiently moved bulk phenolic powder from a production line to a finishing station, reducing material loss and improving production throughput. These case studies demonstrate the effectiveness of headpowder's solutions in addressing the specific challenges of phenolic powder handling and enhancing overall operational performance.
Conclusion and Contact Information
Phenolic powder pneumatic conveying solutions are a vital component for industries relying on this material. By leveraging the expertise of Shandong HeadPowder Engineering Co., Ltd. (headpowder), businesses can achieve efficient, safe, and reliable material handling. The company's customized approach, combined with its commitment to quality and customer satisfaction, makes it a trusted partner for phenolic powder pneumatic conveying systems. For more information or to discuss your specific needs, please contact Shandong HeadPowder Engineering Co., Ltd., located in Shandong, China.




