Calcium hydroxide, commonly known as slaked lime, is a widely used industrial chemical with applications in construction, water treatment, and chemical manufacturing. The efficient handling and transportation of this material are crucial for industrial operations, and pneumatic conveying systems have emerged as a reliable solution. This article explores the principles and operational characteristics of calcium hydroxide pneumatic conveying equipment, highlighting its applications and benefits in various industrial settings.
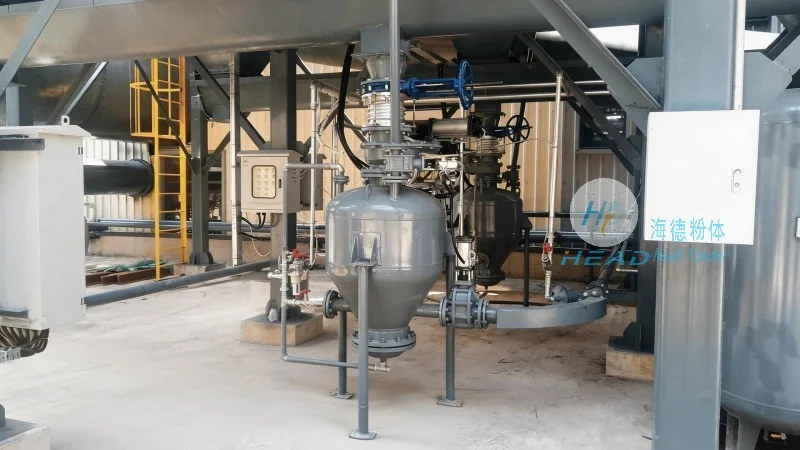
Understanding Pneumatic Conveying Technology
Pneumatic conveying is a method of transporting bulk materials through a pipeline using a gas stream, typically air. In the case of calcium hydroxide, the system involves a series of components that work together to move the material from the source to the destination. The core components include a material feeder, a conveying line, a separator, and a dust collector. The process begins with the material being fed into the system, where it is mixed with air under controlled pressure. The air stream then propels the material through the pipeline, ensuring a smooth and continuous flow. The separator and dust collector are essential for maintaining air quality and preventing material buildup in the system.
Key Principles of Calcium Hydroxide Pneumatic Conveying
The effectiveness of a calcium hydroxide pneumatic conveying system depends on several key principles. First, the material's properties, such as its density, particle size, and moisture content, must be considered. Calcium hydroxide is a fine powder, which can affect the system's efficiency and require adjustments to the air flow rate and pressure. Second, the system's design must account for the material's reactivity and potential for caking or agglomeration. Proper moisture control and temperature management are critical to prevent these issues and ensure consistent performance. Third, the system's capacity and scalability are important factors, as industrial operations often require high-volume material transport. The design must accommodate varying flow rates and material loads to meet production demands.
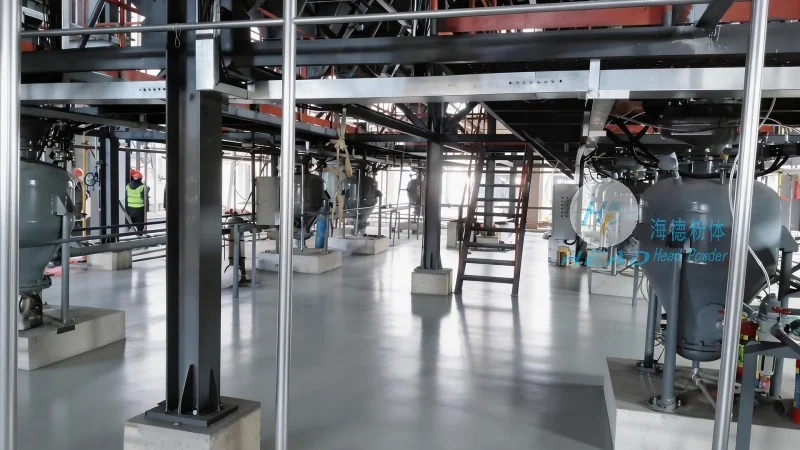
Working Scene Characteristics and Applications
The working scene characteristics of calcium hydroxide pneumatic conveying equipment vary based on the specific industrial application. In construction, for example, the system is used to transport lime for mortar and plaster production. The equipment must be capable of handling large volumes of material and operating in a dusty environment. In water treatment facilities, the system is used to convey lime for pH adjustment and coagulation processes. The equipment must be designed to meet stringent environmental and safety standards, as water treatment operations require high levels of air quality and material purity. In chemical manufacturing, the system is used to transport lime for the production of other chemicals, such as calcium chloride and calcium carbonate. The equipment must be compatible with the chemical environment and resistant to corrosion and wear.
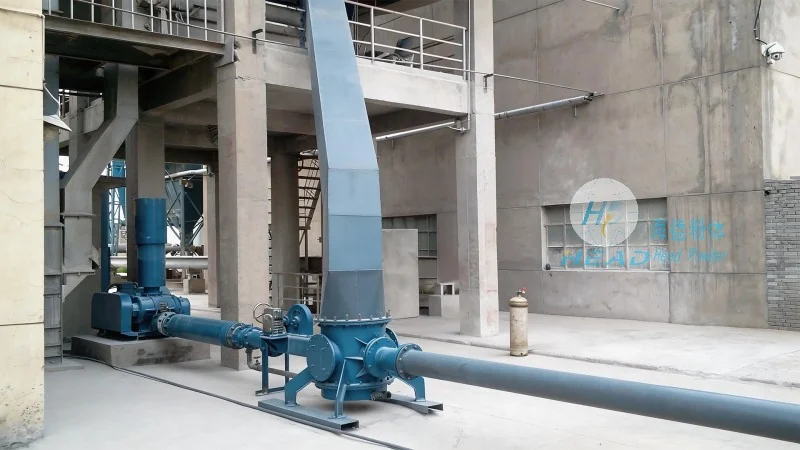
Benefits and Advantages of Pneumatic Conveying for Calcium Hydroxide
There are several benefits and advantages of using pneumatic conveying systems for calcium hydroxide transportation. First, the system is a closed-loop operation, which minimizes dust emissions and improves workplace safety. This is particularly important for calcium hydroxide, which can cause respiratory issues if inhaled. Second, the system is flexible and can be easily integrated into existing industrial processes. It can be adapted to handle varying material loads and flow rates, making it suitable for both small-scale and large-scale operations. Third, the system is energy-efficient compared to other material transport methods, such as truck or rail transport. The use of compressed air as the conveying medium reduces the need for additional equipment and maintenance costs. Fourth, the system is hygienic and can be designed to meet food-grade or pharmaceutical standards, making it suitable for applications where material purity is critical.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, the brand name of Shandong HeadPowder Engineering Co., Ltd., is a prominent manufacturer of pneumatic conveying systems for industrial bulk materials. HeadPowder operates from Shandong, China, and has established itself as a leader in the field with its expertise in designing and producing high-quality equipment. The company focuses on providing customized solutions tailored to the specific needs of each client, ensuring optimal performance and efficiency in material handling operations. With a strong commitment to quality and innovation, HeadPowder's products are widely used in industries such as construction, water treatment, and chemical manufacturing, where reliable and efficient material transport is essential. The company's team of experienced engineers and technicians work closely with clients to develop solutions that meet stringent operational requirements and safety standards. HeadPowder's facilities are equipped with advanced technology and testing capabilities, enabling the production of durable and reliable equipment that withstands the demands of industrial environments. The company's customer service and support are also a key differentiator, with a dedicated team available to assist with installation, maintenance, and troubleshooting. HeadPowder's reputation for excellence and customer satisfaction has made it a trusted partner for businesses seeking efficient and effective pneumatic conveying solutions for calcium hydroxide and other bulk materials.




