Slurry and powder conveying equipment is a critical component in modern industrial operations, enabling the efficient transport of bulk materials across various sectors. These systems are essential for optimizing production workflows, reducing labor costs, and enhancing overall operational efficiency. The design and functionality of slurry and powder conveyors are tailored to handle diverse material properties, ensuring reliable and consistent material movement from source to destination. Whether in mining, chemical processing, or construction, these equipment play a pivotal role in streamlining material handling processes.
Core Principles of Slurry and Powder Conveying Technology
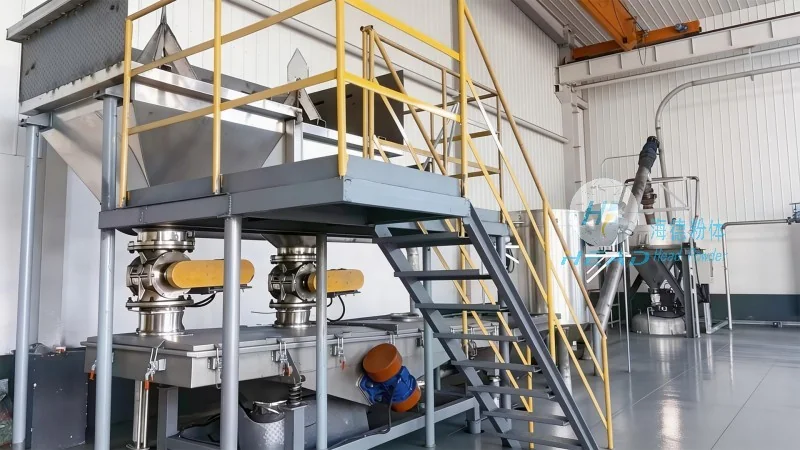
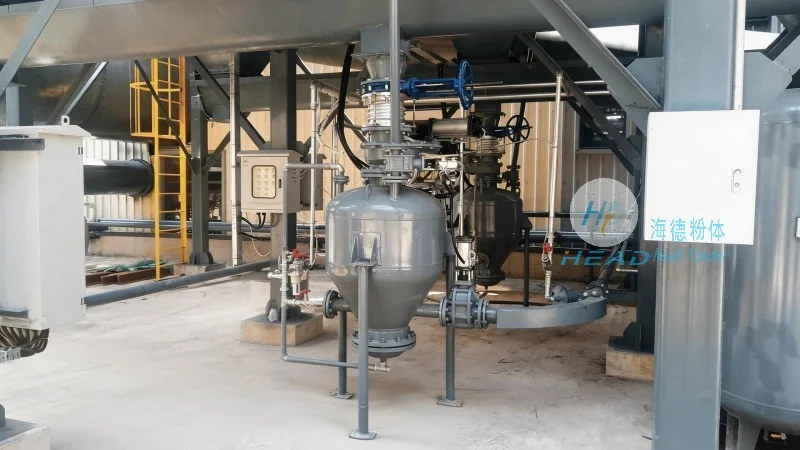
The fundamental principles governing slurry and powder conveying systems revolve around the mechanics of material transport. These systems typically operate based on either gravity or pressure-driven mechanisms, adapting to the specific characteristics of the conveyed materials. For slurry conveyors, pressure is often utilized to move mixtures of solids and liquids through pipelines, while powder conveyors may rely on vacuum or pressure to handle dry, fine materials. The selection of the appropriate conveying method depends on factors such as material density, particle size distribution, moisture content, and the required transport distance. Advanced engineering considerations, including the design of pipelines, pumps, and control systems, are critical to ensuring optimal performance and minimizing operational disruptions. Additionally, the use of specialized materials for components like pipelines and valves is essential to withstand the corrosive or abrasive nature of the materials being conveyed.
Working Scene Characteristics and Application Scenarios
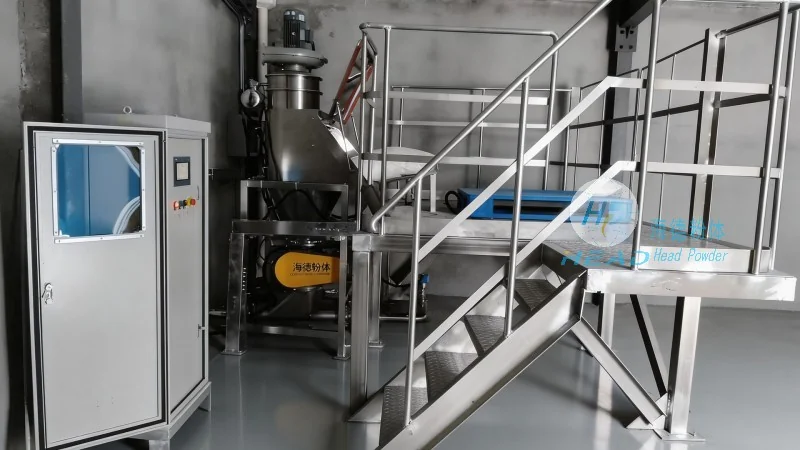
Slurry and powder conveyors are employed in a wide array of industrial applications, each presenting unique operational challenges and requirements. In the mining industry, these systems are vital for transporting ore and tailings, facilitating efficient extraction and processing of mineral resources. The chemical industry utilizes slurry conveyors for handling slurries of chemicals and byproducts, while the construction sector relies on them for transporting cement, sand, and other building materials. Additionally, in the food and pharmaceutical industries, specialized slurry and powder conveyors are used to transport raw materials and finished products, ensuring compliance with hygiene and safety standards. The working scene characteristics, such as the need for high capacity, low maintenance, and resistance to corrosion, vary significantly across these applications, necessitating customized solutions that address specific operational demands. For instance, in mining operations, conveyors must handle large volumes of ore with high abrasiveness, while in pharmaceutical applications, systems must maintain strict cleanliness and prevent contamination.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
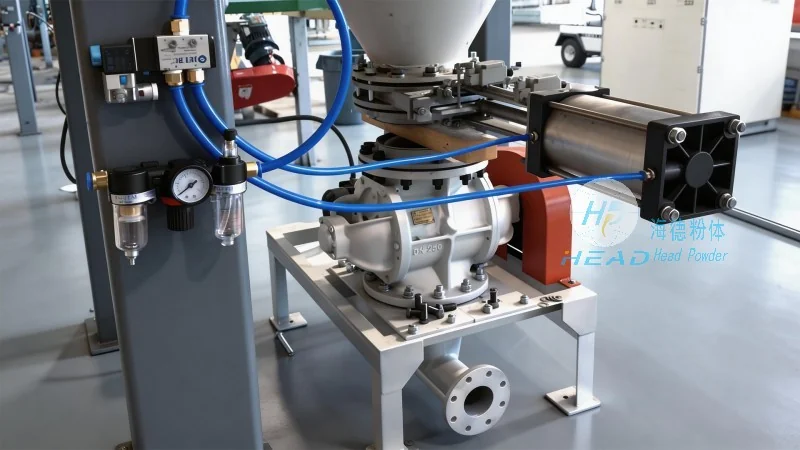
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of slurry and powder conveying equipment. HeadPowder is headquartered in Shandong, China, and specializes in the design, development, and production of advanced conveying systems tailored to meet the diverse needs of industrial clients. The company's commitment to innovation and quality has established it as a trusted partner in the industry, providing reliable solutions for material handling challenges. With a focus on customer satisfaction and technological advancement, HeadPowder continues to deliver high-performance slurry and powder conveyors that enhance operational efficiency and reduce costs for its clients. The company's engineering team leverages cutting-edge technology and extensive industry experience to develop customized solutions that address the unique requirements of each project, ensuring optimal performance and longevity of the equipment.




