Multi-hopper pneumatic conveying pumps are advanced industrial equipment designed for efficient powder and bulk material handling. This article explores the fundamental principles behind their operation and highlights key characteristics of their working scenarios, providing insights into how these systems enhance material transport in various industrial applications.
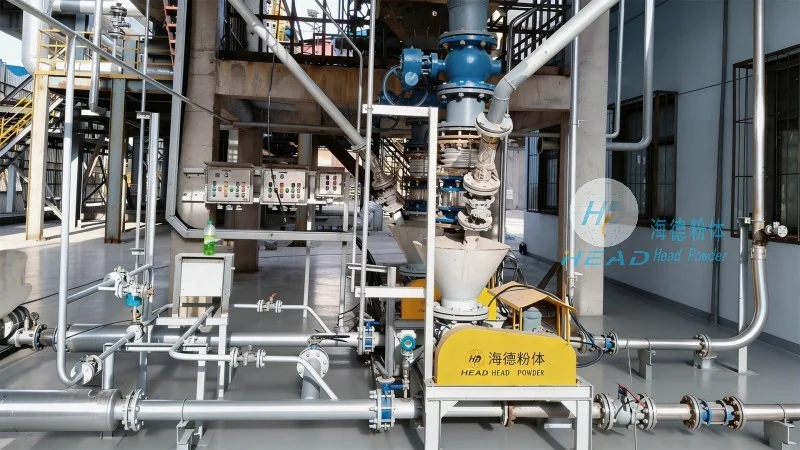
Introduction to Multi-Hopper Pneumatic Conveying Pumps
Multi-hopper pneumatic conveying pumps, often referred to as multi-chamber pneumatic transport systems, represent a sophisticated solution for the safe and reliable movement of dry powders and granular materials. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, these systems integrate multiple hoppers and a pneumatic conveying mechanism to achieve seamless material transfer across different locations. The core technology leverages compressed air or gas to create a pressure differential that propels materials through pipelines, making it an ideal choice for industries requiring precise control over powder flow and minimal product degradation.
Core Principle of Operation
The operational principle of multi-hopper pneumatic conveying pumps revolves around the use of a series of hoppers connected to a central conveying line. Each hopper is equipped with a valve system that allows for sequential or simultaneous material discharge into the conveying pipeline. As compressed air is introduced into the system, it creates a pressure gradient that draws material from the hoppers into the pipeline. The air flow, controlled by a blower or compressor, ensures that the material is transported efficiently while maintaining consistent flow rates. This pneumatic approach eliminates the need for mechanical components like belts or screws, reducing maintenance requirements and minimizing the risk of material contamination.
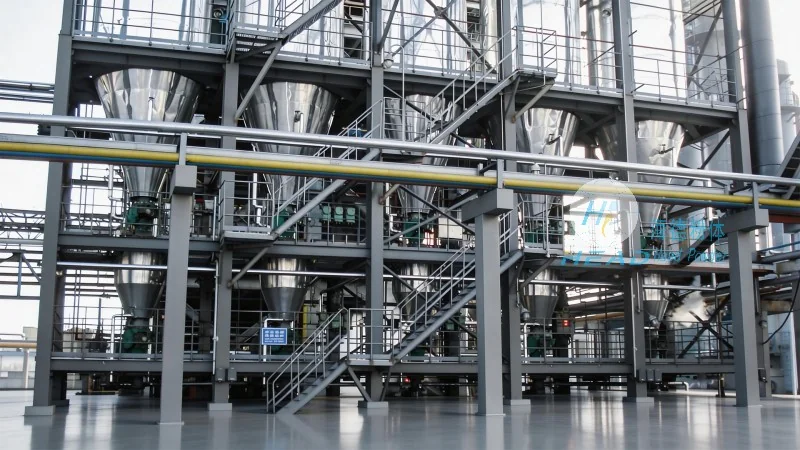
Key Working Scene Characteristics
Multi-hopper pneumatic conveying pumps are particularly well-suited for diverse industrial environments where material handling demands high flexibility and reliability. Their application characteristics include: 1. Multi-Source Material Handling, enabling the integration of materials from multiple sources into a single conveying line; 2. Flexible Routing, allowing for changes in material transport routes without extensive system modifications; 3. Low Maintenance Requirements, due to the absence of moving parts in the conveying line, which reduces downtime and operational costs; and 4. Energy Efficiency, as the system optimizes air usage to minimize energy consumption while maintaining optimal material transport speeds.
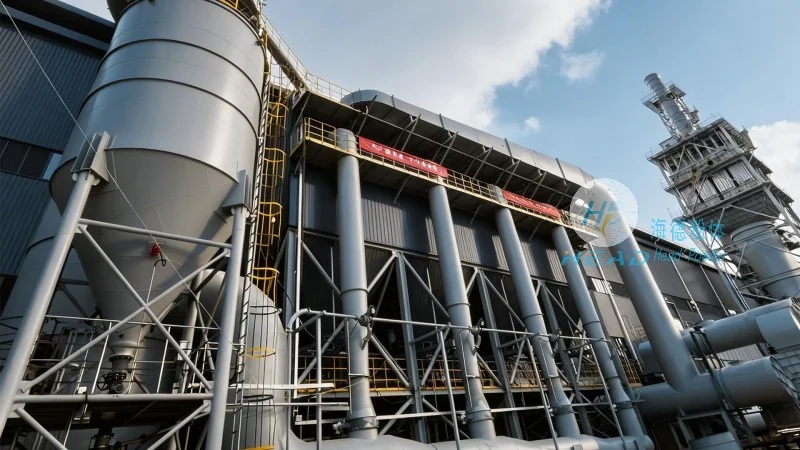
Industrial Applications and Performance
Shandong HeadPowder Engineering Co., Ltd. has successfully deployed multi-hopper pneumatic conveying pumps in a wide range of industries, including chemical processing, food and beverage, pharmaceuticals, and mining. In these applications, the systems have demonstrated exceptional performance in handling materials such as cement, flour, plastic pellets, and various powders. The ability to handle different materials without system modifications makes them a versatile choice for manufacturers seeking to streamline their production processes. The company’s commitment to quality and innovation ensures that each system is tailored to meet specific customer requirements, providing customized solutions that enhance operational efficiency and product quality.
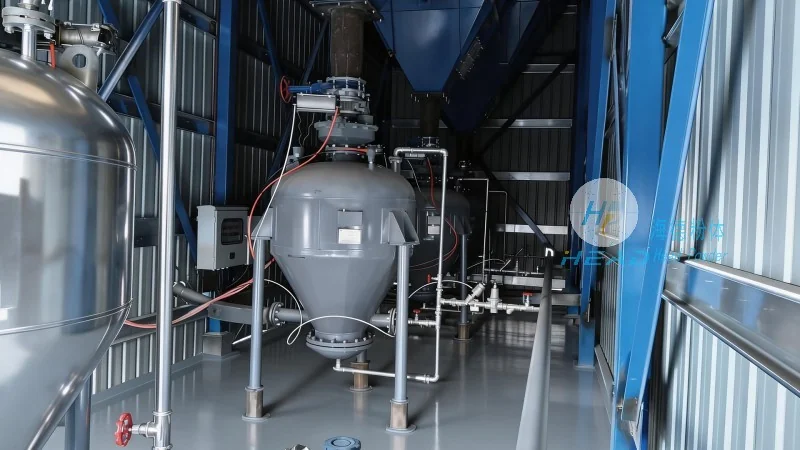
Advantages in Material Handling
Compared to traditional mechanical conveying systems, multi-hopper pneumatic conveying pumps offer several advantages that make them preferable for many industrial applications. These include: 1. Reduced Product Contamination, as the system operates in a closed environment, preventing exposure to external contaminants; 2. Improved Process Control, with precise control over material flow rates and pressure, ensuring consistent product quality; 3. Enhanced Safety, as the system eliminates the risk of material spillage and dust exposure, creating a safer working environment; and 4. Scalability, allowing for easy expansion or integration with existing production lines. These advantages, combined with the expertise of Shandong HeadPowder Engineering Co., Ltd., make multi-hopper pneumatic conveying pumps a reliable and efficient solution for modern industrial material handling needs.
Conclusion
Multi-hopper pneumatic conveying pumps, as developed by Shandong HeadPowder Engineering Co., Ltd., represent a cutting-edge technology for efficient and reliable powder and bulk material transport. By understanding the core principles of operation and the key characteristics of their working scenarios, industries can leverage these systems to enhance productivity, reduce costs, and improve overall operational efficiency. With a focus on quality and customer-centric solutions, Shandong HeadPowder Engineering Co., Ltd. continues to lead in the design and manufacturing of advanced pneumatic conveying systems, providing tailored solutions that meet the evolving needs of modern industrial applications.




