HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced fertilizer material conveying systems. These systems are engineered to efficiently transport bulk materials such as fertilizers, chemicals, and other granular or powdered substances across various industrial and agricultural settings. Understanding the principles and operational characteristics of these systems is crucial for optimizing material handling processes and ensuring operational efficiency.
Core Principles of Fertilizer Material Conveying Systems
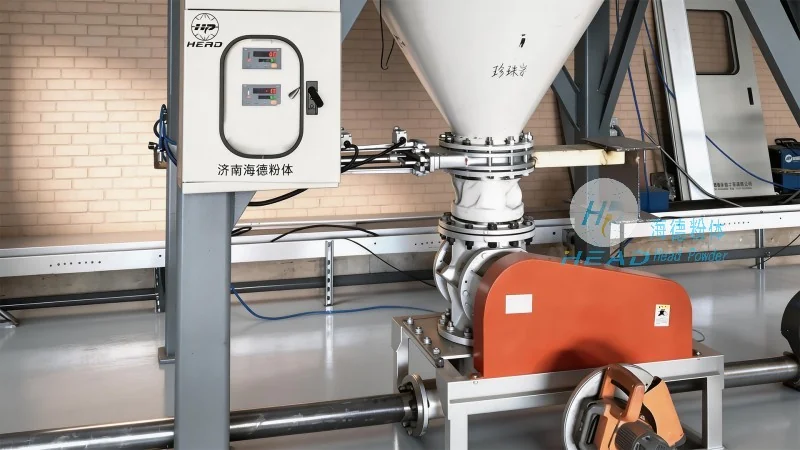
The fundamental principle behind fertilizer material conveying systems lies in the efficient transfer of bulk materials from one location to another with minimal loss, contamination, or degradation. These systems typically utilize mechanical components like conveyor belts, screw conveyors, or pneumatic transport mechanisms to move materials. The design of the system is tailored to the specific properties of the fertilizer, including its particle size, moisture content, and flow characteristics. For instance, systems designed for fine powders may incorporate special sealing and dust control features to prevent material spillage and environmental contamination. Additionally, the conveying equipment is engineered to handle varying loads and speeds, ensuring consistent performance under different operational conditions.
Working Scene Characteristics and Applications
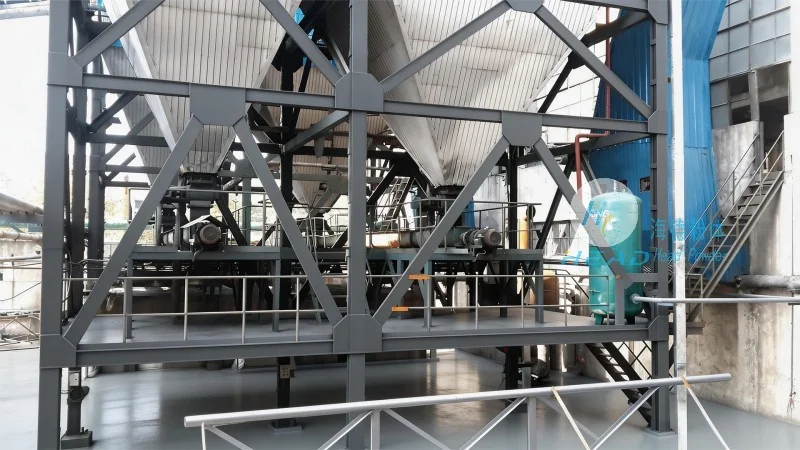
Fertilizer material conveying systems are widely used in diverse working environments, each presenting unique challenges and requirements. In agricultural settings, these systems are commonly employed in fertilizer production plants, storage facilities, and distribution centers to move raw materials and finished products. The systems must be capable of handling large volumes of material, often in high-volume production lines, while maintaining accuracy and minimizing downtime. Industrial applications include chemical processing plants, where the conveying of raw materials and intermediates is critical for continuous production. The working scene characteristics also encompass environmental factors, such as temperature variations and exposure to moisture, which can affect the material's properties and the system's performance. HeadPowder's conveying systems are designed to adapt to these conditions, ensuring reliable operation in both indoor and outdoor environments.
Key Features and Advantages in Different Operational Scenarios
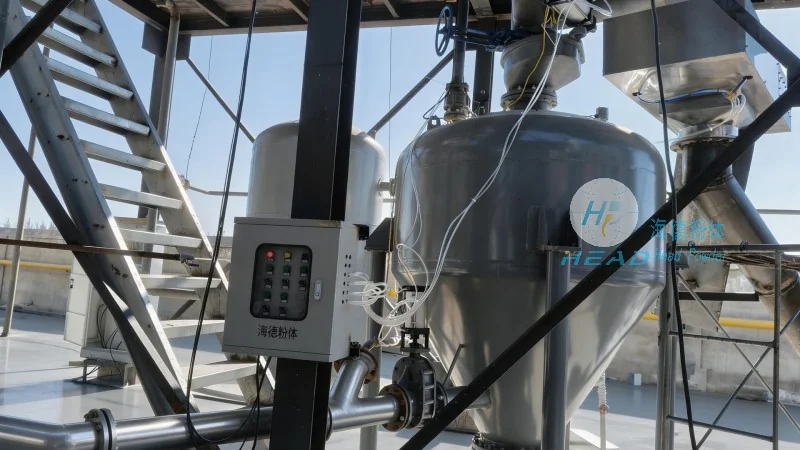
HeadPowder's fertilizer material conveying systems are equipped with several features that enhance their performance in various working scenarios. One notable feature is the use of durable materials for the conveyor components, such as food-grade stainless steel or high-strength polymers, which resist corrosion and wear from abrasive materials. This ensures long-term reliability and reduces maintenance costs. Another key advantage is the integration of advanced control systems, allowing for precise speed and load regulation. This capability is particularly important in scenarios where material flow needs to be synchronized with other production processes, such as packaging or blending. The systems also incorporate safety features, including emergency stop mechanisms and overload protection, to ensure operational safety in busy industrial environments. Furthermore, the modular design of the equipment enables easy customization and integration with existing infrastructure, making it suitable for both new installations and retrofits.
Conclusion and Company Overview
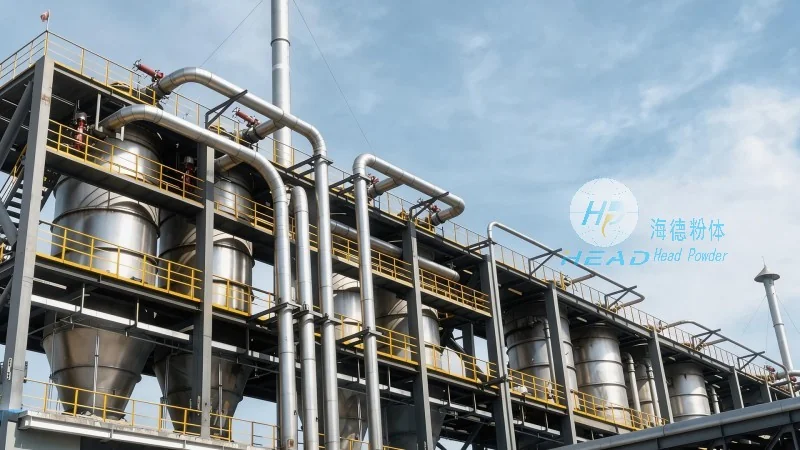
HeadPowder Engineering Co., Ltd., based in Shandong, China, continues to innovate in the field of fertilizer material conveying systems, providing solutions that meet the evolving needs of the agricultural and industrial sectors. By focusing on the core principles of efficient material transfer and adapting to diverse working scene characteristics, HeadPowder's systems deliver superior performance, reliability, and cost-effectiveness. The company's commitment to quality and customer satisfaction has established it as a trusted partner for businesses seeking to optimize their material handling operations. With a strong presence in the market and a dedication to technological advancement, HeadPowder remains at the forefront of delivering advanced conveying solutions for fertilizer and bulk material applications.




