For power plants and industrial facilities dealing with fly ash, the efficient and reliable transport of this material is crucial. The fly ash silo pneumatic conveying system, manufactured by Shandong HeadPowder Engineering Co., Ltd., offers a sophisticated solution that integrates advanced technology with practical application. This equipment is designed to handle the unique challenges associated with fly ash, ensuring safe, efficient, and environmentally compliant material transfer. The following sections will explore the fundamental principles behind this system and the specific working scene characteristics that make it an ideal choice for various industrial environments.
Basic Principle of Fly Ash Silo Pneumatic Conveying System
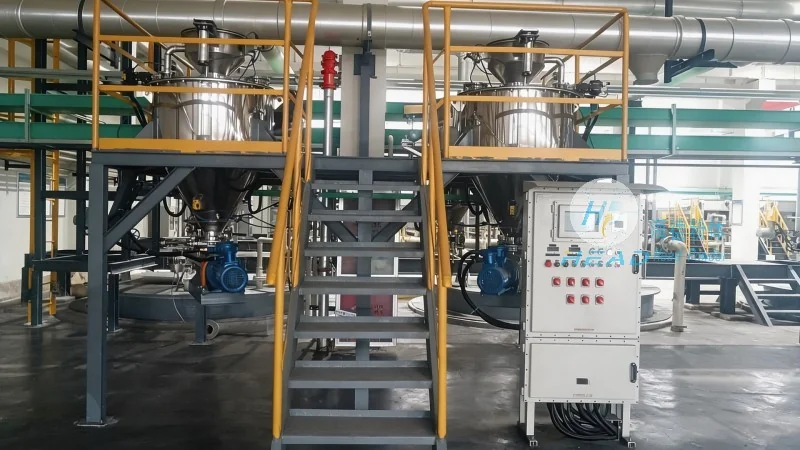
The core principle of the fly ash silo pneumatic conveying system is the use of compressed air or vacuum to transport fly ash from the storage silo to the designated discharge point. This process typically operates under positive pressure, where air is forced through the conveying line, creating a flow that carries the fly ash particles. The system consists of several key components, including the fly ash silo, air compressor, conveying pipeline, and control system. The air compressor generates the necessary pressure to move the material, while the pipeline network ensures the material is transported over long distances or through complex layouts. The control system monitors and regulates the pressure, flow rate, and other parameters to maintain optimal performance and prevent system failures. The material is introduced into the conveying line through a feed hopper or a rotary valve, which controls the flow rate and prevents blockages. The conveying process relies on the kinetic energy of the air to suspend and transport the fly ash particles, ensuring that the material moves smoothly and without clogging. This principle is particularly effective for handling fine powders like fly ash, as it minimizes the risk of material degradation and ensures consistent performance.
Working Scene Characteristics and Application Scenarios
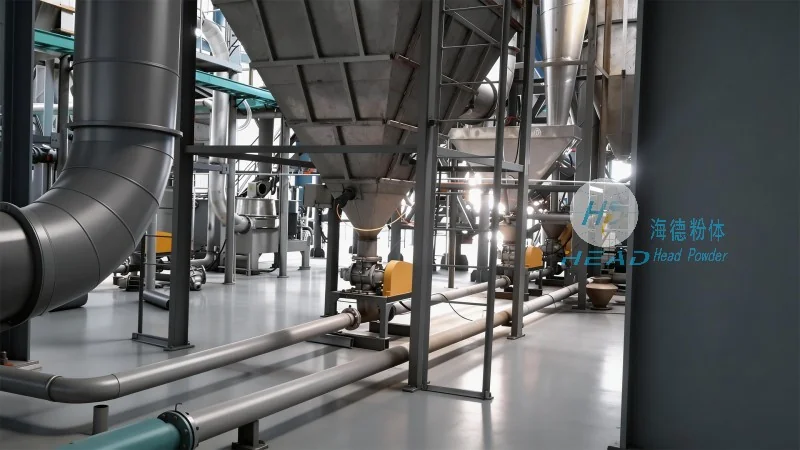
The fly ash silo pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. is designed to meet the diverse needs of industrial applications. Its working scene characteristics are tailored to the specific requirements of different industries, making it suitable for a wide range of environments. One of the primary working scene characteristics is its ability to handle large volumes of fly ash efficiently. The system can transport significant quantities of material over extended distances, which is essential for power plants with multiple storage silos or for facilities that need to distribute fly ash to different processing units. The equipment is also designed for high reliability and low maintenance, which is critical in industrial settings where downtime can result in significant operational costs. The working scene characteristics also include adaptability to different operating conditions, such as varying fly ash moisture content or particle size. The system can be adjusted to accommodate these variations, ensuring consistent performance regardless of the material's characteristics. Another key characteristic is the system's environmental friendliness. The pneumatic conveying process is enclosed, which prevents dust emissions and ensures compliance with environmental regulations. This is particularly important for facilities located in areas with strict air quality standards. The working scene characteristics also include safety features, such as pressure relief valves and emergency shut-off systems, which protect both the equipment and personnel from potential hazards. These features make the system suitable for use in hazardous environments, such as power plants where fly ash may contain trace amounts of hazardous substances. The equipment is also designed to be compatible with existing infrastructure, allowing for easy integration into existing plant layouts without major modifications. This adaptability reduces installation time and costs, making it a cost-effective solution for industrial facilities.
Company Information and Technical Support
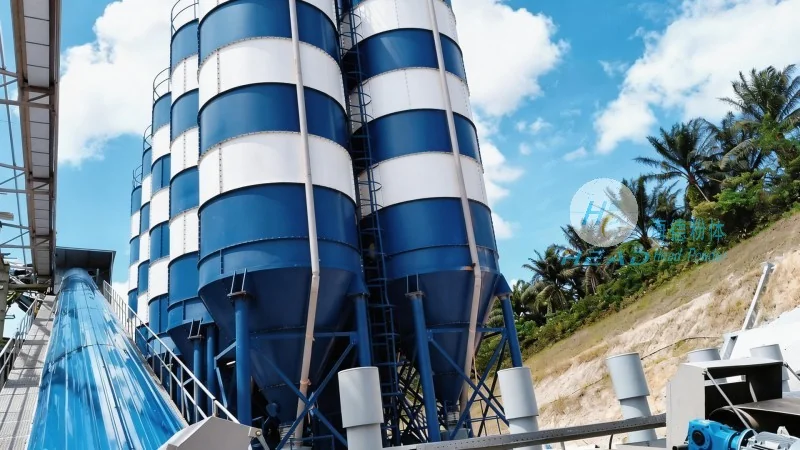
As a leading manufacturer of fly ash handling equipment, Shandong HeadPowder Engineering Co., Ltd. provides comprehensive technical support and after-sales service to ensure the long-term performance of its pneumatic conveying systems. The company is headquartered in Shandong, China, and has a team of experienced engineers and technicians who specialize in the design, manufacturing, and installation of fly ash handling systems. The company's commitment to quality and innovation has made it a trusted partner for power plants and industrial facilities worldwide. The technical support team offers on-site installation and commissioning services, ensuring that the system is properly installed and operational. They also provide regular maintenance and inspection services to prevent system failures and extend the equipment's lifespan. The company's R&D department continuously develops new technologies and improvements to its products, ensuring that they remain at the forefront of the industry. This commitment to innovation allows the company to offer cutting-edge solutions that meet the evolving needs of its customers. The company also provides training programs for customers' staff, ensuring that they are well-equipped to operate and maintain the equipment. This training helps to minimize downtime and maximize the system's efficiency. The company's customer-centric approach and comprehensive support services make it an ideal choice for industrial facilities seeking reliable and efficient fly ash handling solutions.




