HeadPowder, as a professional manufacturer based in Shandong, China, specializes in the design, development, and production of pneumatic conveying systems. The company's headquarters is located in Shandong, providing a solid foundation for its engineering expertise and product innovation in the field of material handling solutions.
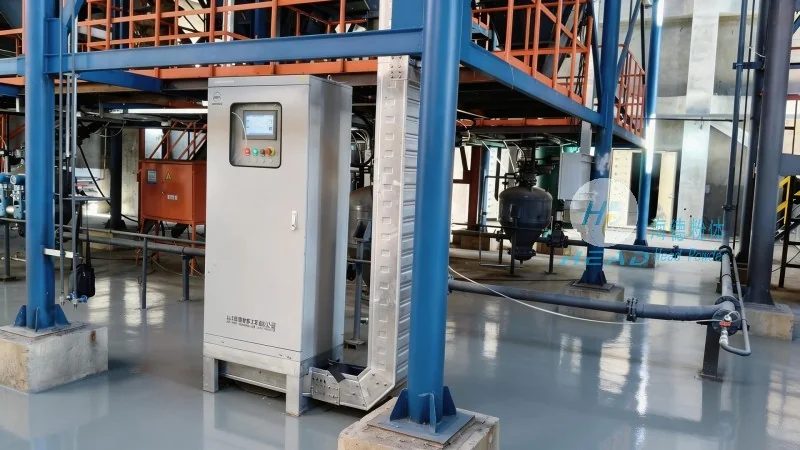
Overview of Pneumatic Conveying Systems
Pneumatic conveying systems are a critical component in modern industrial material handling, offering an efficient and flexible method for transporting bulk materials such as powders, granules, and fine particles. Unlike traditional mechanical conveyors, these systems utilize compressed air or other gases to move materials through a pipeline network. The fundamental principle involves creating a pressure differential that propels the material along the pipeline, ensuring a continuous and controlled flow. This technology is particularly advantageous for applications requiring dust-free, hygienic, or low-noise operation, making it suitable for industries like food processing, pharmaceuticals, and chemical manufacturing.
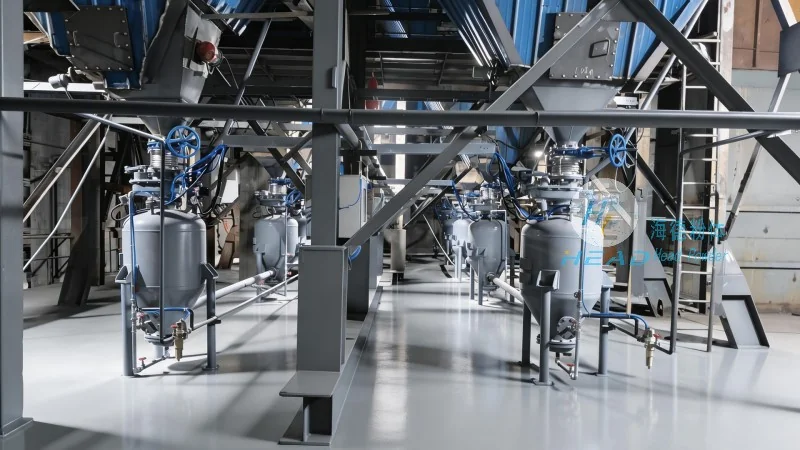
The Working Principle of HeadPowder Pneumatic Conveying Systems
At the core of HeadPowder's pneumatic conveying systems lies a sophisticated mechanism that combines air dynamics and material physics. The system typically consists of a blower, a hopper for material storage, a conveying line, and a receiver for the discharged material. The process begins when material is fed into the hopper, where it is then drawn into the conveying line by the high-velocity air generated by the blower. The air velocity is carefully controlled to ensure that the material is fully entrained and transported without segregation or degradation. The system may employ different modes of operation, including dilute-phase and dense-phase conveying, each tailored to specific material characteristics and application requirements.
Key Working Scene Characteristics
The working scene characteristics of HeadPowder's pneumatic conveying systems are tailored to meet diverse industrial needs, ensuring optimal performance in various environments. One of the primary advantages is the ability to handle a wide range of materials, from fine powders to larger granules, with minimal maintenance and low operational costs. The systems are designed for high efficiency, with minimal energy consumption and reduced material loss compared to traditional methods. Additionally, the enclosed pipeline design prevents dust contamination and maintains a clean working environment, which is crucial for industries that require strict hygiene standards. The flexibility of the system allows for easy integration into existing production lines, enabling seamless material transfer between different processing stages. In terms of scalability, HeadPowder's systems can be customized to accommodate varying production volumes, from small-scale laboratory applications to large-scale industrial operations. This adaptability makes them suitable for both new installations and retrofitting in existing facilities.
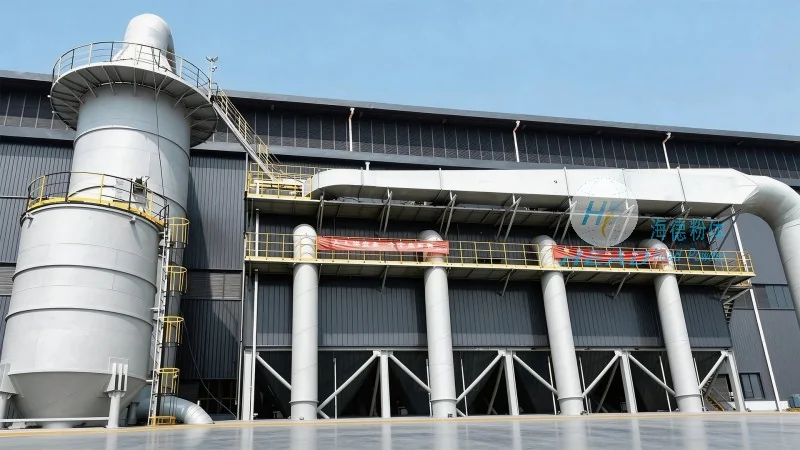
Application Examples and Performance Metrics
HeadPowder's pneumatic conveying systems have been successfully implemented in numerous working scenes across different industries. For instance, in the food processing industry, the systems are used to transport flour, sugar, and other dry ingredients with precision, ensuring product quality and safety. In the pharmaceutical sector, the hygienic design of the systems prevents cross-contamination, meeting stringent regulatory requirements. The performance metrics of these systems, such as conveying capacity, pressure drop, and material handling efficiency, are consistently optimized through rigorous engineering and testing. The company's commitment to quality and innovation ensures that each system is tailored to the specific needs of the client, resulting in reliable and long-lasting performance. By leveraging advanced technology and local manufacturing expertise, HeadPowder delivers solutions that enhance productivity and reduce operational costs for its customers.




