Efficient and environmentally responsible material handling is a critical consideration in modern industrial operations, particularly when dealing with bulk materials like activated carbon. Traditional methods of transporting such materials often involve manual handling, which can be labor-intensive and pose risks to both personnel and the environment. In response to these challenges, pneumatic conveying systems have emerged as a superior alternative, offering a seamless blend of efficiency, safety, and sustainability. This article explores the benefits and applications of pneumatic conveying for activated carbon particles, highlighting how this technology can transform material handling processes in various industries.
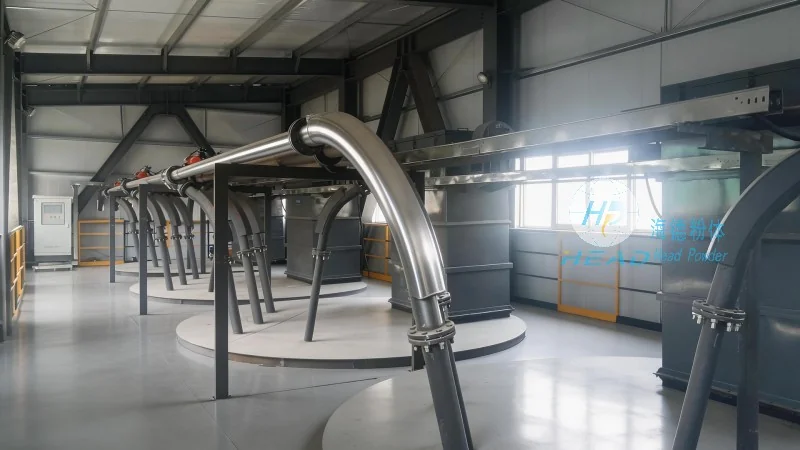
Pneumatic Conveying Systems: A Comprehensive Overview
Pneumatic conveying, also known as pneumatic transport, is a method of transporting bulk materials through a pipeline using a gas stream, typically air or other gases. Unlike traditional mechanical conveying systems, which rely on belts, buckets, or screw conveyors, pneumatic systems utilize the force of compressed air to move materials. This approach eliminates the need for multiple transfer points and reduces the risk of material spillage or contamination. For activated carbon particles, which are often used in filtration, adsorption, and other industrial processes, pneumatic conveying offers several distinct advantages.
Key Advantages of Pneumatic Conveying for Activated Carbon Particles
One of the primary benefits of pneumatic conveying is its ability to maintain the integrity of the material being transported. Activated carbon particles are delicate and can be easily damaged by mechanical abrasion or impact. Pneumatic systems use gentle air currents to move particles, minimizing wear and tear and preserving their adsorption capacity. This is particularly important in applications where the quality of the activated carbon is critical, such as in water treatment or air purification systems.
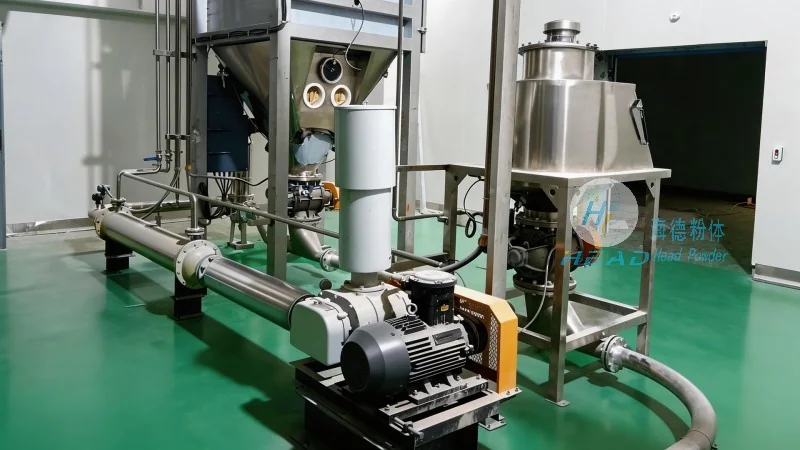
Another significant advantage is the environmental impact. Traditional bulk material handling often involves dust generation and the release of particulate matter into the environment. Pneumatic conveying systems are enclosed, which effectively contains dust and prevents it from escaping into the air. This not only improves workplace safety by reducing respiratory hazards but also aligns with environmental regulations and sustainability goals. The enclosed nature of the system also reduces the risk of material loss and contamination, making it more cost-effective in the long run.
Efficiency is another key factor that makes pneumatic conveying an attractive option. These systems can transport materials over long distances with minimal energy consumption compared to other methods. The speed and reliability of pneumatic transport allow for continuous operation, reducing downtime and increasing overall productivity. For activated carbon, which is often required in large quantities, the ability to transport it quickly and consistently is essential for maintaining production schedules and meeting demand.
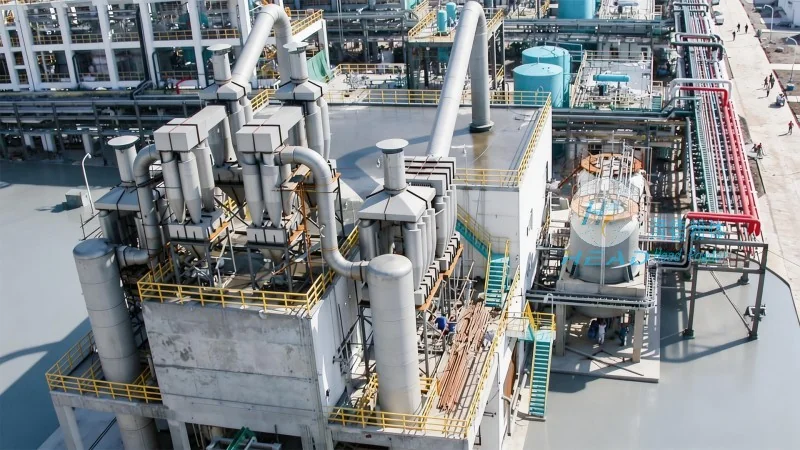
Applications and Industries Benefiting from Pneumatic Conveying
The versatility of pneumatic conveying makes it suitable for a wide range of industries that utilize activated carbon. In the water treatment industry, for example, activated carbon is used to remove impurities and contaminants from water. Pneumatic systems can efficiently transport the carbon to and from filtration units, ensuring a consistent supply of high-quality material. Similarly, in the pharmaceutical and food processing industries, where purity is paramount, pneumatic conveying helps maintain the integrity of the activated carbon, preventing cross-contamination and ensuring compliance with regulatory standards.
In the chemical and petrochemical sectors, activated carbon is used for adsorption and purification processes. Pneumatic conveying systems can handle the high volumes of carbon required in these applications while maintaining the material's quality. The ability to transport materials in a controlled environment also reduces the risk of chemical reactions or contamination, which is critical in these industries.
HeadPowder Engineering: Your Partner in Efficient Material Handling
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of advanced material handling solutions, specializing in the design and implementation of pneumatic conveying systems for activated carbon particles and other bulk materials. With years of experience in the industry, HeadPowder has developed a reputation for delivering high-quality, reliable systems that meet the unique needs of its clients. The company's commitment to innovation and customer satisfaction has made it a trusted partner for businesses seeking to improve their material handling processes.
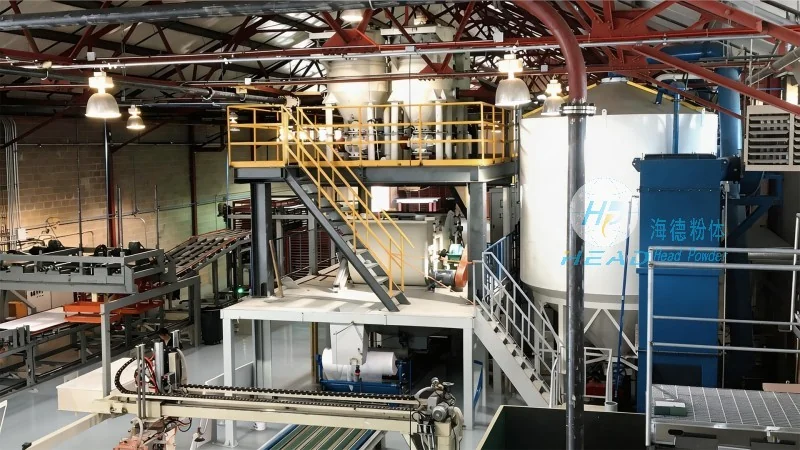
HeadPowder's expertise lies in customizing pneumatic conveying systems to suit specific operational requirements. Whether it's a small-scale application or a large industrial facility, the company works closely with clients to understand their needs and design a system that maximizes efficiency and minimizes environmental impact. The company's team of engineers and technicians is dedicated to providing comprehensive support, from initial consultation and system design to installation and ongoing maintenance.
Located in Shandong, China, HeadPowder leverages its local resources and expertise to deliver top-tier solutions. The company's facilities are equipped with state-of-the-art technology and equipment, ensuring that every system is built to the highest standards. By choosing HeadPowder, businesses can benefit from a partnership that combines technical excellence with a customer-centric approach, resulting in improved operational efficiency and a more sustainable material handling process.




