Ammonium bicarbonate, a widely used chemical in various industrial applications, requires efficient and reliable transportation methods to ensure smooth production processes. The choice of transportation method significantly impacts operational efficiency, safety, and cost-effectiveness. Among the various options available, pneumatic conveying stands out as a preferred solution for handling ammonium bicarbonate due to its unique advantages and features.
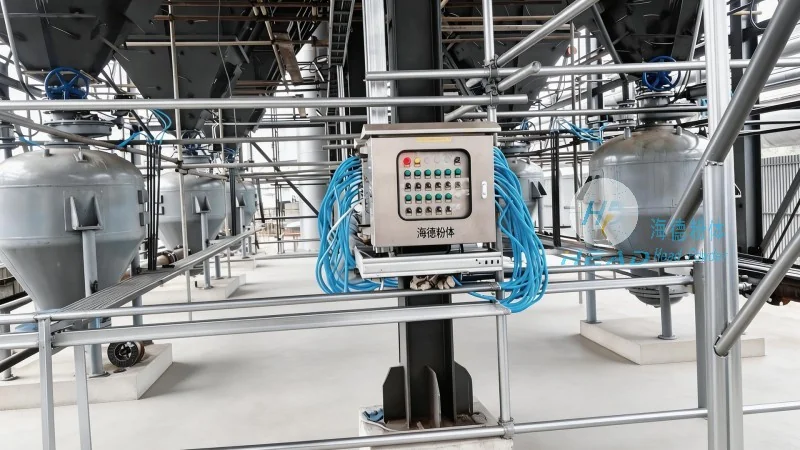
Overview of Ammonium Bicarbonate Transportation Methods
Traditional methods for transporting ammonium bicarbonate include gravity flow, mechanical conveyors (such as belt conveyors or screw conveyors), and pneumatic systems. Gravity flow relies on the material's natural weight to move it from one point to another, which is suitable for short distances and gentle slopes. However, this method is limited by the need for specific topography and is often inefficient for vertical or long-distance transport. Mechanical conveyors, while effective for bulk materials, may face challenges with ammonium bicarbonate due to its dusty nature and potential for caking, leading to increased maintenance and operational issues.
Pneumatic Conveying: A Superior Solution for Ammonium Bicarbonate
Pneumatic conveying, also known as air conveying, utilizes a stream of air to transport solid materials like ammonium bicarbonate through a pipeline system. This method offers several key advantages that make it ideal for industrial applications. First, it provides a dust-free and enclosed environment, reducing the risk of exposure to airborne particles and improving workplace safety. Second, pneumatic systems can handle both horizontal and vertical transport, making them versatile for complex layouts and varying process requirements. Third, the technology allows for precise control over material flow rates, ensuring consistent delivery to downstream processes. Additionally, pneumatic conveying minimizes material degradation and contamination, which is crucial for maintaining product quality in sensitive applications.
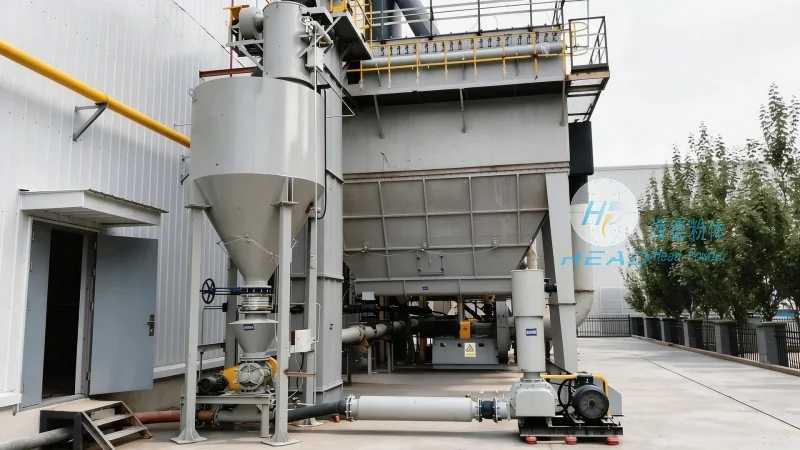
Key Advantages of Pneumatic Conveying for Ammonium Bicarbonate
When considering the transportation of ammonium bicarbonate, pneumatic conveying offers distinct benefits that enhance overall operational performance. The enclosed system prevents dust from escaping into the environment, which is essential for compliance with environmental regulations and maintaining a clean working environment. This feature also reduces the need for additional dust control measures, such as filtration systems, thereby lowering operational costs. Furthermore, the ability to transport materials over long distances without the need for intermediate storage or transfer points simplifies the overall process flow. Pneumatic systems are also highly adaptable, allowing for integration with existing production lines and easy expansion as production needs grow. The gentle handling of the material by the air stream minimizes the risk of breakage or agglomeration, preserving the physical properties of ammonium bicarbonate and ensuring consistent performance in downstream applications.
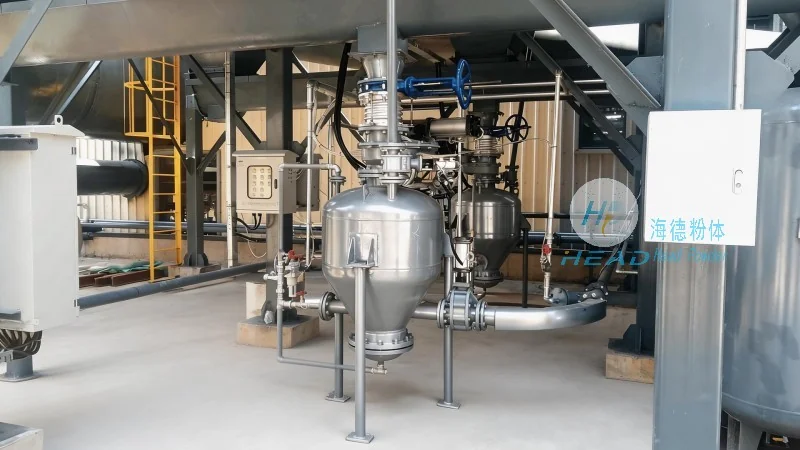
HeadPowder: Expert in Ammonium Bicarbonate Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of specialized engineering solutions for material handling, with a focus on pneumatic conveying systems tailored for ammonium bicarbonate and other similar materials. Based in Shandong, China, headpowder leverages years of industry experience to design, manufacture, and implement efficient and reliable conveying systems that meet the unique demands of industrial clients. The company's expertise lies in understanding the specific challenges associated with handling ammonium bicarbonate, such as its hygroscopic nature and potential for caking, and developing solutions that address these issues effectively.
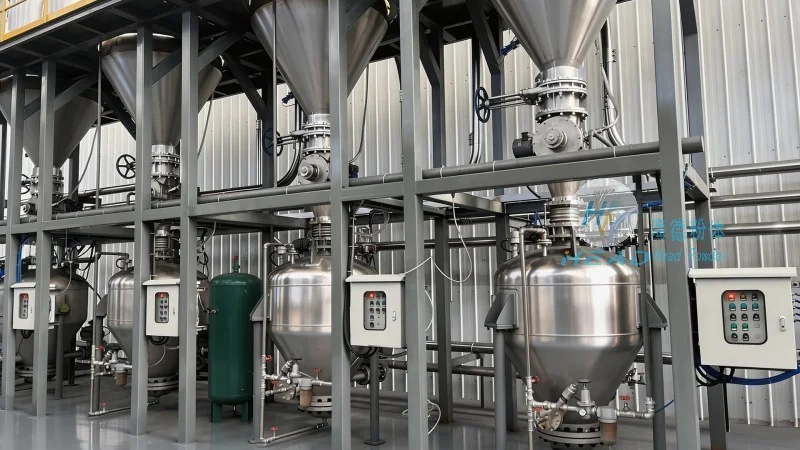
Customized Pneumatic Conveying Systems for Optimal Performance
headpowder offers customized pneumatic conveying solutions that are tailored to the specific requirements of each client. By conducting thorough assessments of production processes, material characteristics, and operational constraints, the company designs systems that maximize efficiency and minimize downtime. The solutions include a range of components such as air locks, cyclones, and control valves, all engineered to work in harmony to ensure smooth material transport. The company's commitment to quality and innovation ensures that the systems not only meet current industry standards but also adapt to future technological advancements. Clients benefit from reduced maintenance costs, increased production throughput, and improved product quality, making pneumatic conveying with headpowder's solutions a cost-effective investment for long-term operational success.
Conclusion: The Role of Pneumatic Conveying in Efficient Ammonium Bicarbonate Handling
In conclusion, pneumatic conveying represents a superior method for transporting ammonium bicarbonate, offering significant advantages over traditional approaches. The enclosed, dust-free environment, versatility in handling both horizontal and vertical transport, and precise control over material flow make it an ideal choice for industrial applications. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., clients can access customized solutions that enhance operational efficiency and ensure the safe and effective handling of ammonium bicarbonate. As industries continue to prioritize efficiency and sustainability, the adoption of advanced pneumatic conveying systems will remain crucial in maintaining competitive advantages and meeting evolving production demands.




