Small stone material conveying lines are critical components in industrial operations, particularly within mining, construction, and material processing sectors. These systems are engineered to efficiently transport bulk materials like small stones, gravel, and similar aggregates from one location to another with precision and reliability. Understanding the underlying working principle and key features of such conveying lines is essential for optimizing operational efficiency and ensuring smooth workflow in material handling processes.
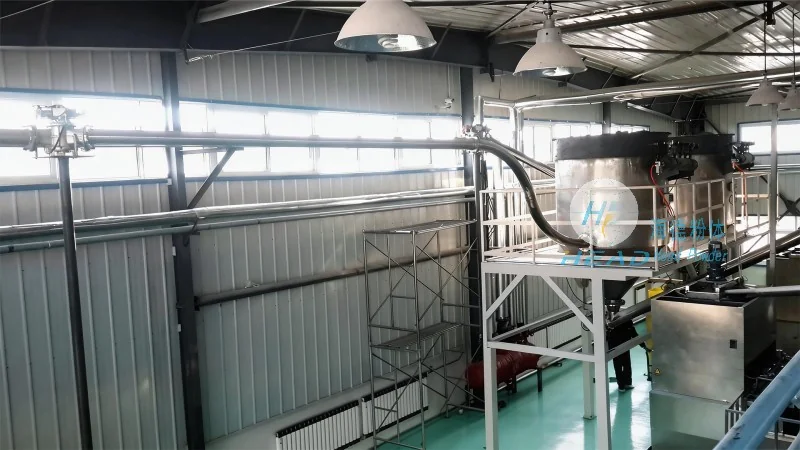
Working Principle of Small Stone Material Conveying Lines
The fundamental working principle of small stone material conveying lines centers on mechanical components that facilitate the movement of bulk materials along a defined path. Typically, these systems utilize a combination of rollers, belts, or chains to transport the material. The process initiates with the material being loaded at the input end, often via a hopper or feeder. As the material progresses along the conveyor, it is guided by mechanical elements such as idlers, drive pulleys, and tensioning mechanisms. The drive system, commonly powered by electric motors, supplies the necessary force to propel the material forward. The speed and direction of material flow can be controlled by adjusting motor speed or employing variable frequency drives (VFDs), enabling precise management of the conveying process. At the output end, the material is discharged into a storage bin, truck, or another processing unit. This continuous movement ensures efficient material transport without manual handling, reducing labor costs and enhancing workplace safety.
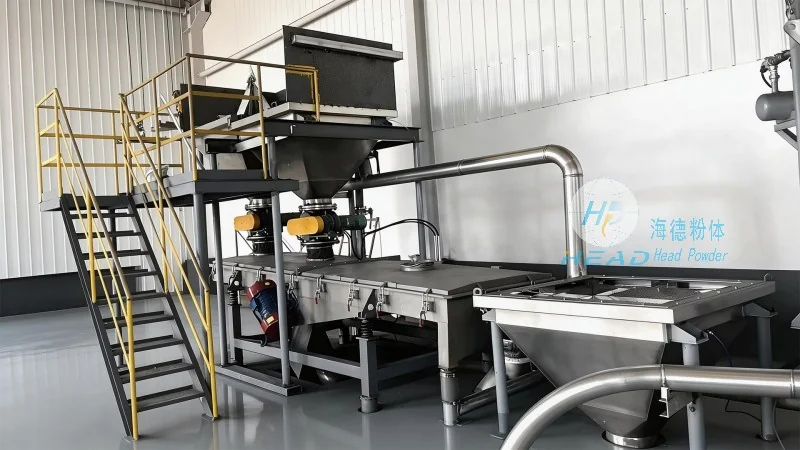
Key Features of Small Stone Material Conveying Lines
Small stone material conveying lines are distinguished by several key features that enhance performance and adaptability across diverse industrial applications. One primary feature is robust construction, designed to withstand the abrasive nature of small stones and heavy loads. Components like conveyor belts or chains are often made from durable materials such as rubber or metal, ensuring long-term durability and minimal maintenance. Another crucial feature is adjustable speed control, allowing operators to modify conveying speed based on material type and processing requirements. This flexibility is particularly valuable in applications where varying material sizes or processing stages demand different speeds. Additionally, these systems frequently include safety features like emergency stop buttons, overload protection, and protective guards to prevent accidents and comply with safety regulations. The modular design of many small stone conveying lines also enables easy installation and customization, adapting to specific site requirements. Furthermore, integration of sensors and monitoring systems provides real-time data on material flow, enabling proactive maintenance and optimizing operational efficiency.
Applications and Benefits in Industrial Settings
Small stone material conveying lines find extensive application in industries including mining, construction, and aggregate processing. In mining operations, these systems transport crushed stones from extraction sites to processing facilities for further refinement. In construction, they move gravel and sand from storage to construction sites, supporting road, building, and infrastructure development. The benefits of using small stone conveying lines in these contexts are significant. Firstly, they automate material handling, reducing time and labor for manual transport. Secondly, they enhance safety by minimizing worker exposure to heavy or bulky materials, lowering injury risks. Thirdly, they maintain consistent material quality by controlling flow and preventing degradation or contamination. Additionally, modern systems’ energy efficiency, often via VFD technology, reduces operational costs and environmental impact. Overall, small stone material conveying lines play a vital role in streamlining industrial processes and supporting efficient construction material production.
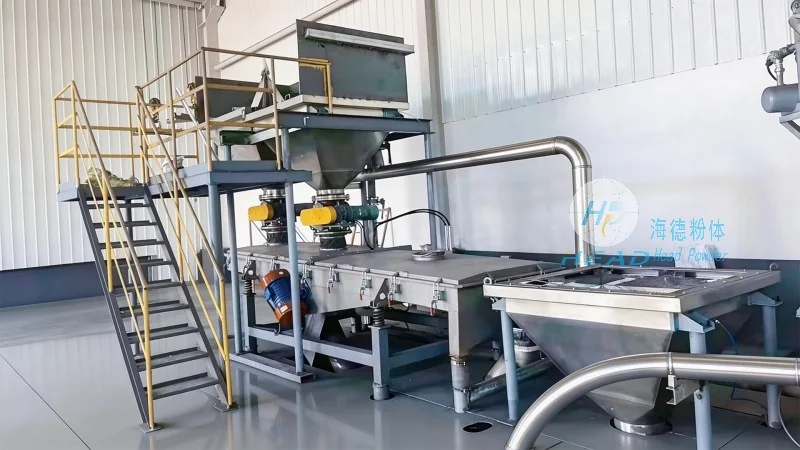
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer in the material handling industry, specializes in designing, manufacturing, and supplying high-quality small stone material conveying lines. With years of experience and a commitment to innovation, the company has established itself as a trusted partner for businesses seeking reliable and efficient material handling solutions. HeadPowder’s products are engineered to meet specific industry needs, ensuring durability, performance, and safety. The company’s expert team collaborates closely with clients to understand requirements and provide customized solutions that enhance operational efficiency and reduce costs. HeadPowder’s facilities are equipped with advanced manufacturing technologies and quality control measures, ensuring each product meets high performance and reliability standards. The company’s dedication to customer satisfaction and technological advancement has made it a preferred choice for businesses in mining, construction, and material processing sectors. With strong presence in China and global reach, HeadPowder continues to advance material handling technologies and support clients’ business growth.




