High-pressure dilute-phase material handling is a critical technology in the field of bulk material transportation, offering efficient and reliable solutions for various industrial applications. This article aims to explore the working principles and key characteristics of this system, providing a comprehensive understanding for professionals and potential users.
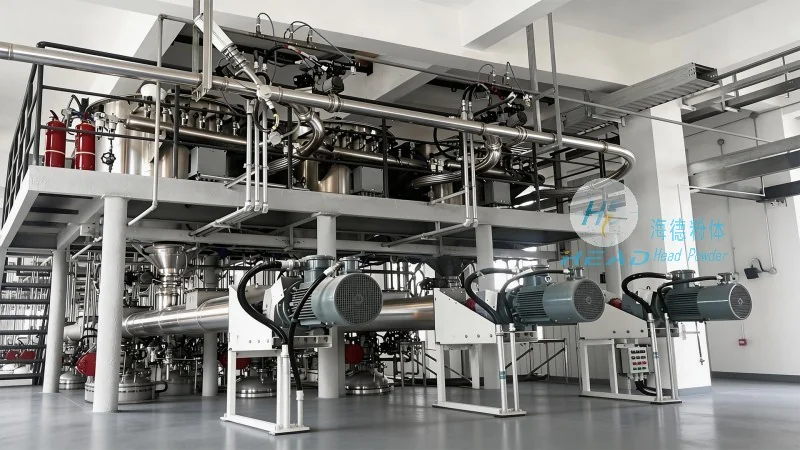
Introduction to High-Pressure Dilute-Phase Material Handling
High-pressure dilute-phase material handling systems are designed to transport bulk materials such as powders, granules, and fine particles through pipelines under high pressure. Unlike dense-phase or pneumatic conveying systems, dilute-phase systems operate by suspending the material in a stream of air or gas, creating a low concentration of particles in the conveying medium. This method is particularly effective for long-distance and high-capacity material transport, making it a preferred choice in industries like mining, chemicals, food processing, and pharmaceuticals.
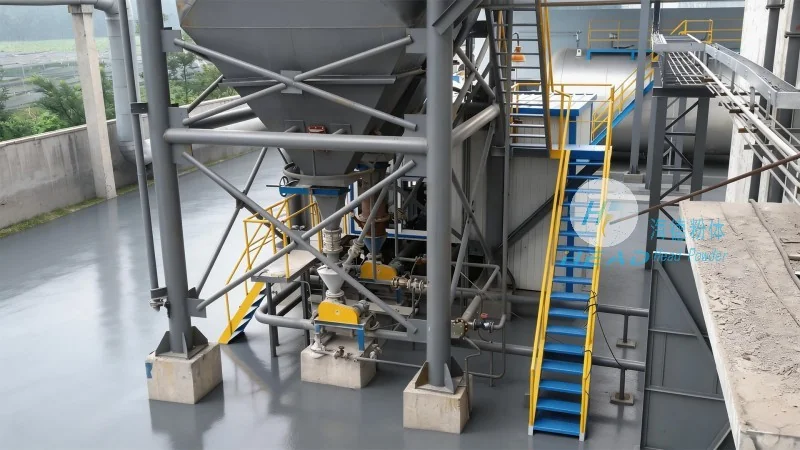
The Working Principle of High-Pressure Dilute-Phase Material Handling
The core working principle of high-pressure dilute-phase material handling involves the use of a high-pressure air compressor to generate a powerful air stream. The material is then introduced into the pipeline at the inlet, where it is mixed with the high-velocity air. The air stream, moving at speeds typically ranging from 20 to 100 meters per second, suspends the particles and propels them forward through the pipeline. The system utilizes a series of components, including a blower, air filter, material feeder, and pipeline network, to ensure consistent and efficient material transport. The pressure within the system is maintained at a level sufficient to overcome friction losses and elevation changes, ensuring the material reaches its destination without clogging or degradation.
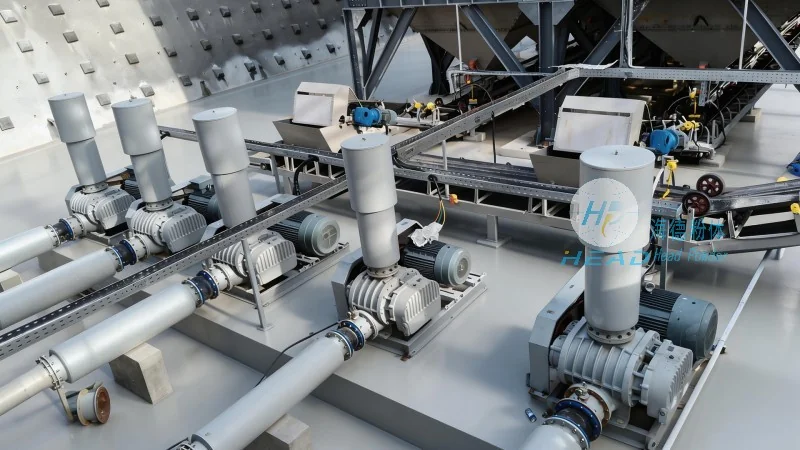
Key Characteristics of High-Pressure Dilute-Phase Material Handling
Several distinct characteristics define high-pressure dilute-phase material handling systems, contributing to their effectiveness and adaptability in industrial settings. Firstly, the system offers high transport capacity, capable of moving large volumes of material over long distances with minimal energy consumption compared to other methods. Secondly, it provides excellent material handling flexibility, as it can handle a wide range of particle sizes and shapes, from fine powders to coarse granules. Thirdly, the system ensures minimal material degradation, as the particles are suspended in air rather than being subjected to high shear forces or mechanical abrasion. Additionally, high-pressure dilute-phase systems are relatively simple in design and operation, with fewer moving parts compared to dense-phase systems, leading to lower maintenance requirements and operational costs. Finally, the technology allows for easy integration with existing industrial infrastructure, making it a viable solution for both new and retrofit applications.
Applications and Advantages in Industrial Context
High-pressure dilute-phase material handling systems find extensive applications across various industries due to their versatility and efficiency. In the mining industry, they are used to transport ore and tailings from processing plants to storage facilities or disposal sites. In the chemical industry, they handle raw materials and finished products, such as powders and granules, between processing units. The food and pharmaceutical industries benefit from the system's ability to maintain product purity and quality, as the air used in the conveying process is often filtered and treated to meet stringent hygiene standards. The primary advantages of this technology include its ability to handle large volumes of material over long distances, its low operational costs, and its adaptability to different material types and processing requirements. Furthermore, the system's compact design and minimal space requirements make it suitable for installation in confined areas, a common challenge in modern industrial facilities.
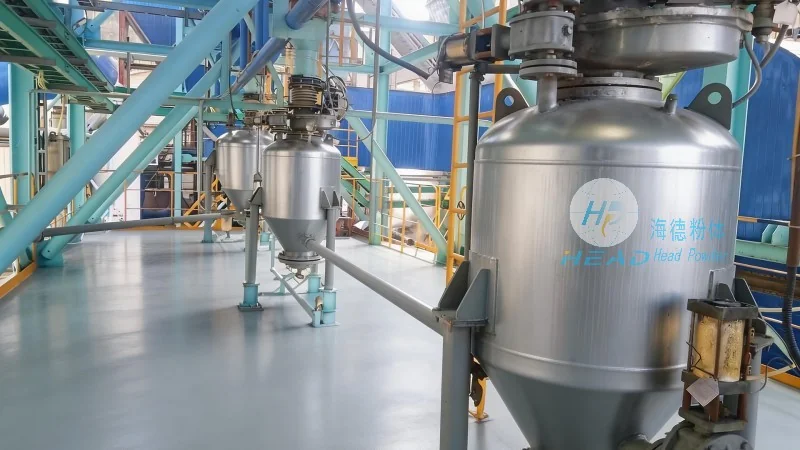
Conclusion and Company Overview
High-pressure dilute-phase material handling represents a sophisticated and efficient solution for bulk material transportation, combining advanced engineering principles with practical application. The system's working principle, characterized by high-pressure air suspension and efficient pipeline transport, ensures reliable and consistent material movement. Its key characteristics, including high capacity, flexibility, and low degradation, make it an ideal choice for diverse industrial needs. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing, manufacturing, and implementing high-quality high-pressure dilute-phase material handling systems tailored to the specific requirements of clients. With a strong commitment to innovation and customer satisfaction, the company has established itself as a trusted partner in the industry, delivering reliable solutions that enhance operational efficiency and productivity. Based in Shandong, China, HeadPowder Engineering leverages its expertise and experience to provide cutting-edge material handling technologies that meet the evolving demands of modern industrial applications.




