Understanding the working principles and features of dust-free material handling systems is crucial for industries that require maintaining a clean and controlled environment. These systems are designed to transport materials without generating dust or particles, ensuring compliance with stringent environmental and safety standards. The technology behind these systems involves advanced engineering solutions that integrate precision components and efficient operational mechanisms.
Working Principle of Dust-Free Material Conveying
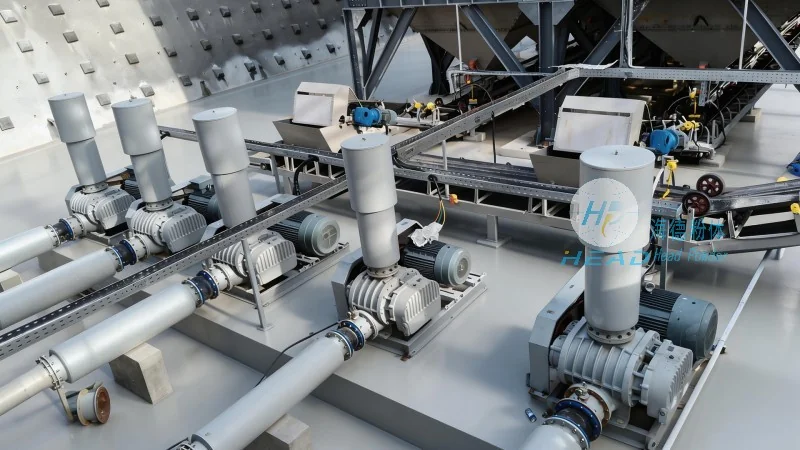
The core working principle of dust-free material handling systems revolves around the use of enclosed or sealed conveyor mechanisms. Unlike traditional open conveyors that may release dust into the air, these systems employ enclosed structures that trap and contain particulate matter. The process typically begins with the loading of materials into the system, where they are then transported through a series of rollers, belts, or chains within a sealed housing. This enclosure prevents dust from escaping and ensures that the material remains in a controlled environment throughout the transport process. Additionally, the systems often incorporate filtration and air circulation mechanisms to maintain air quality within the enclosed space. The working principle also includes the use of low-dust materials for components such as belts and rollers, further minimizing the generation of particulate matter. Motor-driven systems provide the necessary power to move the materials, with variable speed controls allowing for precise adjustment based on the material's characteristics and handling requirements. The entire process is designed to be efficient, reliable, and safe, ensuring that the material is transported without compromising the cleanliness of the surrounding environment.
Key Features of Dust-Free Material Transport Solutions
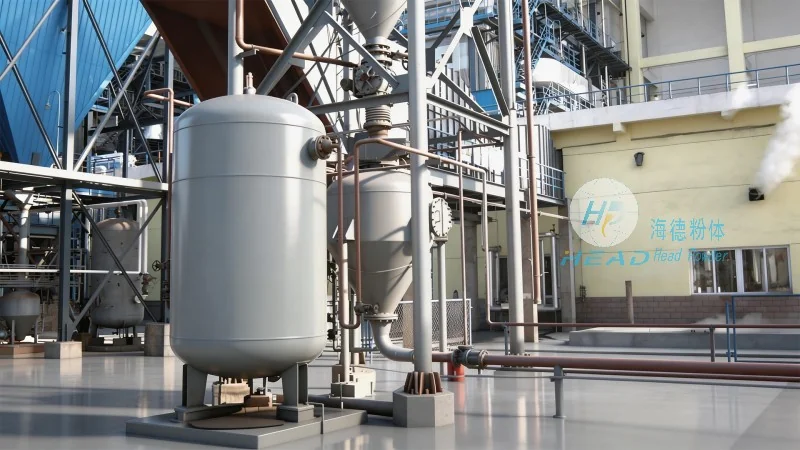
Dust-free material handling systems offer several key features that make them ideal for applications in pharmaceutical, food processing, electronics, and other industries where contamination control is paramount. One of the primary features is the enclosed design, which provides a fully sealed environment that prevents dust and contaminants from entering or exiting the system. This feature is critical for maintaining product quality and preventing cross-contamination. Another important feature is the use of high-quality, low-dust materials for all components, including conveyor belts, rollers, and housing parts. These materials are selected to minimize wear and tear, reducing the generation of dust particles over time. The systems also incorporate advanced filtration systems that capture any dust that may be generated during operation, ensuring that the air within the system remains clean and free from contaminants. Additionally, the design often includes easy access points for maintenance and cleaning, allowing for quick and efficient upkeep to maintain the system's performance and cleanliness. The systems are typically equipped with sensors and monitoring devices that provide real-time feedback on operational parameters, such as temperature, pressure, and material flow, enabling proactive maintenance and ensuring consistent performance. Energy efficiency is another notable feature, with many systems incorporating energy-saving technologies like variable frequency drives to reduce power consumption while maintaining optimal performance. The robust construction of these systems ensures durability and long-term reliability, making them suitable for continuous operation in demanding industrial environments.
Applications and Benefits in Industrial Settings
Dust-free material handling systems are widely used in various industrial applications where maintaining a clean environment is essential. In the pharmaceutical industry, these systems are used to transport raw materials and finished products, ensuring that they remain free from contaminants that could affect product safety and efficacy. The food processing industry also relies on these systems for handling ingredients and packaging materials, preventing cross-contamination and maintaining food safety standards. The electronics industry uses dust-free conveyors to transport sensitive components, protecting them from dust and moisture that could damage the products. Other applications include the chemical and automotive industries, where these systems help maintain a controlled environment for processing and assembly tasks. The benefits of using dust-free material handling systems extend beyond just cleanliness; they also contribute to improved operational efficiency and reduced downtime. By preventing dust buildup and contamination, these systems reduce the need for frequent cleaning and maintenance, leading to lower operational costs. Additionally, the enclosed design helps protect the materials being transported from external factors such as dust, moisture, and debris, ensuring that they remain in optimal condition throughout the transport process. The reliability of these systems also contributes to increased productivity, as they can operate continuously without interruptions, meeting the demands of high-volume production environments.
Conclusion and Company Overview
In conclusion, dust-free material handling systems are advanced solutions that combine efficient material transport with stringent contamination control. Their working principles, based on enclosed mechanisms and low-dust components, ensure that materials are moved safely and cleanly. The key features, including sealed designs, high-quality materials, and advanced filtration, make these systems suitable for critical applications in various industries. The benefits of using such systems include improved product quality, reduced maintenance costs, and enhanced operational efficiency. Shandong HeadPowder Engineering Co., Ltd., a leading provider in this field, specializes in designing and manufacturing these systems to meet the diverse needs of industrial clients. With a focus on precision engineering and customer satisfaction, the company offers tailored solutions that ensure compliance with industry standards and contribute to the success of their clients' operations. The company's commitment to quality and innovation has made it a trusted partner for businesses seeking reliable dust-free material handling solutions. By leveraging advanced technology and expertise, Shandong HeadPowder Engineering Co., Ltd. continues to provide cutting-edge systems that support the evolving needs of modern industries.




