HeadPowder, a leading manufacturer in the field of powder handling technology, specializes in the design and production of advanced sugar powder conveying equipment. Based in Shandong, China, the company has established itself as a trusted partner for industries requiring efficient and reliable sugar powder transportation solutions.
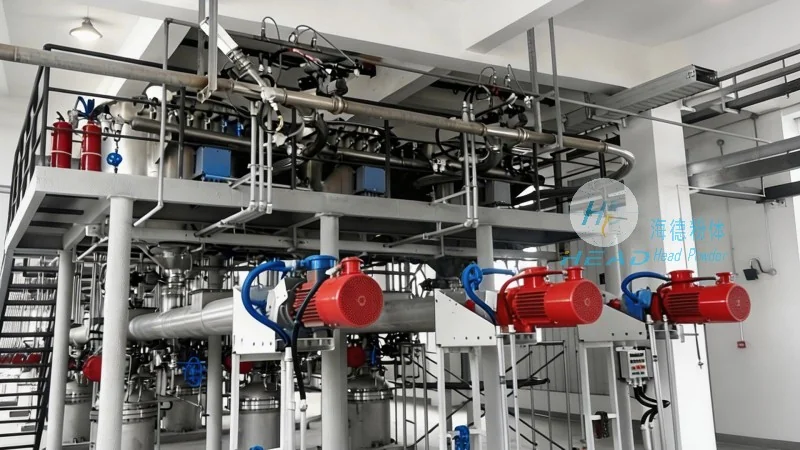
Working Principle of Sugar Powder Conveying Equipment
The core working principle of sugar powder conveying equipment involves the use of mechanical systems to transport granular or powdered sugar from one location to another. These systems typically employ a combination of components such as hoppers, feeders, conveyors, and control mechanisms. The process begins with the sugar being fed into a hopper, where it is stored and prepared for transport. From the hopper, the sugar is then transferred to a feeder, which regulates the flow rate and ensures consistent material delivery. The feeder connects to a conveyor system, which can be either pneumatic (air-powered) or mechanical (belt-driven), depending on the specific application requirements. Pneumatic conveyors use compressed air to move the sugar particles through a pipeline, while mechanical conveyors rely on belts, screws, or buckets to transport the material. The conveyor system transports the sugar to the desired destination, such as a storage silo, processing unit, or packaging line. Control systems, often integrated with sensors and automation technology, monitor the flow rate, pressure, and other parameters to maintain optimal operation and prevent blockages or overloading. This integrated approach ensures that the sugar powder is conveyed safely and efficiently, minimizing product degradation and maximizing system performance.
Key Features of Sugar Powder Conveying Equipment
Sugar powder conveying equipment from HeadPowder is designed with several key features that enhance performance, reliability, and user experience. One of the primary features is the ability to handle fine or cohesive powders, such as sugar, without causing caking or agglomeration. The equipment incorporates anti-caking mechanisms, such as vibration or air agitation, to maintain the flowability of the material. Another important feature is the adjustable flow control, which allows operators to regulate the speed of sugar delivery based on production needs. This flexibility is crucial for maintaining consistent product quality and preventing overfilling or underfilling. The equipment also features robust construction, using high-quality materials like stainless steel and corrosion-resistant components, to withstand the harsh conditions of sugar processing environments. Additionally, the systems are equipped with safety features, including overload protection and emergency stop buttons, to ensure operator safety and prevent equipment damage. The integration of advanced automation and monitoring systems provides real-time data on system performance, enabling proactive maintenance and reducing downtime. These features collectively contribute to the efficiency and reliability of sugar powder conveying operations.
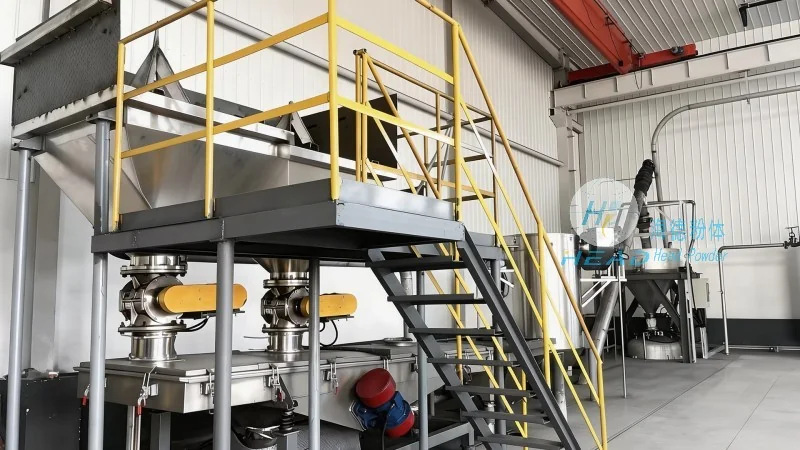
Advantages of Using HeadPowder's Conveying Solutions
Implementing sugar powder conveying equipment from HeadPowder offers several advantages for sugar processing industries. The primary advantage is improved operational efficiency, as the equipment ensures consistent and continuous sugar transport, reducing bottlenecks and increasing production throughput. The use of advanced control systems minimizes human intervention, leading to lower labor costs and enhanced productivity. Another significant advantage is the reduction in product loss and contamination. The sealed and enclosed design of the conveying systems prevents dust and moisture from entering or exiting, maintaining the purity of the sugar. This is particularly important for food-grade applications where product quality and safety are paramount. The equipment also contributes to cost savings by minimizing material waste and reducing the need for manual handling, which can be labor-intensive and prone to errors. Furthermore, the durability and low maintenance requirements of HeadPowder's systems result in long-term cost savings and extended equipment lifespan. The company's commitment to quality and innovation ensures that their conveying solutions are tailored to meet the specific needs of each client, providing customized solutions that enhance overall operational performance.
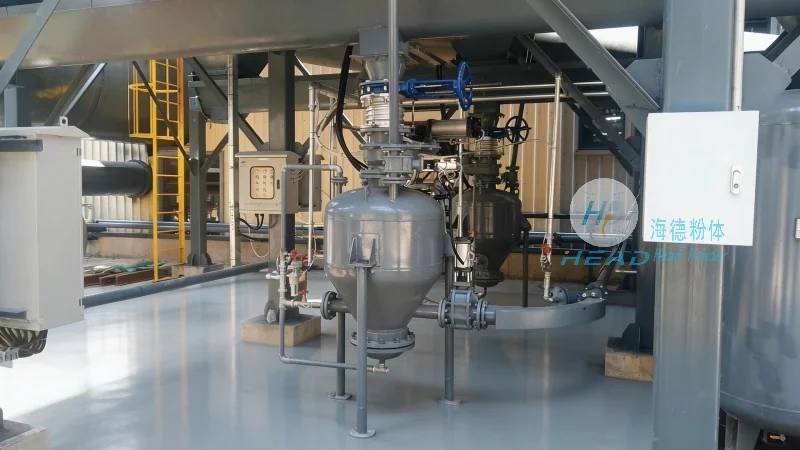
Application Scenarios and Industry Impact
Sugar powder conveying equipment from HeadPowder is widely used in various stages of the sugar processing industry, from raw material handling to final product packaging. In sugar refineries, the equipment is used to transport raw sugar from storage silos to processing units, ensuring a steady supply of material for refining. During the refining process, the equipment conveys refined sugar to packaging lines, where it is prepared for distribution. In sugar mills, the equipment handles raw sugar and molasses, facilitating the conversion of raw materials into refined sugar. The systems are also used in sugar storage facilities, where they transport sugar from processing units to storage silos, maintaining inventory levels and ensuring availability for downstream operations. The versatility of HeadPowder's conveying solutions makes them suitable for both large-scale industrial applications and smaller processing facilities. The equipment's ability to handle different sugar types, such as white sugar, brown sugar, and powdered sugar, makes it a versatile solution for various production needs. The impact of using these systems is significant, as they contribute to the overall efficiency and profitability of sugar processing operations. By improving material flow and reducing downtime, the equipment helps companies maintain competitive advantages in the market.
Conclusion and Company Overview
HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading provider of sugar powder conveying equipment, offering advanced solutions that enhance the efficiency and reliability of sugar processing operations. The company's equipment is designed based on a deep understanding of the unique challenges faced by the sugar industry, including the need to handle fine powders, maintain product quality, and ensure operational safety. By integrating innovative technologies and robust construction, HeadPowder's conveying systems provide superior performance and durability. The company's commitment to customer satisfaction and continuous improvement has established it as a trusted partner for industries worldwide. With a focus on quality, innovation, and customer support, HeadPowder continues to deliver cutting-edge solutions that meet the evolving needs of the sugar processing industry. Whether for large-scale refineries or smaller processing facilities, HeadPowder's sugar powder conveying equipment is the ideal choice for achieving optimal performance and operational efficiency.




