Pneumatic conveying systems represent a sophisticated and efficient method for transporting powdered materials, such as bean powder, from one location to another. Unlike traditional mechanical systems that rely on belts, buckets, or screws, pneumatic conveying utilizes air flow to move particulate materials through a sealed pipeline. This approach not only enhances operational efficiency but also ensures the integrity and quality of the material being transported. For industries dealing with food-grade products like bean powder, the hygienic and enclosed nature of pneumatic conveying is particularly advantageous, as it minimizes the risk of contamination and product degradation.
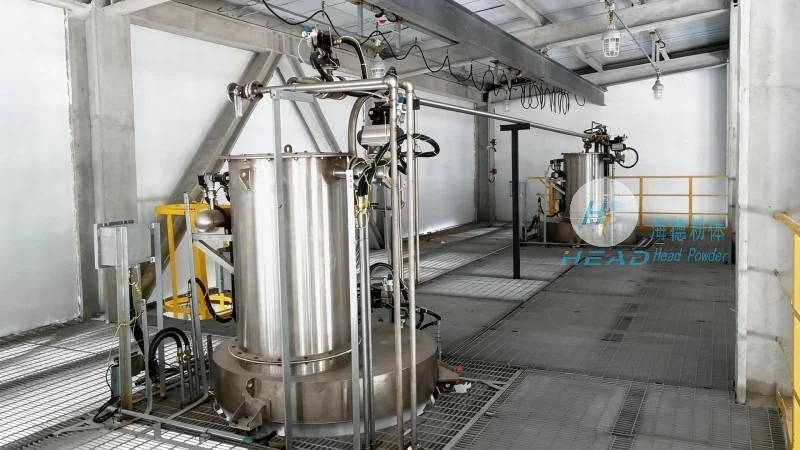
Key Advantages of Pneumatic Conveying Systems
Implementing a pneumatic conveying system for bean powder offers several distinct advantages that make it a preferred choice for many manufacturers. First, the enclosed system provides a hygienic environment, which is critical for food processing applications. By containing the material within the pipeline, the system prevents exposure to external contaminants, dust, or moisture, thereby maintaining the purity and quality of the bean powder. Second, pneumatic conveying reduces operational downtime and maintenance requirements compared to mechanical systems. The absence of moving parts like belts or screws minimizes the risk of wear and tear, leading to lower maintenance costs and extended system life. Third, the technology is highly versatile, capable of handling a wide range of particle sizes, densities, and moisture contents. This adaptability makes it suitable for various processing stages, from raw material handling to final product packaging.
How Pneumatic Conveying Works: The Mechanics Behind the Process
The operation of a pneumatic conveying system for bean powder is based on the principle of creating a pressure differential within a pipeline. The system typically consists of a hopper or feeder that supplies the bean powder, a conveyor line (pipeline) that transports the material, a separator or cyclone to separate the material from the air, and a dust collector to capture any airborne particles. The feeder is designed to control the flow rate of the material, ensuring a consistent and controlled feed into the system. The pipeline is usually made of stainless steel or other corrosion-resistant materials to prevent contamination and ensure durability. The separator plays a critical role in separating the material from the air, allowing the material to be discharged while the air is filtered and recycled back into the system.
There are two primary types of pneumatic conveying: pressure and vacuum systems. Pressure systems use positive pressure to push the material forward, while vacuum systems use negative pressure to pull the material. For bean powder, a pressure system is often preferred due to its ability to handle higher material loads and longer distances without significant pressure loss. The pressure system works by introducing compressed air into the pipeline, which entrains the bean powder and propels it toward the destination. The air velocity within the pipeline is carefully controlled to ensure proper material transport without causing excessive wear on the system components.
Components and Design Considerations
Each component of a pneumatic conveying system is carefully designed to optimize performance and ensure reliability. The hopper or feeder is a key component that regulates the flow of bean powder into the system. It is typically equipped with a rotary valve or a screw feeder to maintain a consistent feed rate. The conveyor line, or pipeline, is usually made of stainless steel or polyethylene, depending on the material being conveyed. The choice of material depends on factors such as the corrosiveness of the bean powder and the required durability. The pipeline is often equipped with bends and elbows to direct the material flow, and these components are designed to minimize pressure loss and prevent material buildup.
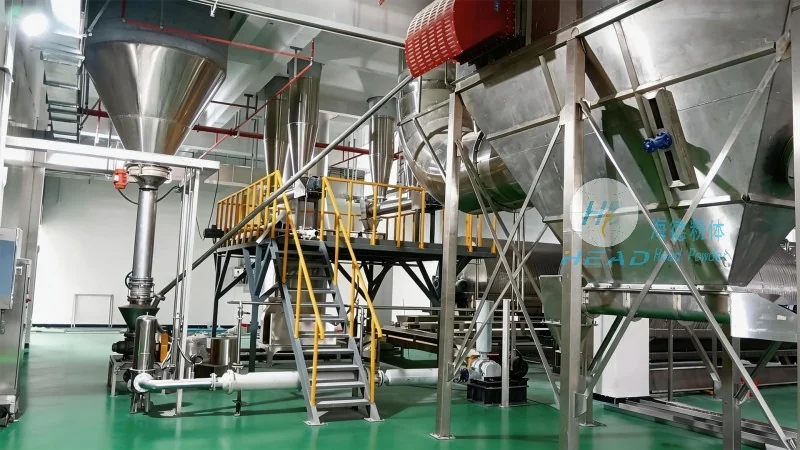
The separator or cyclone is another critical component that separates the bean powder from the air. The separator works by using centrifugal force to separate the heavier material from the lighter air. The material is discharged from the bottom of the separator, while the air is filtered and recycled back into the system. The dust collector, which is often integrated with the separator, captures any fine particles that may escape, ensuring that the air is clean and free of contaminants. This recycling of air reduces energy consumption and maintains the efficiency of the system.
Applications in the Food Industry: Ensuring Quality and Efficiency
Pneumatic conveying is widely used in the food processing industry, particularly for handling products like bean powder. The technology is ideal for applications where product purity and hygiene are paramount. For example, in the production of instant coffee or other powdered food products, pneumatic conveying ensures that the bean powder is transported without any contamination or degradation. The enclosed system also helps maintain the moisture content of the powder, preventing clumping or caking during transport. Additionally, the system can be integrated with other processing equipment, such as mixers or packaging machines, to create a seamless production line.
In the pharmaceutical industry, pneumatic conveying is used to transport powdered ingredients for drug manufacturing. The hygienic and enclosed nature of the system ensures that the ingredients are free from contamination, which is crucial for maintaining the safety and efficacy of the final product. The system's ability to handle fine powders without degradation makes it suitable for sensitive pharmaceutical applications.
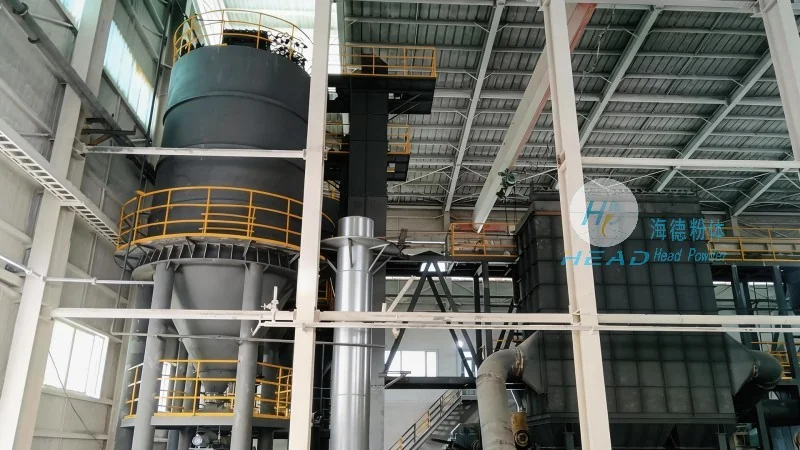
Choosing the Right Pneumatic Conveying System for Bean Powder
When selecting a pneumatic conveying system for bean powder, several factors need to be considered to ensure optimal performance and efficiency. The first is the material's properties, such as particle size, density, and moisture content. These factors influence the system's design and components. For instance, finer particles may require a higher air velocity to ensure proper entrainment, while larger particles may need a different feeder design to prevent blockages. The second factor is the distance and height the material needs to be conveyed. Longer distances may require booster pumps or larger pipelines to maintain sufficient pressure. The third factor is the required capacity, which determines the size of the feeder and pipeline. It is essential to work with a reputable supplier who can provide a customized system tailored to the specific needs of the application.
Working with a supplier like Shandong HeadPowder Engineering Co., Ltd. (headpowder) can help ensure that the right system is selected for the job. Headpowder specializes in designing and manufacturing pneumatic conveying systems that meet the unique requirements of each client. The company's expertise lies in providing solutions that enhance production efficiency, maintain product quality, and comply with industry standards. By leveraging advanced technology and years of experience, headpowder helps clients improve their processing capabilities and achieve their business goals.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of pneumatic conveying systems and related equipment. With headquarters in Shandong, China, the company has established itself as a trusted partner for industries requiring efficient and reliable material handling solutions. Headpowder's products are designed to meet the specific needs of the food, pharmaceutical, and chemical industries, ensuring that clients receive high-quality systems that enhance their operational performance.
The company's commitment to quality and innovation has earned it a reputation for excellence in the industry. Headpowder's team of engineers and technicians work closely with clients to understand their requirements and develop customized solutions. The company's manufacturing facilities are equipped with advanced technology and quality control measures to ensure that each system meets the highest standards. By providing comprehensive support, from design and installation to maintenance and after-sales service, headpowder helps clients maximize the value of their investment and achieve long-term success.




