HeadPowder Engineering Co., Ltd., a prominent enterprise based in Shandong, China, specializes in the development and manufacturing of advanced pneumatic conveying systems tailored for the transportation of lysine, a vital amino acid in animal feed and food production. The lysine pneumatic conveying system is a critical piece of equipment for industries that require efficient, dust-free, and automated handling of bulk lysine powder. This system is designed to ensure minimal product loss, maintain product quality, and enhance overall operational efficiency in material handling processes.
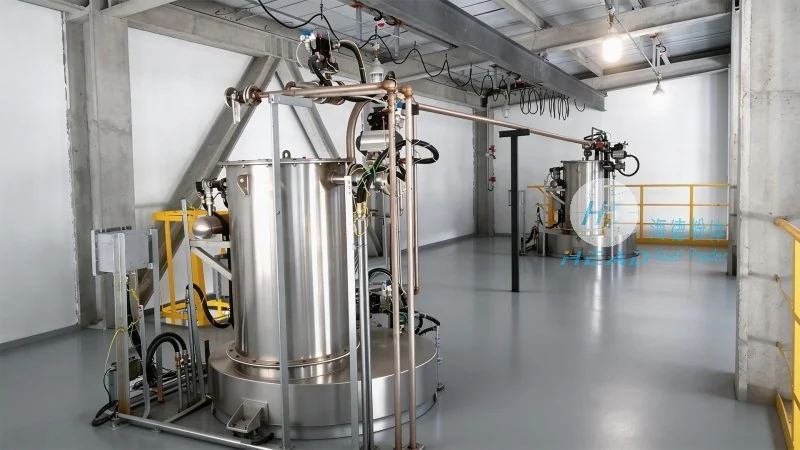
Structural Principles and Operational Mechanism
The lysine pneumatic conveying system operates on the principle of pneumatic transport, which involves the use of air or gas to move solid materials through a pipeline. The system's structure comprises several key components that work in concert to achieve seamless material transport. The primary components include a storage hopper, a rotary airlock valve, a conveying line (either positive pressure or negative pressure), and a product receiver. The storage hopper is designed to hold a large quantity of lysine powder, ensuring a consistent supply to the system. The rotary airlock valve acts as a controlled discharge mechanism, regulating the flow of lysine into the conveying line to prevent overloading or clogging. The conveying line is the core of the system, where the lysine powder is transported by the air flow. In positive pressure systems, compressed air is used to push the material through the pipeline, while in negative pressure (air-assisted) systems, a vacuum is created to draw the material. The product receiver collects the lysine powder at the end of the conveying line, ready for further processing or packaging. The system's design ensures that the material is transported with minimal degradation, maintaining its purity and nutritional value.
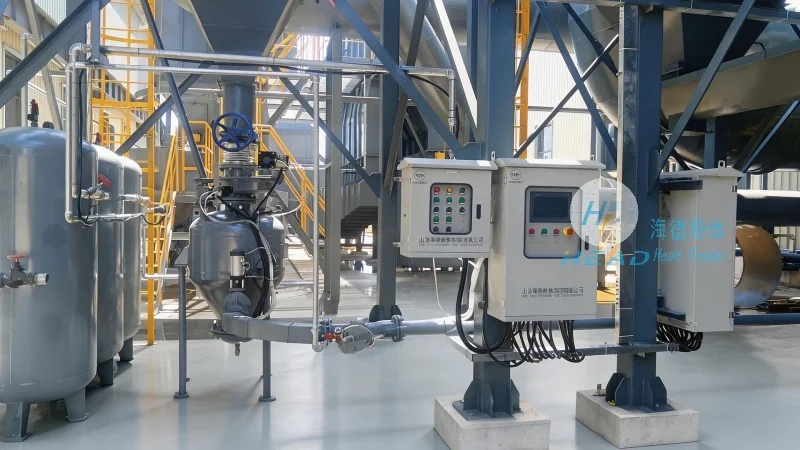
Key Features and Technical Advantages
HeadPowder's lysine pneumatic conveying system is equipped with several features that enhance its performance and reliability. The system utilizes a closed-loop design, which eliminates dust emissions and provides a hygienic environment, crucial for food and feed industries. This design also helps in maintaining product quality by preventing contamination from external sources. The system is designed for high conveying efficiency, with the ability to transport lysine over long distances with minimal pressure drop. This ensures that the material reaches its destination without significant loss of quality or performance. The equipment is also equipped with advanced control systems, allowing for precise regulation of flow rates, pressure, and temperature. This level of control enables operators to optimize the system's performance and adapt to changing production demands. Additionally, the system is constructed with high-quality materials that are resistant to corrosion and wear, ensuring long-term durability and low maintenance costs. The modular design of the system allows for easy installation and integration into existing production lines, reducing downtime and installation costs.
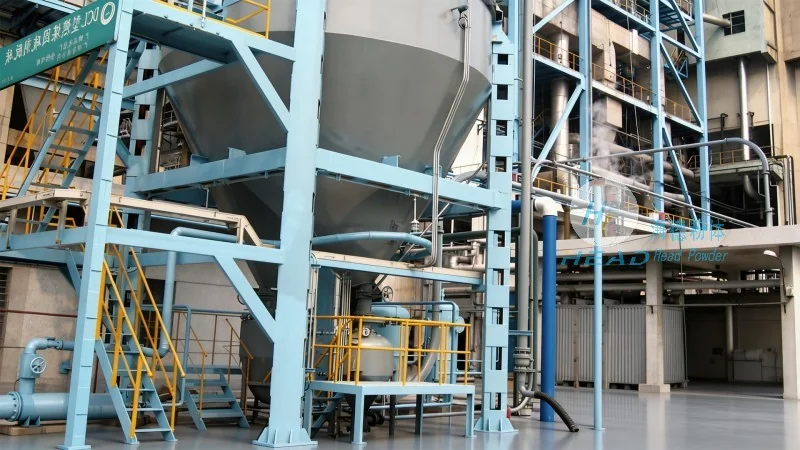
Application and Industry Impact
The lysine pneumatic conveying system is widely adopted in the animal feed and food processing industries due to its efficiency and reliability. In animal feed production, the system ensures that lysine is transported from storage to mixing plants without any loss or contamination, maintaining the nutritional quality of the final feed products. In food processing, the system is used to transport lysine for use in food supplements and fortified products, where consistent quality and purity are essential. The system's ability to handle bulk lysine powder in a controlled manner helps manufacturers meet production targets while adhering to strict quality control standards. By providing a reliable and efficient solution for lysine transportation, HeadPowder's equipment contributes to the overall productivity and profitability of its clients' operations. The system's design and performance are tailored to meet the specific needs of each client, ensuring that the equipment integrates seamlessly into existing production lines and enhances overall operational efficiency. The use of this system not only improves the safety and hygiene of the workplace but also reduces the risk of product recalls due to contamination, thereby enhancing the reputation and market position of the end-users.




