

Operation Process and Working Principle of Intelligent Tonne Bag Loading Station for Powder Pneumati
HeadPowder, a leading provider of powder handling solutions, specializes in advanced equipment designed to enhance efficiency and reliability in industrial material processing. This article delves into the operation process and working principle of the intelligent tonne bag loading station for powder pneumatic conveying systems, highlighting key components and the systematic approach to material transfer.
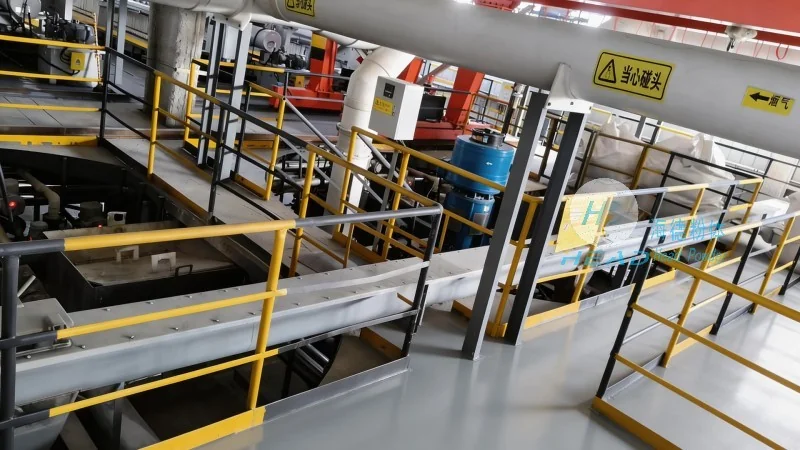
Overview of the Intelligent Tonne Bag Loading Station
The intelligent tonne bag loading station is a sophisticated system engineered to automate the handling of bulk powders from tonne bags into pneumatic conveying lines. Developed by Shandong HeadPowder Engineering Co., Ltd., based in China, this equipment integrates cutting-edge technology to streamline operations in various industrial sectors, including chemical, pharmaceutical, food, and agricultural processing. The station is designed to ensure precise and safe material transfer, minimizing human intervention and reducing the risk of contamination or loss.
Working Principle of the Pneumatic Conveying System
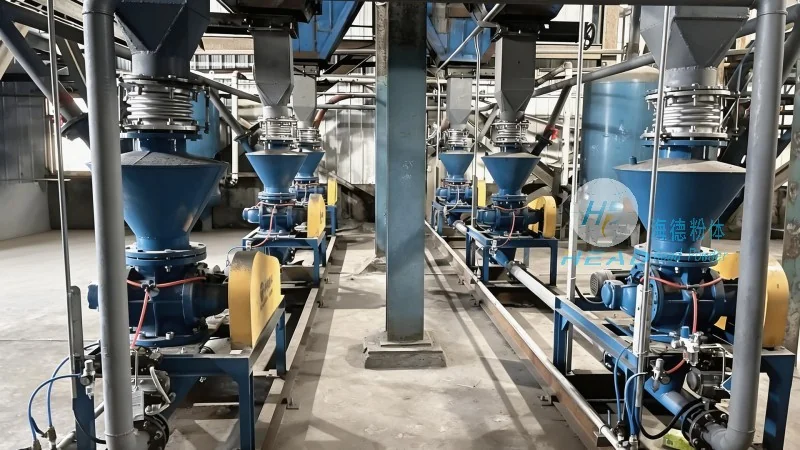
The core of the intelligent tonne bag loading station is the pneumatic conveying system, which utilizes air pressure to transport powders through a network of pipes. The system operates on the principle of creating a pressure differential between the material hopper and the conveying line. When the system is activated, a vacuum or pressure is applied to draw the powder from the tonne bag into the hopper. The powder is then propelled through the pipeline using compressed air or a combination of vacuum and pressure, depending on the system configuration. This method allows for the efficient and continuous movement of powders over long distances, with minimal product degradation.
Key Components and Their Functions
The intelligent tonne bag loading station comprises several critical components, each playing a vital role in the overall operation. These include:
- Tonne Bag Unloading Mechanism: This component is responsible for opening and emptying the tonne bag. It typically features a mechanical or pneumatic system that lifts the bag and positions it over the material hopper, ensuring a secure and controlled release of the powder.
- Material Hopper: The hopper serves as a temporary storage container for the powder, collecting it from the tonne bag before it is conveyed to the next stage. It is designed with a smooth interior to prevent material buildup and is equipped with a discharge valve to regulate the flow of powder into the conveying line.
- Pneumatic Conveying Line: The pipeline network transports the powder from the hopper to the destination, such as a silo, storage tank, or processing unit. The line is constructed from materials resistant to corrosion and abrasion, ensuring durability and long-term performance.
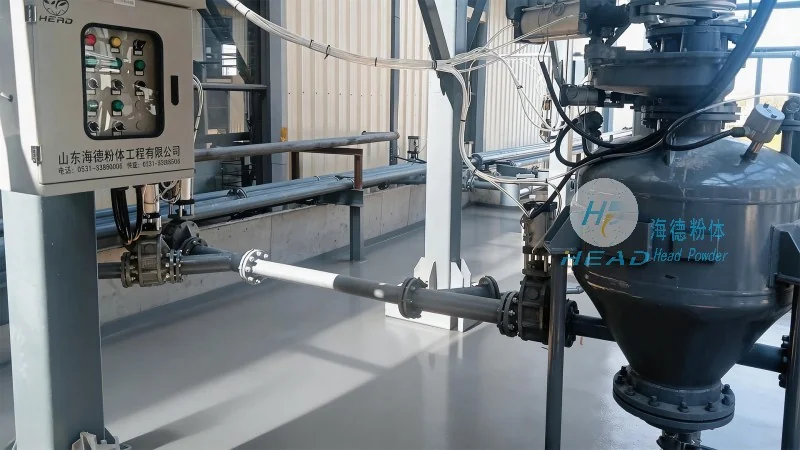
- Control System: An advanced control panel manages the entire operation, monitoring parameters such as pressure, flow rate, and material level. The system can be programmed to operate automatically, with sensors detecting the status of the tonne bag and the hopper, triggering the appropriate actions to maintain consistent performance.
Operation Process: Step-by-Step Guide
The operation of the intelligent tonne bag loading station follows a systematic sequence, ensuring efficient and reliable material transfer. The process begins with the placement of a tonne bag on the loading platform. The control system then initiates the unloading mechanism, which lifts the bag and positions it over the hopper. As the bag is emptied, the powder flows into the hopper, and the system monitors the material level. Once the hopper is filled to the desired capacity, the control system activates the pneumatic conveying system, which draws the powder from the hopper and transports it through the pipeline to the target location. The process continues until the tonne bag is completely emptied, after which the system can be prepared for the next bag or transition to a different operation mode.
Advantages and Applications
The intelligent tonne bag loading station offers several advantages that make it an ideal solution for industries requiring high-volume powder handling. These include:
- Automation and Efficiency: The system reduces labor costs and increases production throughput by automating the entire loading process, minimizing downtime and maximizing operational efficiency.
- Precision and Control: Advanced sensors and control systems ensure precise material measurement and consistent flow rates, reducing the risk of overfilling or underfilling.
- Safety and Hygiene: The enclosed design and automated operation minimize human exposure to powders, enhancing workplace safety and maintaining product purity.
- Flexibility: The system can be configured to handle various types of powders and tonne bag sizes, making it adaptable to different industrial applications.
Shandong HeadPowder Engineering Co., Ltd. has been at the forefront of developing innovative powder handling solutions, and the intelligent tonne bag loading station exemplifies their commitment to quality and technological advancement. By integrating state-of-the-art components and a user-friendly control system, this equipment provides industries with a reliable and efficient method for handling bulk powders, ensuring smooth operations and consistent product quality.