Multi-hopper pneumatic powder handling equipment, commonly known as multi-hopper pumps, is a specialized system designed for the efficient and reliable transportation of bulk powders over long distances. This equipment is widely used in various industrial sectors, including chemical, food, pharmaceutical, and cement industries, where the safe and effective movement of powders is critical to operational efficiency. The system combines advanced pneumatic technology with a multi-hopper design to provide a flexible and powerful solution for powder handling challenges.
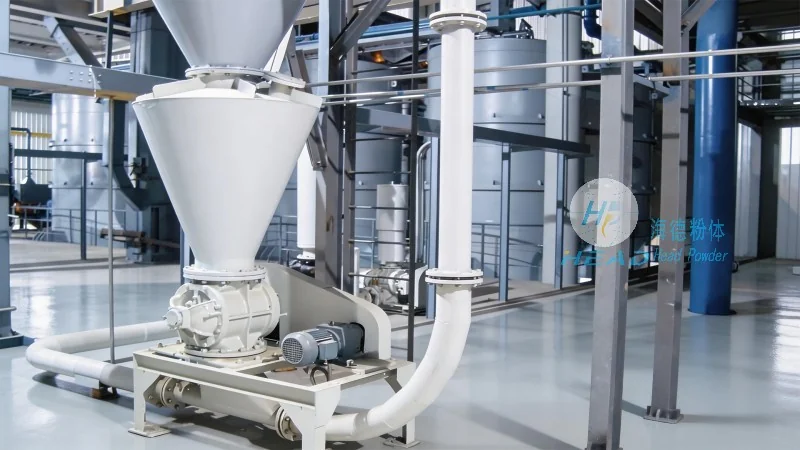
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design, development, and production of high-quality pneumatic powder handling equipment. With years of experience in the industry, the company has established itself as a trusted partner for businesses seeking reliable solutions for their bulk material handling needs. HeadPowder's commitment to innovation and quality ensures that their products meet the stringent requirements of modern industrial applications.
Principle of Operation
The core principle of multi-hopper pneumatic powder handling equipment is the use of compressed air to create a pressure differential that propels the powder through a pipeline. The system typically consists of multiple hoppers, each containing a different material or a portion of the same material. As the material is discharged from one hopper, it is replaced by the material from the next hopper, creating a continuous flow. The compressed air is introduced into the system through a venturi or a similar device, which draws the powder into the air stream and transports it to the destination. This process allows for the simultaneous handling of multiple materials or the sequential handling of a single material, depending on the configuration of the system.
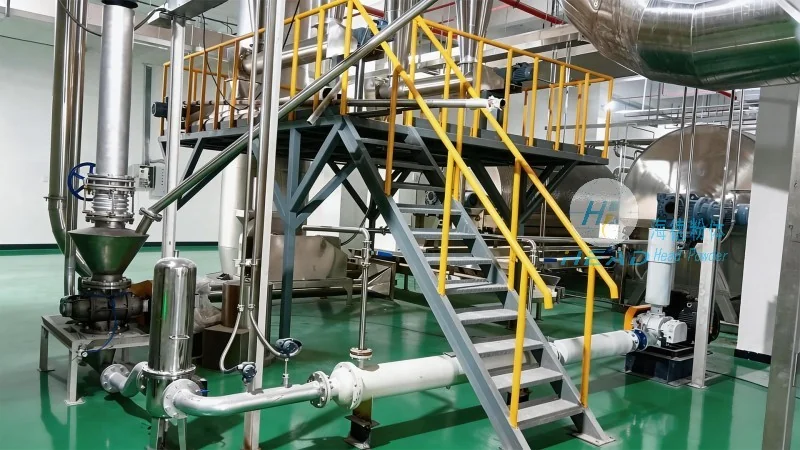
Key Components and Their Functions
The multi-hopper pneumatic system includes several key components that work together to ensure smooth operation. The main components are the hoppers, the air compressor, the control valves, the pipeline, and the discharge equipment. The hoppers are designed to hold the powder and provide a controlled discharge mechanism. The air compressor generates the necessary compressed air to create the pressure differential. The control valves regulate the flow of air and powder, ensuring that the system operates at optimal pressure and flow rates. The pipeline transports the powder and air mixture from the source to the destination. The discharge equipment, such as a rotary valve or a venturi, controls the release of the powder at the end of the pipeline.
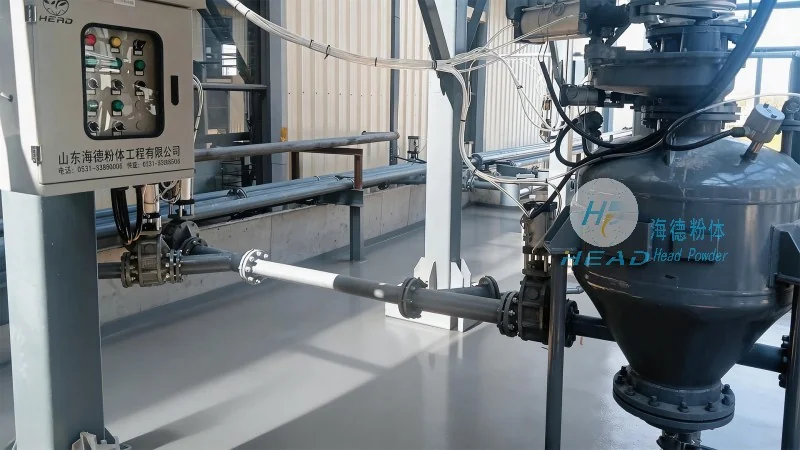
Working Scene Characteristics
The working scene characteristics of multi-hopper pneumatic powder handling equipment vary depending on the specific application and the industry. In general, the system is designed to handle a wide range of powder types, including fine powders, granules, and bulk materials. The equipment is suitable for both short and long-distance transportation, with the ability to handle distances up to several kilometers. The system is also capable of handling high volumes of material, making it ideal for large-scale industrial operations. Additionally, the multi-hopper design allows for the simultaneous handling of multiple materials, which is particularly useful in applications where different powders need to be mixed or processed together.
Advantages and Applications
Multi-hopper pneumatic powder handling equipment offers several advantages over traditional handling methods. The system is highly efficient, as it eliminates the need for manual handling and reduces the risk of material contamination. The equipment is also flexible, as it can be configured to handle different materials and distances. The system is also reliable, as it is designed to operate continuously without interruption. The applications of this equipment are diverse, including the transportation of chemicals, food products, pharmaceuticals, and cement. The system is also used in the production of powders for various industries, such as cosmetics, plastics, and ceramics.




