HeadPowder, a leading provider in the field of powder handling technology, introduces its advanced Automatic Tonne Bag Feeding Powder Material Conveying System. This system is designed to efficiently handle large volumes of bulk powders from tonne bags, ensuring seamless and reliable material transfer in industrial applications. The system integrates state-of-the-art components and intelligent control mechanisms to optimize the feeding and conveying process, meeting the stringent requirements of modern manufacturing and processing industries.
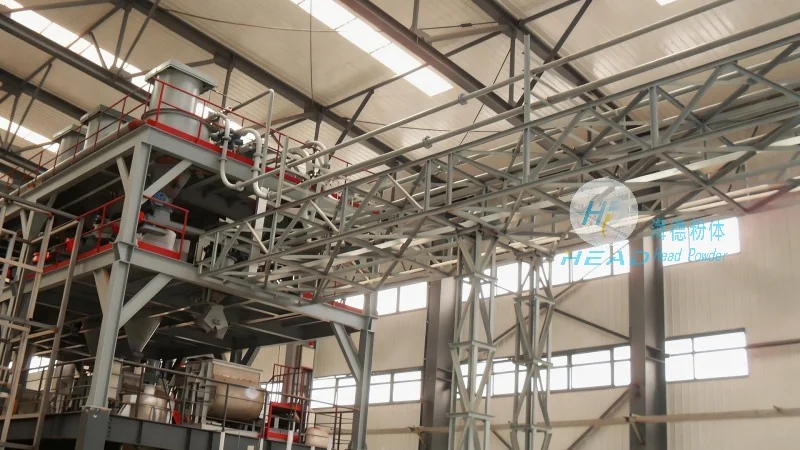
Key Components and Functional Overview
The Automatic Tonne Bag Feeding Powder Material Conveying System comprises several core components that work in harmony to achieve efficient material handling. The primary components include the tonne bag opening mechanism, the hopper and feeding hopper, the conveyor system (such as screw conveyors or pneumatic conveying lines), and the control panel with automated sensors. Each component is engineered to handle the specific challenges of bulk powder handling, such as preventing material bridging, ensuring consistent flow rates, and maintaining product integrity. The system is built with durability and ease of maintenance in mind, using high-quality materials and robust construction to withstand the rigors of continuous operation.
Operation Process of the System
The operation of the Automatic Tonne Bag Feeding Powder Material Conveying System follows a systematic sequence to ensure smooth material transfer. The process begins with the positioning of a tonne bag onto the system's loading platform. The bag is then secured and the opening mechanism activates, typically using a hydraulic or mechanical cutter to open the top of the bag. Once the bag is opened, the powder inside is discharged into the feeding hopper. The feeding hopper, equipped with a rotary valve or gate, regulates the flow of powder into the conveyor system. The conveyor then transports the powder to the desired destination, such as a storage silo, processing equipment, or packaging line. Throughout the process, sensors monitor the flow rate, level, and any potential blockages, providing real-time feedback to the control system. The system can be programmed to operate in automatic mode, where it cycles through the steps without manual intervention, or in manual mode for adjustments and maintenance. This flexibility ensures adaptability to various production schedules and operational needs.
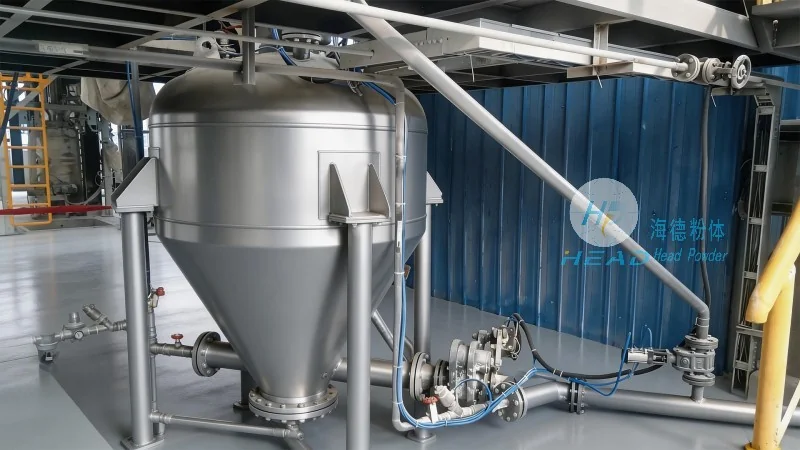
Working Principle of the System
The working principle of the Automatic Tonne Bag Feeding Powder Material Conveying System is based on the principles of mechanical and pneumatic conveying, combined with automated control technology. The system utilizes a combination of gravity and mechanical force to move the powder from the tonne bag to the conveyor. The opening mechanism ensures that the powder is released uniformly, preventing clumping or bridging that could lead to operational issues. The feeding hopper acts as a buffer, maintaining a consistent flow rate to the conveyor, which is crucial for preventing overloading and maintaining product quality. The conveyor system, whether screw or pneumatic, transports the powder through a sealed pipeline, minimizing dust emissions and ensuring a clean working environment. The control panel integrates sensors and actuators to monitor and control the entire process. For example, level sensors in the hopper detect when the material is low and trigger the opening of a new tonne bag or the start of the next cycle. Flow sensors measure the rate of material transfer, allowing the system to adjust the speed of the conveyor or the opening of the hopper to maintain optimal performance. The system's automation ensures that all steps are executed in a coordinated manner, reducing human error and increasing operational efficiency.
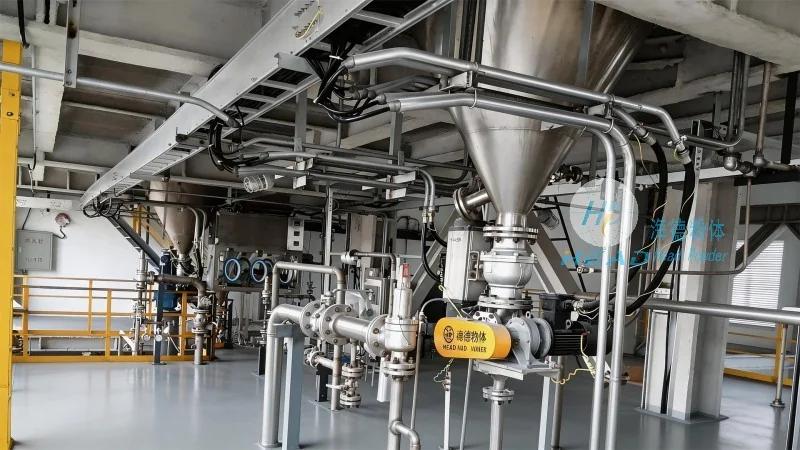
Benefits and Applications
The Automatic Tonne Bag Feeding Powder Material Conveying System offers numerous benefits to industrial operations, including increased productivity, reduced labor costs, and improved product quality. By automating the process of handling bulk powders from tonne bags, the system minimizes the need for manual labor, which can be hazardous and time-consuming. The automated feeding and conveying reduce the risk of material spillage and contamination, ensuring that the powder remains in a clean and controlled environment. The system's ability to handle large volumes of material efficiently makes it suitable for a wide range of applications, including chemical processing, food and beverage manufacturing, pharmaceutical production, and mining operations. The system's flexibility allows it to be integrated into existing production lines, enhancing overall operational efficiency and reducing downtime. Additionally, the system's durability and low maintenance requirements contribute to long-term cost savings, making it a reliable investment for industrial facilities.
Conclusion
HeadPowder's Automatic Tonne Bag Feeding Powder Material Conveying System represents a significant advancement in bulk powder handling technology. By combining advanced components, intelligent control, and automated processes, the system provides a reliable and efficient solution for industrial applications. The system's ability to handle large volumes of material from tonne bags, while maintaining product integrity and operational safety, makes it an essential asset for modern manufacturing and processing facilities. With its robust construction, flexible operation modes, and comprehensive monitoring capabilities, the system ensures optimal performance and contributes to the overall success of industrial operations. HeadPowder continues to innovate in the field of powder handling, providing solutions that meet the evolving needs of the industry.




