White flour pneumatic conveying systems are sophisticated industrial equipment designed to transport white flour and other fine powders efficiently and reliably. As a core component in the flour processing industry, these systems ensure the seamless movement of flour from storage silos to processing lines, maintaining product quality and operational efficiency. The system’s design and functionality are tailored to handle the unique characteristics of white flour, such as its fine particle size and hygroscopic nature, which require specialized handling to prevent caking, segregation, or contamination.
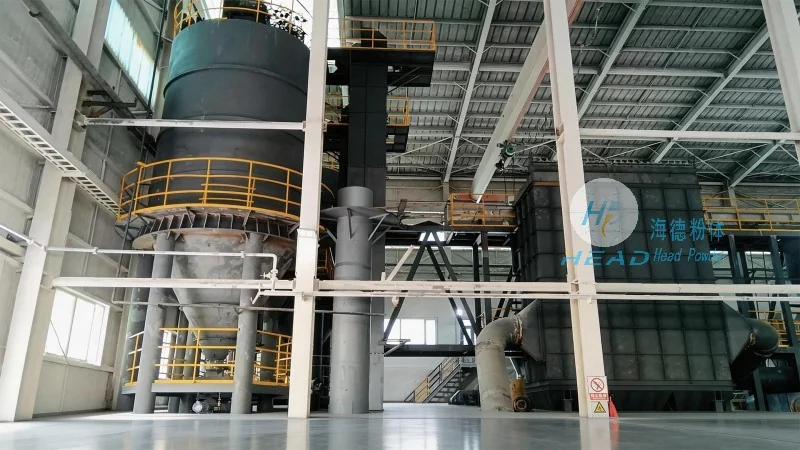
Key Components of the Pneumatic Conveying System
The white flour pneumatic conveying system from Shandong HeadPowder Engineering Co., Ltd. comprises several critical components that work in harmony to achieve effective material transport. These include a dust collector, a hopper for material storage, a rotary valve for controlled discharge, a pipeline network, and a fan or blower to generate the necessary air pressure. Each component is engineered to meet the specific demands of white flour, ensuring optimal performance and minimal downtime. The system’s modular design allows for easy integration into existing production lines and flexible customization based on client requirements.
Operation Process of the Pneumatic Conveying System
The operation of the white flour pneumatic conveying system follows a systematic process that begins with material loading into the hopper. The rotary valve regulates the flow of white flour from the hopper into the conveying pipeline, while the fan or blower creates a negative pressure or positive pressure environment within the system. As the air flows through the pipeline, it carries the white flour particles, transporting them from the source to the destination. The system’s control panel allows operators to monitor and adjust parameters such as air pressure, flow rate, and material feed rate in real-time, ensuring precise control over the conveying process. This dynamic control capability is essential for maintaining consistent product quality and preventing issues like blockages or overloading.
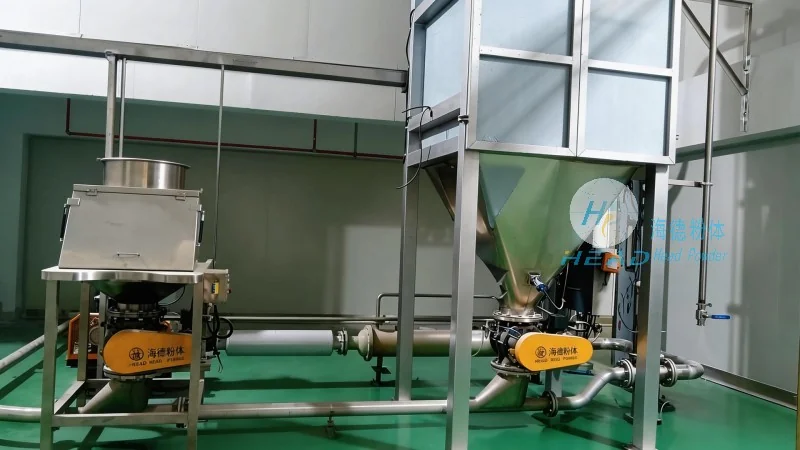
Working Principle of the Pneumatic Conveying System
The working principle of the white flour pneumatic conveying system is based on the fundamental physics of fluid dynamics and particle transport. The system utilizes either a negative pressure (suction) or positive pressure (blowing) method to move white flour through the pipeline. In the negative pressure mode, the fan creates a vacuum that draws white flour from the hopper into the pipeline, while the air flow carries the particles to the receiving hopper. In the positive pressure mode, the fan pushes air and white flour particles through the pipeline, delivering them to the target location. The system’s design minimizes the risk of product degradation by maintaining low temperatures and preventing direct contact with air, which could lead to oxidation or moisture absorption. Additionally, the system incorporates features like cyclone separators and filters to remove any fine particles or dust from the air stream, ensuring a clean and efficient operation.
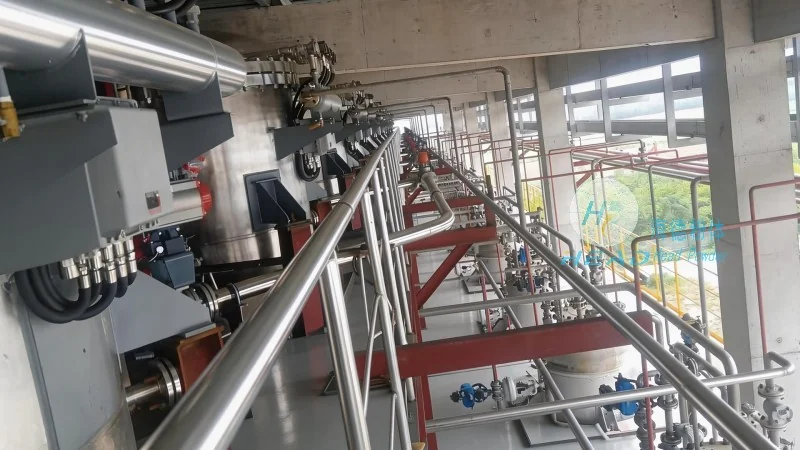
Advantages of Using White Flour Pneumatic Conveying Systems
Implementing a white flour pneumatic conveying system offers numerous advantages for flour processing facilities. These systems provide a dust-free and hygienic method of material transport, which is crucial for maintaining food safety standards. Unlike traditional mechanical conveyors, pneumatic systems eliminate the need for moving parts in the conveying path, reducing maintenance requirements and increasing operational reliability. The system’s ability to handle fine powders without segregation or caking ensures consistent product quality, which is vital for downstream processes such as milling or packaging. Furthermore, the flexible design of the system allows for easy expansion or reconfiguration as production needs change, providing long-term value and adaptability.
Applications and Industries Served
White flour pneumatic conveying systems are widely used in various industries that rely on the efficient handling of fine powders. The primary application is in the flour milling industry, where these systems transport white flour from storage silos to processing lines, packaging machines, or distribution centers. Additionally, the system is utilized in the food processing industry for handling other fine powders like sugar, starch, and spices. The system’s versatility also makes it suitable for pharmaceutical and chemical industries, where precise and hygienic material transport is essential. Shandong HeadPowder Engineering Co., Ltd. has successfully implemented these systems in facilities across China, providing reliable solutions for clients in the food and chemical sectors.




