Cereal powder conveying systems are critical components in the food processing industry, particularly for the efficient handling and transportation of cereal-based products. These systems are designed to ensure the safe, reliable, and efficient movement of powders such as oats, wheat, corn, and other grains from storage to processing or packaging stages. The technology behind these systems combines mechanical engineering principles with material handling expertise to address the unique challenges posed by cereal powders, including their fine particle size, flow characteristics, and potential for dust generation.
Principles of Cereal Powder Conveying Systems
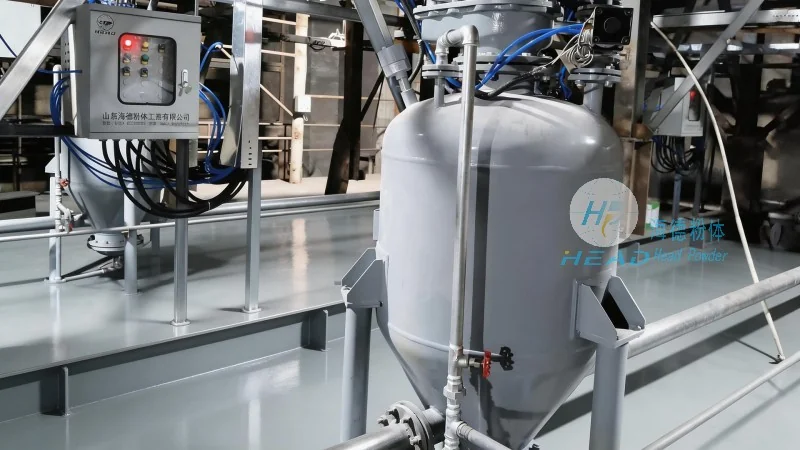
The core principles of cereal powder conveying systems revolve around the use of various mechanical and pneumatic technologies to move bulk materials. Common methods include screw conveyors, pneumatic conveying systems, and bucket elevators. Each method operates based on different physical forces, such as gravity, pressure differentials, or mechanical displacement. For instance, screw conveyors utilize rotating screws to push powders forward, while pneumatic systems use air pressure to transport materials through pipelines. The choice of system depends on factors like the material's properties, the required conveying distance, and the desired speed of operation.
Working Scene Characteristics of Cereal Powder Conveying Systems
Cereal powder conveying systems are employed in diverse industrial settings, each with distinct operational characteristics. In large-scale cereal processing plants, these systems are integral to the production line, ensuring seamless integration between raw material storage, processing, and packaging. The working environment often involves high volumes of material, requiring robust and durable equipment capable of withstanding continuous operation and potential contamination. Additionally, the systems must comply with food safety regulations, which necessitates features like easy cleaning, minimal particle loss, and the prevention of cross-contamination. In smaller-scale operations, such as artisanal cereal producers, the systems may be more compact and flexible, designed to handle smaller batches while maintaining efficiency and precision.
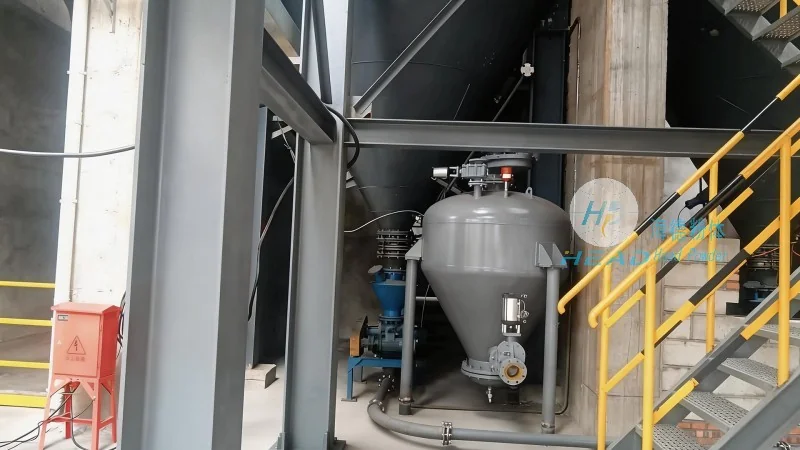
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. is a leading provider of specialized engineering solutions for the food processing industry, with a focus on powder handling and conveying systems. Based in Shandong, China, the company has established itself as a trusted partner for businesses seeking reliable and efficient solutions for their cereal powder processing needs. HeadPowder Engineering leverages advanced technology and extensive industry experience to design, manufacture, and install conveying systems tailored to the specific requirements of each client. The company's commitment to quality, safety, and innovation has earned it a reputation for delivering products that meet or exceed industry standards.
Key Features and Benefits of Cereal Powder Conveying Systems
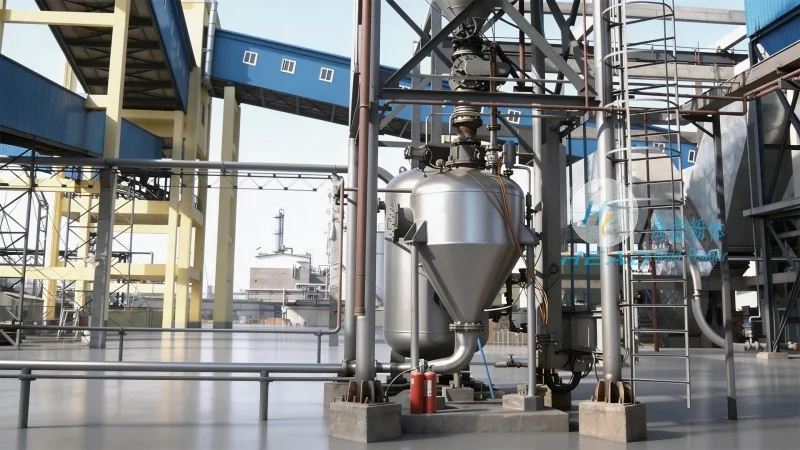
Modern cereal powder conveying systems offer several key features that enhance performance and operational efficiency. These include variable speed control, which allows for adjustments based on material flow rates and processing demands. Additionally, many systems incorporate dust suppression and filtration technologies to minimize environmental impact and ensure worker safety. The use of corrosion-resistant materials and easy-to-clean designs further contributes to the longevity and hygiene of the equipment. For businesses in the cereal industry, these features translate into reduced downtime, lower maintenance costs, and improved overall productivity. By investing in advanced conveying systems, companies can optimize their production processes and maintain a competitive edge in the market.
Application Examples and Operational Scenarios
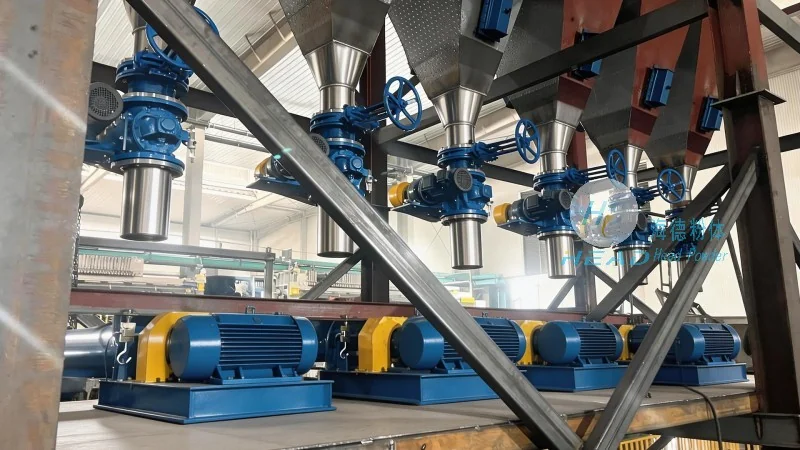
The versatility of cereal powder conveying systems is evident in their application across various operational scenarios. In large-scale cereal mills, these systems are used to transport raw grains from silos to grinding equipment, ensuring a consistent supply of material for flour production. In breakfast cereal manufacturing plants, the systems handle the movement of pre-processed powders from mixing tanks to packaging lines, where they are combined with other ingredients and sealed into final products. Additionally, in the production of specialty cereals, such as organic or gluten-free varieties, the systems must be capable of handling specific material properties while maintaining strict quality control standards. The adaptability of these systems makes them suitable for both traditional and emerging applications within the cereal industry.
Conclusion: The Importance of Reliable Cereal Powder Conveying Systems
In conclusion, cereal powder conveying systems play a vital role in the efficient and safe processing of cereal products. By understanding the principles and operational characteristics of these systems, businesses can make informed decisions about their material handling infrastructure. The integration of advanced technology and robust engineering ensures that these systems can meet the demands of modern cereal production, from large-scale industrial operations to smaller, specialized facilities. As the cereal industry continues to evolve, the importance of reliable conveying systems will only grow, making them an essential component for any business looking to maintain productivity and quality in their operations. With the expertise and commitment of companies like Shandong HeadPowder Engineering, businesses can access the solutions needed to optimize their processes and achieve their production goals.




