Principle and Working Scene Characteristics of Sub-Zinc Oxide Powder Conveying System
Release time:2026-09-19 03:01:31
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Zhang manager
Headpowder, a leading provider in the field of powder handling technology, specializes in the design and manufacturing of advanced conveying systems for various industrial applications. With a strong presence in Shandong, China, the company has established itself as a trusted partner for businesses requiring efficient and reliable powder transport solutions. This article delves into the core principles and operational characteristics of their sub-zinc oxide powder conveying system, highlighting its design, functionality, and practical applications.
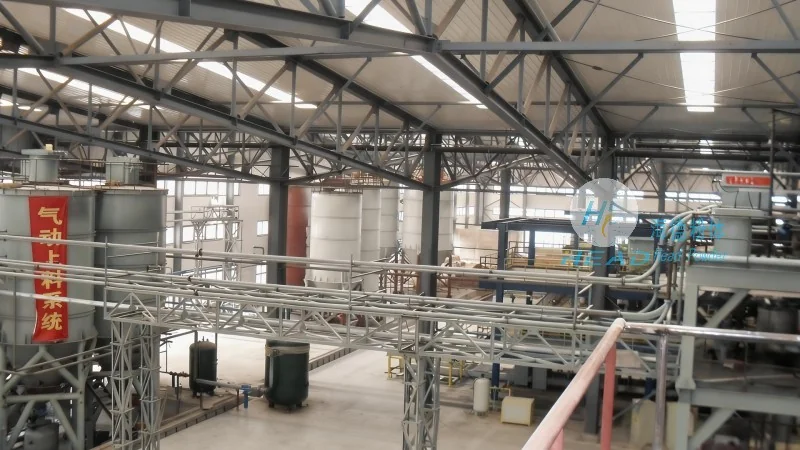
Principle of the Sub-Zinc Oxide Powder Conveying System
The sub-zinc oxide powder conveying system operates on a sophisticated mechanism that ensures the seamless transport of fine powders like sub-zinc oxide. At its core, the system combines elements of pneumatic and mechanical conveying technologies to achieve optimal performance. The process begins with the feeding of the powder into the system, where it is then drawn into the conveying line by a vacuum or pressure differential. This method effectively prevents dust accumulation and maintains a clean working environment, which is crucial for handling sensitive materials such as sub-zinc oxide. The system utilizes high-efficiency filters and air treatment units to ensure that the air used in the conveying process is clean and free from contaminants, thereby protecting both the material and the equipment from degradation or damage.
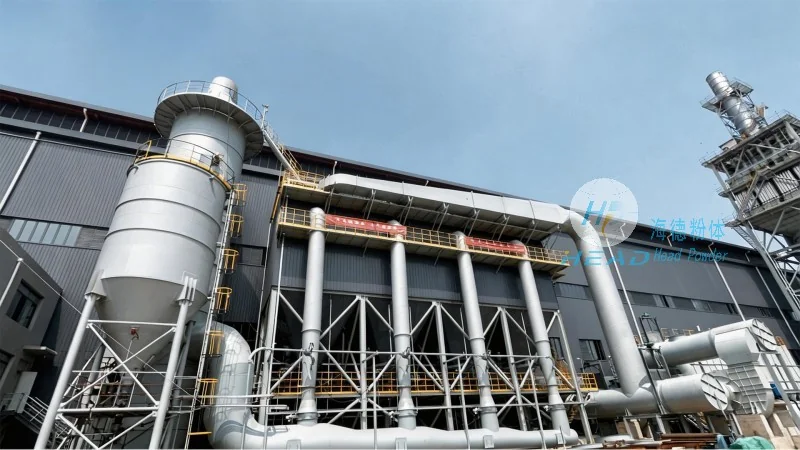
Working Scene Characteristics and Practical Applications
The sub-zinc oxide powder conveying system is designed to adapt to diverse industrial environments, making it suitable for a wide range of applications. Its flexibility allows it to be integrated into existing production lines or used as a standalone solution for material transport. In manufacturing settings, the system excels in handling sub-zinc oxide in processes such as coating, compounding, and blending. The system's ability to maintain consistent material flow and minimize downtime is particularly valuable in high-volume production environments. Additionally, the system's compact design and modular components enable easy installation and maintenance, reducing operational costs and increasing overall efficiency. Whether used in research and development labs or large-scale industrial plants, the system provides reliable performance under varying conditions, ensuring that the material is conveyed safely and efficiently.
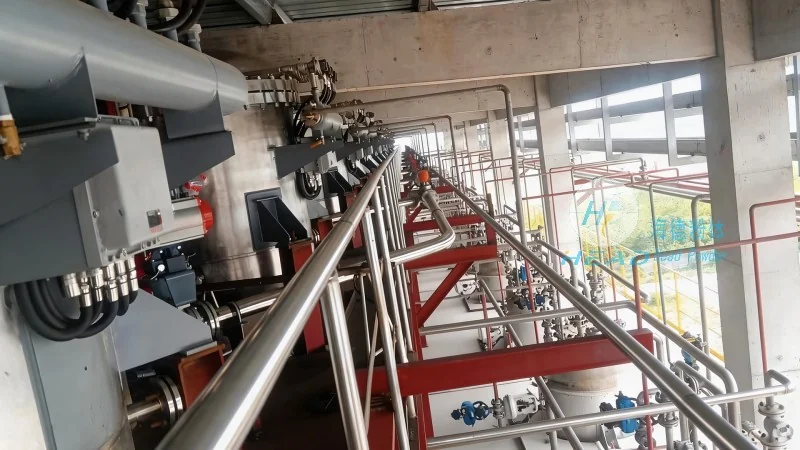
Key Advantages and Operational Benefits
One of the primary advantages of the sub-zinc oxide powder conveying system is its ability to handle fine powders without clogging or blockages. The system's design incorporates features such as self-cleaning filters and adjustable flow rates, which help maintain consistent performance over time. This reliability is essential for industries where material quality and consistency are critical, such as pharmaceuticals, food processing, and chemical manufacturing. Furthermore, the system's energy efficiency contributes to lower operational costs, making it a cost-effective solution for businesses looking to optimize their production processes. The user-friendly control panel and intuitive interface allow operators to easily monitor and adjust the system's parameters, enhancing operational flexibility and reducing the need for specialized training.




