HeadPowder, a leading engineering company based in Shandong, China, specializes in the design, manufacturing, and installation of efficient aggregate material conveying systems. These systems are crucial for the smooth operation of construction and mining projects, ensuring the reliable transport of raw materials like gravel, sand, and crushed stone from one location to another. The company's expertise lies in developing customized solutions that meet the specific requirements of various industrial applications, enhancing productivity and operational efficiency.
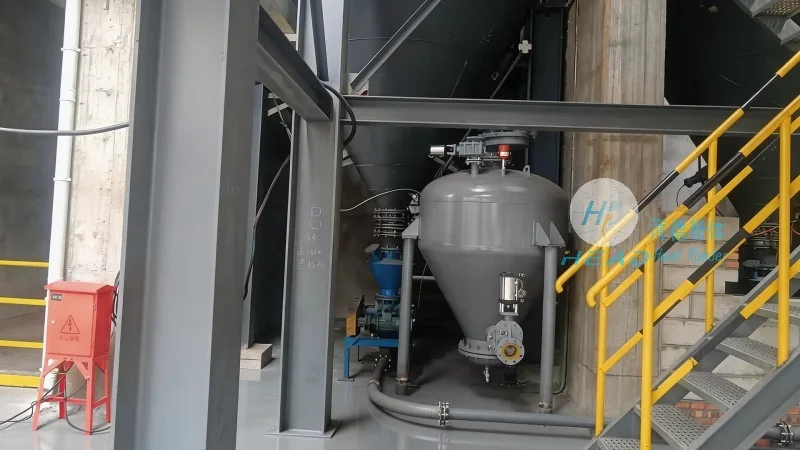
Working Principle of Aggregate Material Conveying Lines
The core of an aggregate material conveying line is a series of interconnected components that work in tandem to transport bulk materials. The process typically begins with the loading of raw materials into a hopper or feeder, which regulates the flow of material into the conveyor system. From there, the material is transferred through various types of conveyors, such as belt conveyors, screw conveyors, or pneumatic conveyors, depending on the material characteristics and distance to be covered. Belt conveyors, for instance, are widely used due to their high load capacity and ability to handle a wide range of materials, including wet or sticky aggregates. Screw conveyors are ideal for vertical or inclined transport, while pneumatic systems are suitable for fine powders or dusty materials. The conveying line may also include components like elevators, transfer points, and control systems to ensure seamless material flow and prevent blockages. Each component is carefully designed and integrated to maintain consistent speed and pressure, minimizing material degradation and energy consumption.
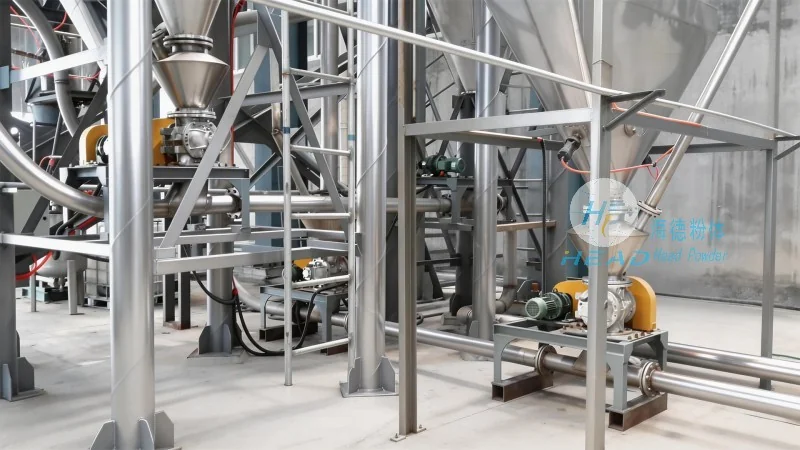
Key Features of Aggregate Material Conveying Lines
HeadPowder's aggregate material conveying lines are distinguished by several key features that enhance their performance and reliability. Firstly, the systems are built with high-quality materials and robust construction, ensuring durability and long service life even under heavy operational loads. This includes the use of corrosion-resistant components for environments with moisture or chemicals, and wear-resistant parts for abrasive materials like crushed stone. Secondly, the conveyors are equipped with advanced control systems that allow for precise regulation of speed, flow rate, and direction. These systems can be integrated with sensors and automation technologies to monitor performance in real-time, detect anomalies, and trigger corrective actions automatically. Thirdly, the design prioritizes safety and maintenance accessibility. Features such as emergency stop buttons, protective guards, and easy-to-reach maintenance points reduce the risk of accidents and simplify routine upkeep. Additionally, the conveyors are designed to minimize energy consumption through efficient drive mechanisms and optimized material handling, contributing to cost savings and environmental sustainability. The modular nature of the systems also allows for easy expansion or modification as project needs evolve, providing flexibility for future growth.
Applications and Benefits in Industrial Settings
Aggregate material conveying lines are essential in a variety of industrial sectors, including construction, mining, and manufacturing. In construction, they are used to transport raw materials to job sites, ensuring a steady supply of aggregates for concrete production and other building materials. In mining operations, the systems facilitate the transport of crushed ore and rock from processing plants to storage or transportation facilities, improving operational efficiency and reducing labor costs. The benefits of these systems extend beyond just material transport; they also contribute to improved safety by eliminating the need for manual handling of heavy or hazardous materials. This reduces the risk of workplace injuries and improves overall workplace safety standards. Furthermore, the automation and control features of modern conveying lines enhance operational consistency, leading to higher quality output and reduced waste. The reliability of these systems also minimizes downtime, as they are designed to operate continuously with minimal maintenance interruptions. For companies like HeadPowder, these features translate into competitive advantages, enabling them to deliver high-quality products and services to their clients while maintaining cost-effectiveness and sustainability.
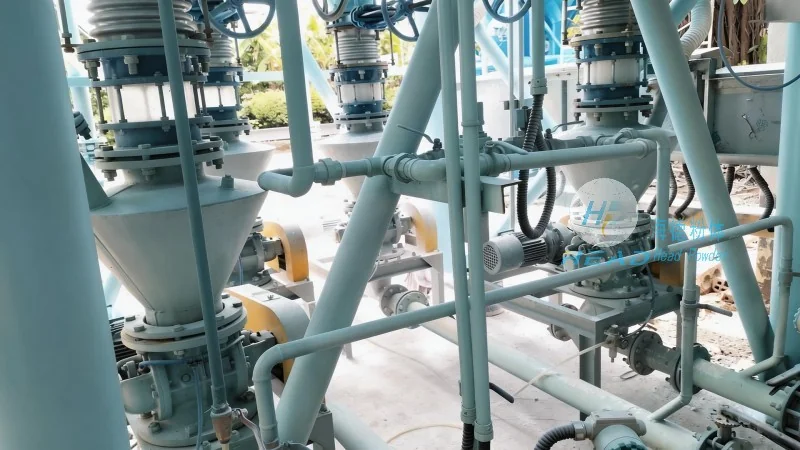
Customization and After-Sales Support
HeadPowder understands that each project has unique requirements, and therefore, offers customized aggregate material conveying solutions tailored to specific needs. The company works closely with clients to assess their operational challenges and material characteristics, then designs a system that optimizes performance and efficiency. This includes selecting the appropriate conveyor type, determining the optimal layout, and integrating necessary accessories like hoppers, chutes, and control panels. After the installation, HeadPowder provides comprehensive after-sales support, including training for operators, regular maintenance services, and technical assistance. The company's team of experienced engineers and technicians is available to address any issues promptly, ensuring that the conveying line operates at peak performance. This commitment to customer satisfaction and long-term partnership is a key differentiator for HeadPowder in the market.




