Stone coal material conveying systems are critical industrial equipment for efficiently transporting bulk materials, particularly stone coal. These systems are engineered to handle the abrasive and high-density properties of stone coal, ensuring reliable performance in demanding environments. Understanding the system's working principle and key features is essential for optimizing operational efficiency and extending equipment lifespan.
Introduction to Stone Coal Material Conveying Systems
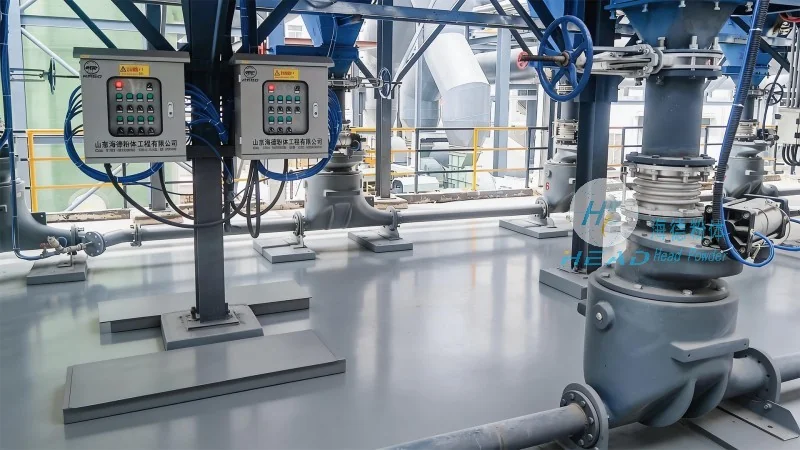
Stone coal, also known as coking coal or semi-coke, is a vital raw material in the steel and chemical industries. Its transportation requires specialized equipment capable of withstanding harsh conditions and maintaining material integrity. The stone coal material conveying system developed by Shandong HeadPowder Engineering Co., Ltd. addresses these challenges through advanced engineering and robust construction. This system is designed to handle the unique characteristics of stone coal, including its varying particle sizes and abrasive nature, making it suitable for diverse industrial applications.
Working Principle of the Stone Coal Material Conveying System
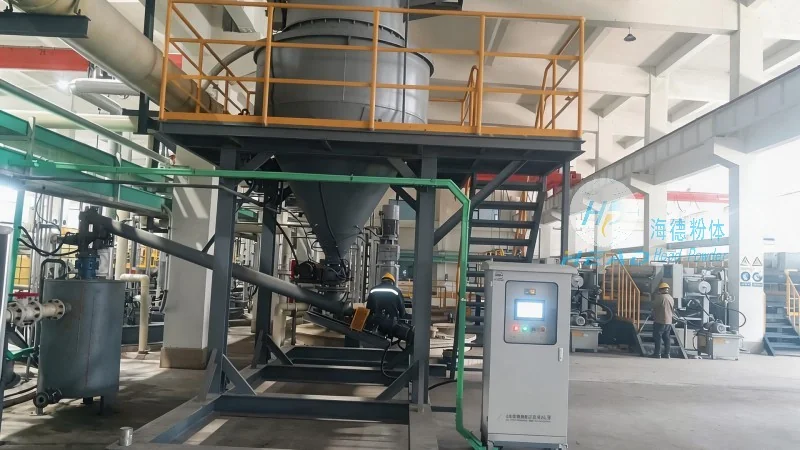
The core working principle of the stone coal material conveying system involves a combination of mechanical components to facilitate material movement. The system typically includes a hopper for material storage, a conveyor mechanism (such as a belt or screw) for transport, and a discharge outlet for delivering the material to its destination. The process begins with material being fed into the hopper, where it is then transferred to the conveyor system. An electric motor powers the conveyor, moving the material along the designated path at a controlled speed. The system maintains consistent pressure and flow to minimize material degradation and ensure efficient transportation. The discharge mechanism releases the material at the required location, completing the process. This integrated approach ensures smooth, continuous operation even under heavy load conditions.
Key Features of the Stone Coal Material Conveying System
The stone coal material conveying system by Shandong HeadPowder Engineering Co., Ltd. incorporates several key features that enhance performance and durability. One primary feature is the robust construction, utilizing high-quality materials resistant to abrasion and corrosion. This ensures the system withstands the harsh environment of stone coal processing without significant wear. Another critical feature is adjustable speed control, allowing operators to optimize conveyor speed based on material characteristics and processing needs. This flexibility helps maintain stone coal quality and reduce energy consumption. The system also includes safety mechanisms like overload protection and emergency stop buttons to prevent accidents and ensure safe operation. Additionally, the design prioritizes easy maintenance with accessible components, minimizing downtime. These features collectively contribute to high efficiency and long service life.
Company Profile: Shandong HeadPowder Engineering Co., Ltd.
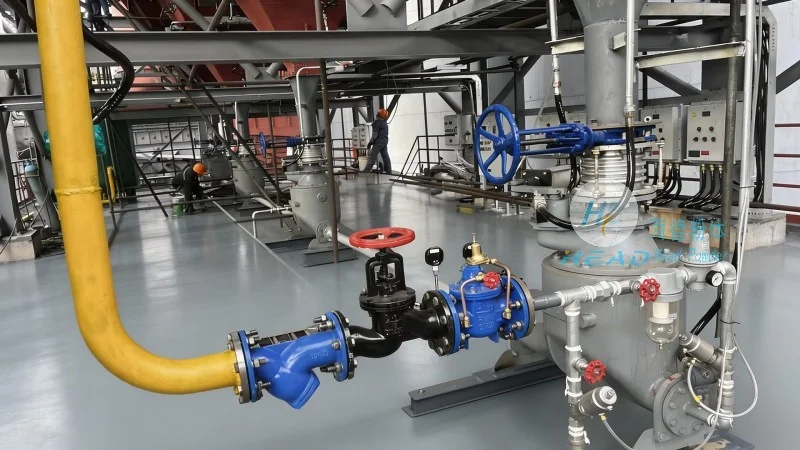
Shandong HeadPowder Engineering Co., Ltd. is a leading manufacturer of industrial conveying systems, with a strong global presence. The company specializes in designing, developing, and producing high-quality material handling equipment, including stone coal material conveying systems. HeadPowder employs experienced engineers and technicians dedicated to providing tailored solutions for clients. The company’s commitment to quality and customer satisfaction has established it as a reliable partner in the industry. HeadPowder’s facilities utilize advanced technology and stringent quality control measures, ensuring all products meet high standards. Comprehensive after-sales support—including installation, maintenance, and technical assistance—is provided to maximize equipment performance. With a focus on research and development, HeadPowder continuously improves its products to meet evolving market demands.
Conclusion
In summary, the stone coal material conveying system by Shandong HeadPowder Engineering Co., Ltd. is an advanced and reliable solution for efficient stone coal transportation. Its working principle, based on mechanical and hydraulic systems, ensures consistent and controlled material flow. The key features—such as robust construction, adjustable speed control, and safety mechanisms—enhance performance and durability. As a leading manufacturer, HeadPowder combines expertise and innovation to deliver high-quality equipment that meets diverse industrial needs. For industries processing stone coal, investing in such a system can significantly improve operational efficiency and reduce costs. The company’s commitment to quality and customer support further adds value, making it a preferred choice for clients worldwide.




