For sugar processing facilities, efficient and reliable powder conveying systems are crucial for maintaining production efficiency and product quality. The sugar powder conveying system equipment developed by Shandong HeadPowder Engineering Co., Ltd. is designed to meet the specific needs of the sugar industry, ensuring smooth and safe material transport. This article will explore the working principle and key features of this advanced conveying system.
Working Principle of the Sugar Powder Conveying System
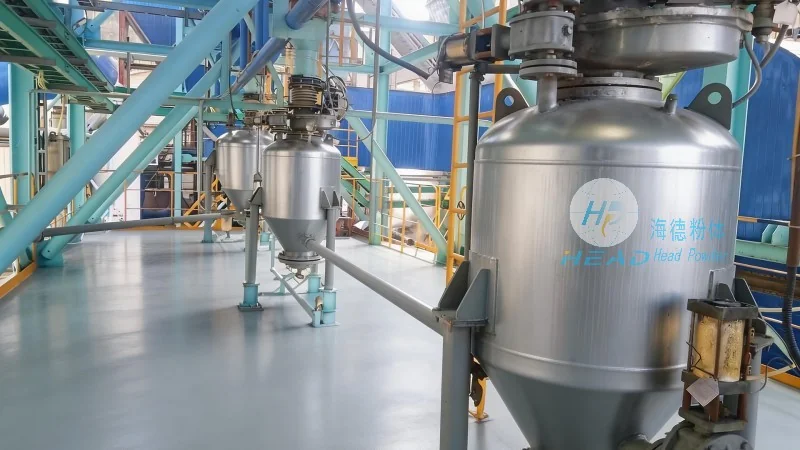
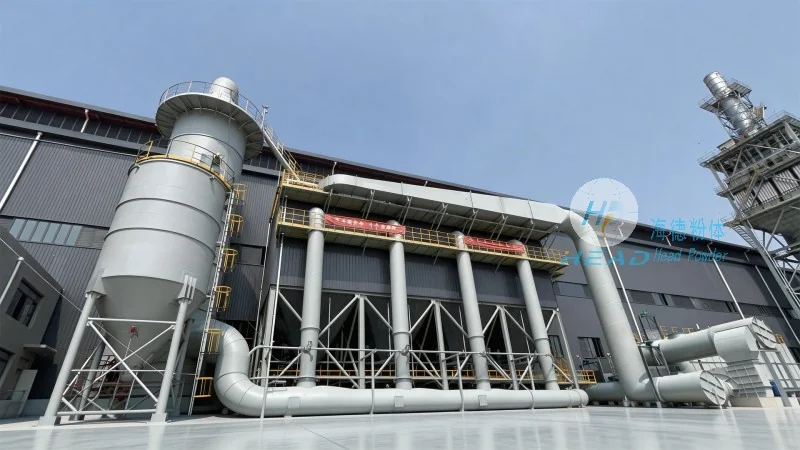
The sugar powder conveying system operates based on a combination of mechanical and pneumatic principles, tailored to handle the unique characteristics of sugar powders. The system typically consists of several core components, including a hopper for material storage, a feeder to control the flow rate, a conveying pipeline, and a discharge mechanism. The working process begins with the sugar powder being fed into the hopper from the storage silo. The feeder then regulates the amount of powder released into the conveying pipeline, ensuring a consistent flow. Within the pipeline, the powder is propelled by a combination of air pressure and mechanical agitation, moving the material from the inlet to the discharge point. This method, often referred to as pneumatic conveying, effectively minimizes product contamination and reduces the risk of blockages compared to traditional mechanical systems. The system is equipped with pressure sensors and flow monitors to maintain optimal operation, providing real-time feedback on the conveying status. Additionally, the design incorporates safety features such as overpressure relief valves and emergency shut-off mechanisms to prevent accidents and protect the equipment and personnel.
Key Features of the Sugar Powder Conveying System
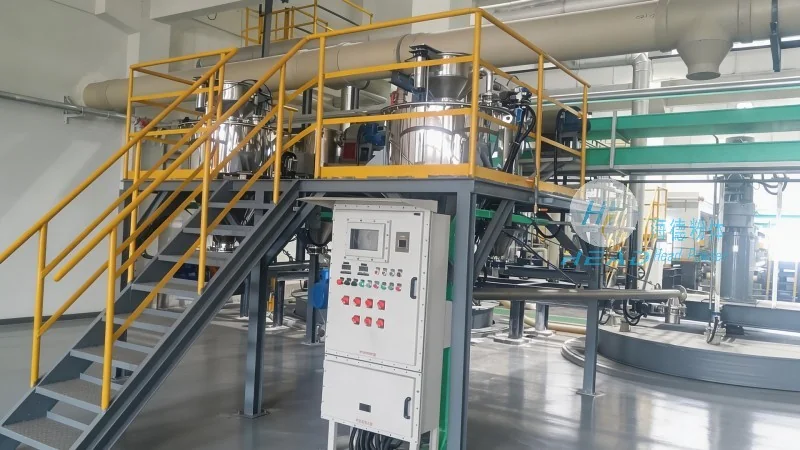
Shandong HeadPowder Engineering Co., Ltd.'s sugar powder conveying system is engineered with several distinctive features that enhance its performance and reliability. One of the primary features is the use of a flexible, corrosion-resistant pipeline material, which is essential for handling sugar powders that may contain moisture or acidic components. The pipeline is constructed from high-quality stainless steel or food-grade plastic, ensuring durability and compliance with industry standards. Another notable feature is the advanced control system, which allows for precise adjustment of the conveying speed and pressure. This system is integrated with a user-friendly interface, enabling operators to monitor and adjust the parameters easily. The conveying system also includes a cleaning mechanism to prevent powder buildup and maintain hygiene, which is critical in food processing environments. Furthermore, the design incorporates energy-efficient components, such as variable frequency drives, to optimize power consumption and reduce operational costs. The system's modular construction allows for easy installation and maintenance, with components that can be quickly replaced or serviced without disrupting the entire operation. These features collectively contribute to a conveying system that is not only efficient but also safe, hygienic, and cost-effective for sugar processing applications.
Application and Benefits in Sugar Industry
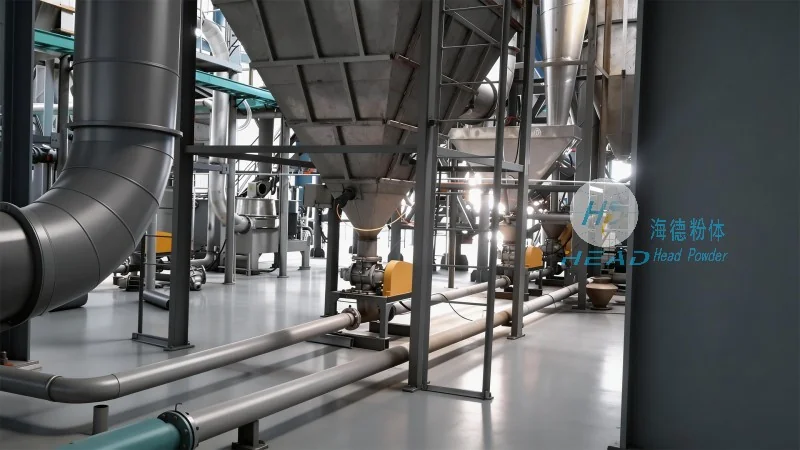
The sugar powder conveying system is widely used in various stages of the sugar production process, from raw material handling to final product packaging. In the raw material stage, the system efficiently transports sugar beets or cane juice concentrate into the processing plant, ensuring a steady supply of raw materials. During the refining process, the system conveys sugar crystals and other intermediate products between different processing units, such as crystallizers and centrifuges. In the final packaging stage, the system delivers finished sugar products to storage silos or packaging lines, maintaining product integrity and preventing contamination. The benefits of using this conveying system include improved production efficiency, reduced labor costs, and enhanced product quality. By minimizing material handling time and ensuring consistent flow rates, the system helps to increase overall production output. Additionally, the hygienic design of the system reduces the risk of product contamination, which is crucial for maintaining compliance with food safety regulations. The system's reliability also contributes to lower downtime and maintenance costs, as the advanced components and modular design minimize the need for frequent repairs. Overall, the sugar powder conveying system from Shandong HeadPowder Engineering Co., Ltd. provides a comprehensive solution for sugar processing facilities, addressing the unique challenges of powder handling in the industry.




