

What is a vacuum and pressure mixing material handling system equipment? What is its design principl
Efficient material handling is a cornerstone of modern industrial operations, and among the innovative solutions available, the vacuum and pressure mixing material handling system stands out for its versatility and effectiveness. This equipment, designed to transport and process bulk materials, combines the principles of both vacuum and pressure technologies to achieve seamless material movement. Understanding its functionality and design is crucial for industries seeking reliable and efficient material handling solutions.
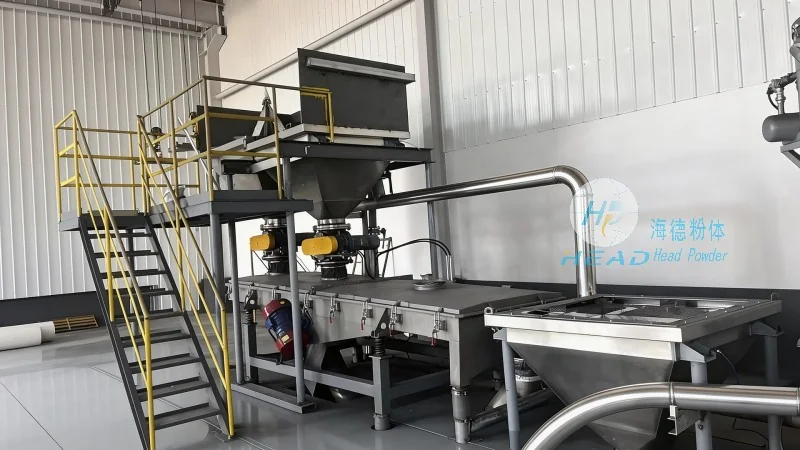
Overview of the Vacuum and Pressure Mixing Material Handling System
The vacuum and pressure mixing material handling system is a sophisticated piece of equipment engineered to handle a wide range of bulk materials, from powders and granules to small parts. Unlike traditional conveyor systems that rely solely on mechanical force, this system utilizes a combination of vacuum and pressure to create a controlled environment for material transport. The core components include a vacuum pump, pressure control valves, material containers, and a network of hoses or pipes that facilitate the movement of materials between different locations within a facility. This design allows for precise control over the flow rate and direction of material, ensuring minimal waste and optimal processing efficiency.
The Design Principle Behind the System
The design principle of the vacuum and pressure mixing material handling system is centered on the creation of a differential pressure between the material source and the destination. By applying a vacuum at the source, the system draws material into the collection container, while simultaneously using pressure at the discharge point to push the material out. This two-stage process ensures that materials are moved without the need for mechanical contact, reducing wear and tear on both the equipment and the materials being handled. The system also incorporates advanced sensors and control mechanisms to monitor pressure levels, flow rates, and material levels in real-time, allowing for automated adjustments and enhanced operational safety. The integration of these elements results in a highly efficient and reliable material handling solution that can adapt to various industrial applications.
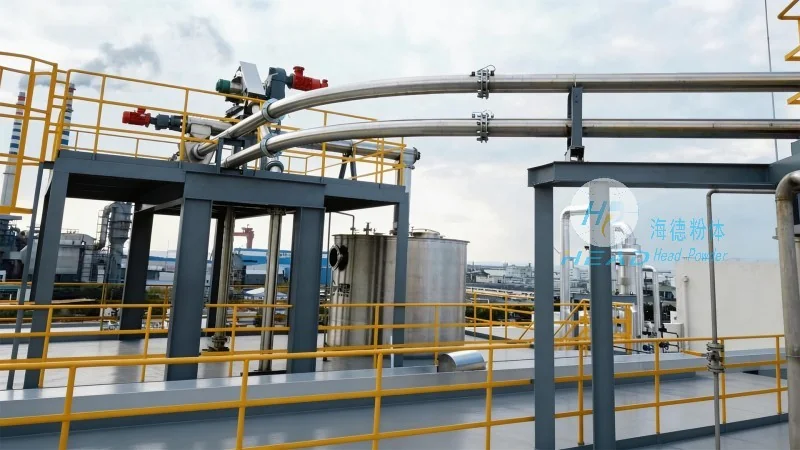
Key Features and Benefits
Several key features make the vacuum and pressure mixing material handling system a preferred choice for many industries. Firstly, its ability to handle a diverse range of materials, including those that are dusty, abrasive, or sensitive to contamination, makes it suitable for applications in pharmaceuticals, food processing, and chemical manufacturing. The system's compact design and modular components allow for easy installation and integration into existing production lines, minimizing downtime and installation costs. Additionally, the use of vacuum and pressure technology reduces energy consumption compared to traditional methods, contributing to lower operational costs and a smaller environmental footprint. The system also offers enhanced safety features, such as automatic shut-off in case of pressure or vacuum failure, and the ability to handle materials in a closed system, preventing dust emissions and cross-contamination.
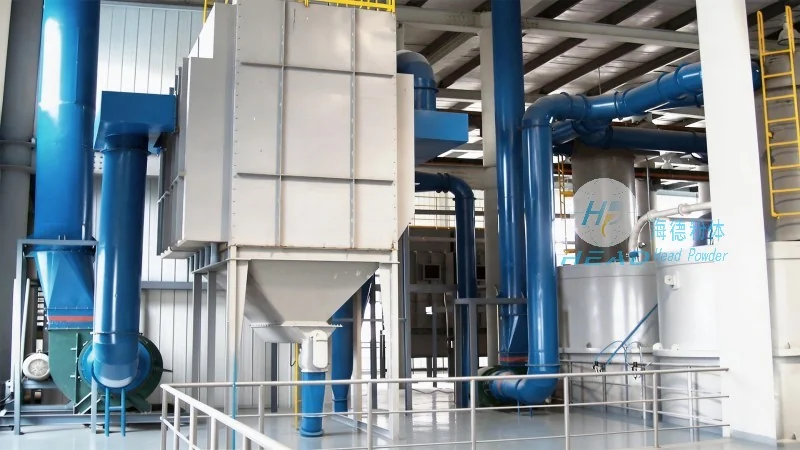
Applications in Industrial Settings
The vacuum and pressure mixing material handling system finds applications in various industrial sectors, including pharmaceuticals, food and beverage, chemical processing, and manufacturing. In pharmaceutical manufacturing, it is used to transport active ingredients and excipients with precision, ensuring that the final product meets stringent quality standards. In food processing, the system is employed to handle ingredients like flour, sugar, and spices, maintaining hygiene and preventing contamination. In chemical processing, it is used to transport powders and granules that are sensitive to moisture or air, ensuring that the chemical reactions proceed as intended. The system's adaptability and efficiency make it a valuable asset in any facility that requires reliable and efficient material handling.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of material handling systems based in China. With a strong commitment to innovation and quality, the company has developed a range of advanced solutions, including the vacuum and pressure mixing material handling system. HeadPowder's products are designed to meet the specific needs of various industries, offering high performance, durability, and reliability. The company's team of experts provides comprehensive support, from product design and customization to installation and maintenance, ensuring that clients receive the best possible service and support. HeadPowder's dedication to customer satisfaction and technological advancement has made it a trusted partner for businesses seeking efficient and effective material handling solutions.