Coal powder pneumatic conveying equipment is a critical component in industrial processes that require the efficient and safe transportation of fine coal powders. This technology utilizes air as the primary medium to move coal particles from one location to another, offering advantages such as reduced material handling costs, improved safety compared to traditional bulk handling methods, and enhanced process control. The fundamental principle behind this equipment involves creating a pressure differential or using suction to transport coal powder through a pipeline system. By understanding the core mechanisms and operational dynamics, industries can optimize their material handling strategies and improve overall operational efficiency.
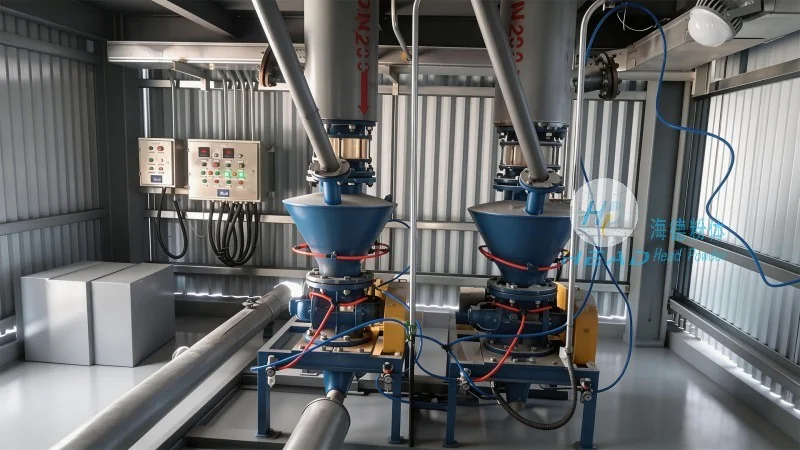
Key Components and Working Principle
The operation of coal powder pneumatic conveying systems relies on several key components, each playing a vital role in the overall process. The main components include a feeding system, a conveying line, a separation or collection system, and a control unit. The feeding system is responsible for introducing the coal powder into the conveying line, typically using a hopper or a rotary valve to ensure a consistent flow. The conveying line, often made of metal or plastic, transports the coal particles along with the air stream. The separation system, such as a cyclone or a filter, separates the coal powder from the air at the end of the line, allowing the powder to be collected and the air to be discharged or recycled. The control unit monitors and adjusts the system parameters, such as air pressure, flow rate, and material feed rate, to maintain optimal performance. The working principle is based on the principle of fluidization and suspension, where the coal particles are kept in a suspended state by the air flow, preventing them from settling or clogging the pipeline. This suspension allows for smooth and continuous transportation of the powder over long distances.
Advantages of Pneumatic Conveying for Coal Powder
Compared to traditional mechanical conveying methods like belt conveyors or bucket elevators, coal powder pneumatic conveying offers several distinct advantages. One of the primary benefits is the ability to handle fine and abrasive powders without causing excessive wear on the equipment. The air flow helps to reduce friction and wear on the pipeline and components, extending their service life. Additionally, pneumatic conveying systems can transport coal powder over longer distances with minimal loss, making them suitable for applications where the powder needs to be moved from a production site to a storage or processing facility. Another advantage is the improved safety aspect, as the system is enclosed, reducing the risk of dust explosions or inhalation hazards. The enclosed design also helps in maintaining a clean and controlled environment, which is crucial in industries where dust control is a regulatory requirement. Furthermore, the flexibility of pneumatic conveying allows for easy integration with other process equipment, such as mixers, classifiers, or storage silos, enabling seamless material flow within the plant.
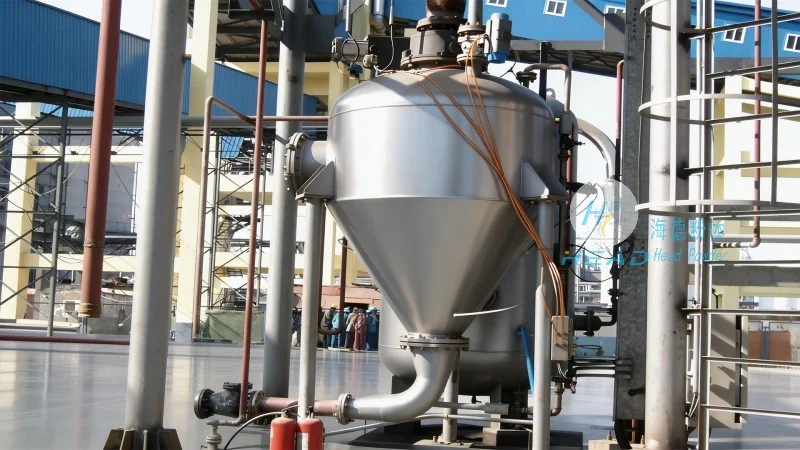
Application Scenarios in Industrial Settings
Coal powder pneumatic conveying equipment is widely used in various industrial sectors, including power generation, cement production, and chemical processing. In power plants, these systems are used to transport coal from storage silos to the boiler feed system, ensuring a continuous and reliable supply of fuel. The ability to handle large volumes of coal powder efficiently makes it ideal for power generation facilities, where consistent fuel supply is critical for maintaining power output. In the cement industry, coal powder is used as a fuel in kilns, and pneumatic conveying systems are employed to transport the coal from storage to the kiln feed point. This ensures that the cement production process runs smoothly without interruptions. In chemical processing plants, coal powder may be used as a raw material or a fuel source, and pneumatic conveying helps in transporting it to reactors or furnaces. The versatility of the system allows it to adapt to different material characteristics and process requirements, making it a preferred choice in diverse industrial applications.
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, is a leading manufacturer and supplier of coal powder pneumatic conveying equipment. The company specializes in designing, manufacturing, and commissioning customized conveying systems tailored to the specific needs of industrial clients. With a strong focus on innovation and quality, headpowder has established itself as a trusted partner in the field of material handling solutions. The company's headquarters is located in Shandong, China, where it has a state-of-the-art manufacturing facility equipped with advanced technology and skilled workforce. This enables headpowder to produce high-quality equipment that meets international standards and complies with industry regulations. The company's product range includes various types of pneumatic conveying systems, such as pressure and suction conveying systems, as well as accessories like hoppers, valves, and filters. Each product is designed with precision engineering to ensure optimal performance and durability. headpowder's commitment to customer satisfaction and technical excellence has earned it a reputation for delivering reliable and efficient solutions to its clients worldwide.
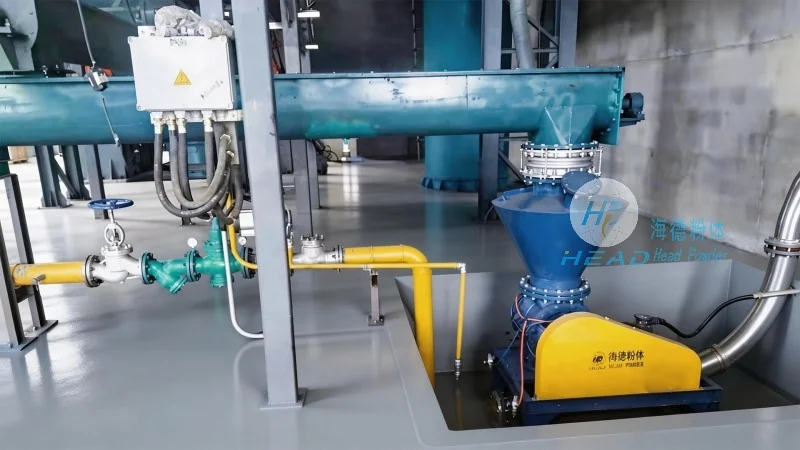
Technical Specifications and Customization Options
headpowder offers a range of technical specifications and customization options to meet the diverse requirements of its clients. The company's coal powder pneumatic conveying systems are available in different pressure ranges, from low-pressure to high-pressure systems, depending on the distance and material characteristics. The conveying line diameter can be customized to suit the volume of coal powder to be transported, with options ranging from small diameters for low-volume applications to large diameters for high-volume industrial use. The feeding system can be designed with different types of feeders, such as rotary valves or screw feeders, to handle various material flow rates and particle sizes. The separation system can be configured with different types of cyclones or filters, depending on the required separation efficiency and the characteristics of the coal powder. Additionally, headpowder provides customization services to integrate the conveying system with existing plant infrastructure, ensuring seamless operation and minimal disruption to the production process. The company's technical team works closely with clients to understand their specific needs and provide tailored solutions that enhance their operational efficiency and reduce costs.
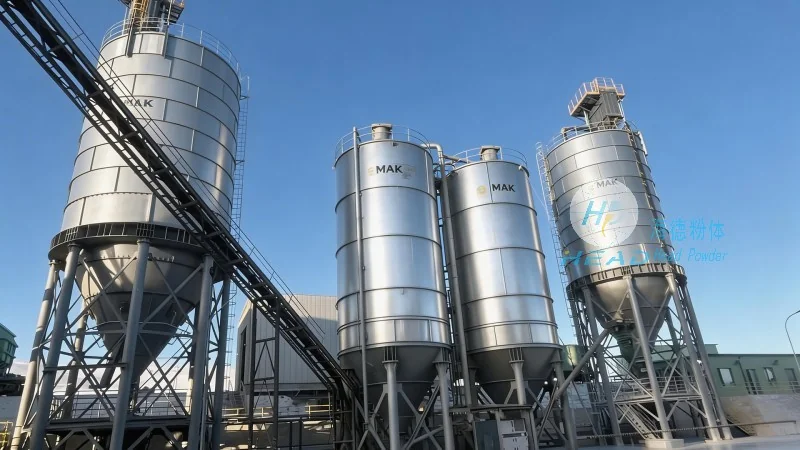
Maintenance and Operational Guidelines
Proper maintenance and operational guidelines are essential to ensure the long-term performance and reliability of coal powder pneumatic conveying equipment. Regular maintenance is crucial to prevent equipment failure and minimize downtime. The maintenance schedule should include routine checks of the conveying line, feeding system, and separation system, as well as replacement of worn parts and cleaning of filters. The air system, including the compressor and air treatment units, should also be regularly maintained to ensure optimal air quality and pressure. Operational guidelines should be followed to ensure safe and efficient operation of the system. This includes proper material feeding to avoid overloading the system, monitoring of air pressure and flow rate, and regular inspection of the system for any signs of wear or damage. By adhering to these guidelines, industrial clients can maximize the lifespan of their equipment and maintain consistent performance. headpowder provides comprehensive maintenance and support services to its clients, including on-site technical support and spare parts supply, to ensure that the equipment operates at its best. The company's technical experts can offer guidance on best practices and troubleshooting to help clients optimize their system performance and reduce maintenance costs.
Conclusion and Future Trends
Coal powder pneumatic conveying equipment plays a vital role in modern industrial processes, offering efficient and safe transportation of fine coal powders. The technology has evolved significantly over the years, with advancements in materials, control systems, and design, leading to more reliable and efficient systems. As industries continue to seek ways to improve operational efficiency and reduce costs, the demand for advanced pneumatic conveying solutions is expected to grow. headpowder, with its expertise and commitment to quality, is well-positioned to meet the evolving needs of the market. By providing customized solutions and comprehensive support, the company helps its clients achieve their operational goals and stay competitive in their respective industries. The future of coal powder pneumatic conveying is likely to involve further integration with automation and digital technologies, enabling real-time monitoring and control of the system. This will enhance the overall performance and reliability of the equipment, making it an even more valuable asset in industrial operations.




