HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for the handling of pulverized materials like bean powder. This article provides a comprehensive exploration of the core technologies behind negative and positive pressure pneumatic conveying systems, focusing on their principles, operational characteristics, and practical applications in the bean powder industry.
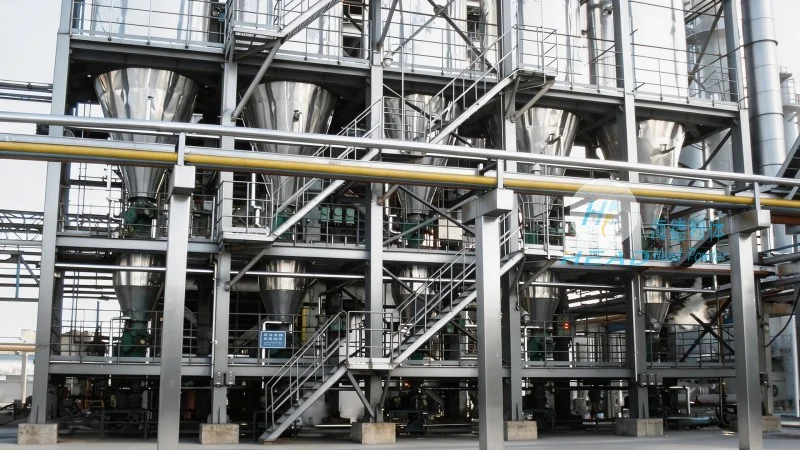
Understanding Pneumatic Conveying Systems for Pulverized Materials
Pneumatic conveying is a critical method for transporting bulk materials, including fine powders such as bean powder, over relatively short to medium distances. Unlike traditional mechanical conveying systems, which rely on belts, screws, or buckets, pneumatic systems utilize air or gas as the medium to move material. This approach offers significant advantages in terms of flexibility, hygiene, and the ability to handle materials that are sensitive to moisture or contamination. The two primary categories of pneumatic conveying systems are negative pressure (suction) and positive pressure (pressure) systems, each with distinct operational principles and suitability for different material handling scenarios.
Negative Pressure (Suction) Pneumatic Conveying Systems
Negative pressure systems, also known as suction or vacuum conveyors, operate by creating a vacuum at the material intake point. This vacuum draws the material from the source, such as a storage silo or hopper, into the conveying line. The system typically consists of a vacuum pump, a filter to separate the material from the air, and a discharge unit where the material is deposited. For bean powder, negative pressure systems are particularly effective when the material is to be transferred from a high elevation to a lower one, or when the source is located in a confined space where positive pressure might pose safety risks. A key advantage of negative pressure systems is their ability to handle materials with a high moisture content or those that are prone to dust explosions, as the vacuum environment reduces the risk of ignition. However, these systems may have limitations in terms of conveying distance and material capacity compared to positive pressure systems.
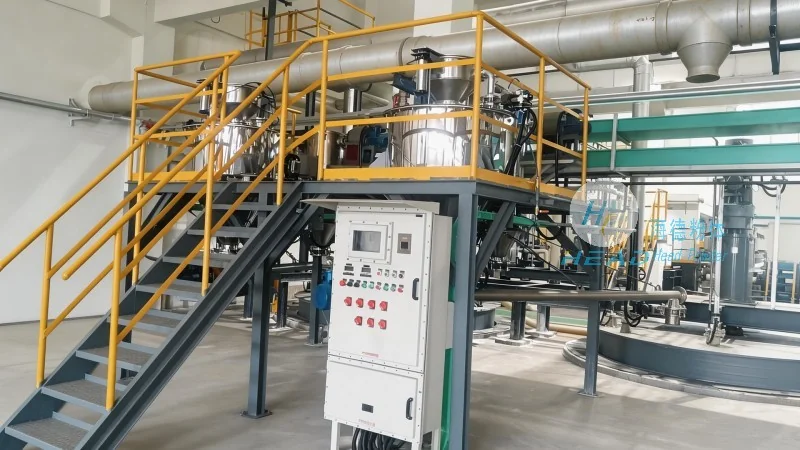
Positive Pressure (Pressure) Pneumatic Conveying Systems
Positive pressure systems, or pressure conveyors, work by forcing air or gas through the material, creating pressure within the conveying line. The material is drawn into the system by the moving air stream and transported to the discharge point. Unlike negative pressure systems, positive pressure systems do not require a vacuum pump and instead rely on a blower or compressor to generate the necessary pressure. These systems are generally more suitable for longer conveying distances and higher material throughput. For bean powder applications, positive pressure systems excel when the material needs to be transported from a lower elevation to a higher one, or when the material is dry and non-explosive. A significant benefit of positive pressure systems is their ability to handle larger volumes of material and maintain consistent flow rates over extended distances. However, they may require more robust equipment to manage higher pressures and can be less effective for materials that are highly cohesive or prone to bridging in the conveying line.
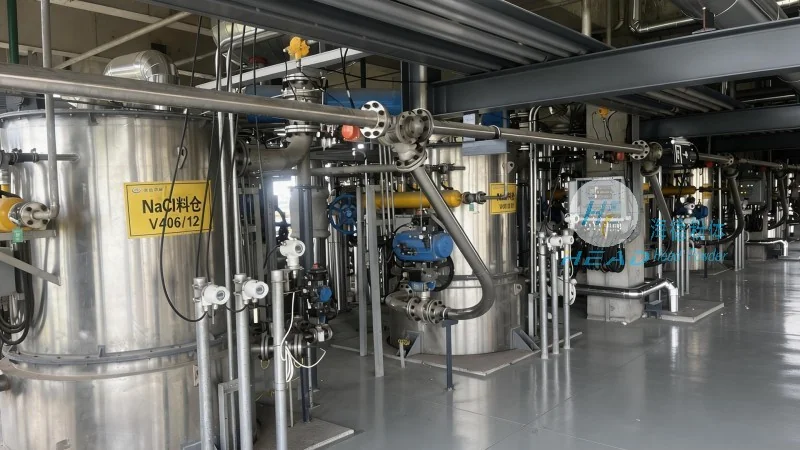
Key Considerations for Selecting the Right System for Bean Powder Handling
The choice between negative and positive pressure pneumatic conveying systems for bean powder depends on several critical factors, including the material's physical properties, the required conveying distance, the elevation changes, and the overall system layout. Material properties such as particle size, moisture content, and dust explosion risk are paramount. For example, bean powder with high moisture content and fine particles may benefit more from a negative pressure system due to its lower risk of ignition and better handling of fine powders. Conversely, if the material is dry and requires long-distance transport, a positive pressure system might be more efficient. Additionally, the layout of the facility, including the positions of the source and destination, plays a crucial role. If the destination is at a higher elevation than the source, a positive pressure system is often preferred, while a negative pressure system may be more suitable for the reverse scenario.
Applications and Practical Implementation in the Bean Powder Industry
In the bean powder industry, pneumatic conveying systems are widely used in various stages of production and processing. For instance, in the initial stage of processing, bean powder may need to be transferred from storage silos to processing equipment such as mills or mixers. A negative pressure system can efficiently draw the powder from the silo and deliver it to the processing unit, especially if the silo is located above the processing equipment. In the later stages, when the processed powder needs to be moved to packaging or storage areas, a positive pressure system may be employed to transport the material over longer distances or to higher elevation storage tanks. The flexibility of pneumatic systems allows for integration into existing production lines with minimal disruption, and their hygienic design makes them ideal for food processing applications where contamination control is essential. HeadPowder's expertise in customizing pneumatic conveying solutions ensures that clients can optimize their material handling processes, improving efficiency, reducing downtime, and maintaining product quality.
Conclusion and Future Trends
Both negative and positive pressure pneumatic conveying systems offer valuable solutions for the efficient and safe handling of bean powder. The choice between the two depends on a thorough analysis of operational requirements and material characteristics. As technology advances, modern pneumatic conveying systems incorporate advanced features such as variable speed drives, real-time monitoring, and automated controls to enhance performance and reliability. These innovations help in optimizing energy consumption, reducing maintenance costs, and improving overall system efficiency. For businesses in the bean powder industry, investing in a well-designed pneumatic conveying system from a reputable engineering firm like HeadPowder can lead to significant operational benefits, including increased productivity, reduced material waste, and improved safety standards. By understanding the principles and applications of both negative and positive pressure systems, industry professionals can make informed decisions to select the most suitable technology for their specific needs, ensuring long-term success in their material handling operations.




