Organic fertilizer production and distribution rely heavily on efficient material handling systems to ensure consistent quality and operational reliability. Pneumatic conveying technology has emerged as a critical solution for transporting granular organic fertilizers, offering advantages such as reduced contamination, improved safety, and enhanced process control. This article explores the application and optimization of pneumatic conveying systems specifically designed for organic fertilizer granules, highlighting the expertise of Shandong HeadPowder Engineering Co., Ltd. in delivering tailored solutions for the agricultural industry.
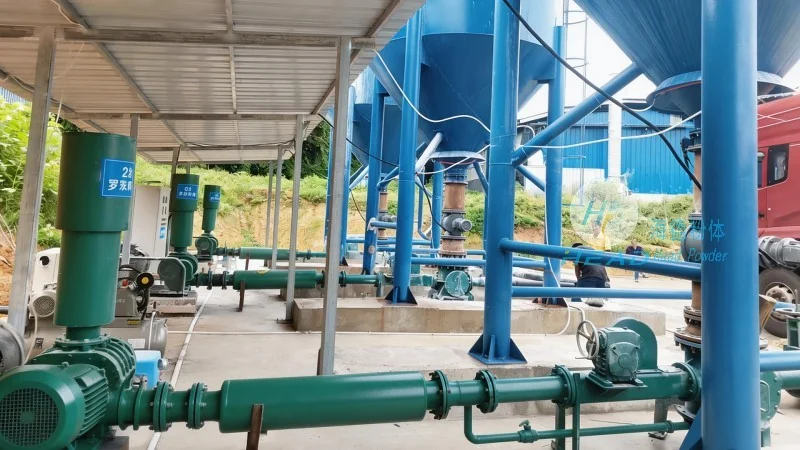
Key Features of Pneumatic Conveying Systems for Organic Fertilizer Granules
HeadPowder specializes in designing and implementing pneumatic conveying systems that address the unique challenges of organic fertilizer granules. These systems are engineered to handle materials with varying moisture content, particle sizes, and flow characteristics. The technology utilizes air pressure to move granules through pipelines, eliminating the need for mechanical components that could introduce contaminants or cause wear and tear. Key features include:
1. Customized Pipeline Design: Systems are tailored to the specific dimensions and layout of the fertilizer production facility, ensuring optimal material flow and minimal pressure loss.
2. Variable Airflow Control: Advanced control systems allow for precise adjustment of air velocity, which is crucial for maintaining consistent granule velocity and preventing material degradation or clogging.
3. Material Handling Flexibility: The ability to handle different types of organic fertilizers, including compost, manure-based products, and blended formulations, without compromising system performance.
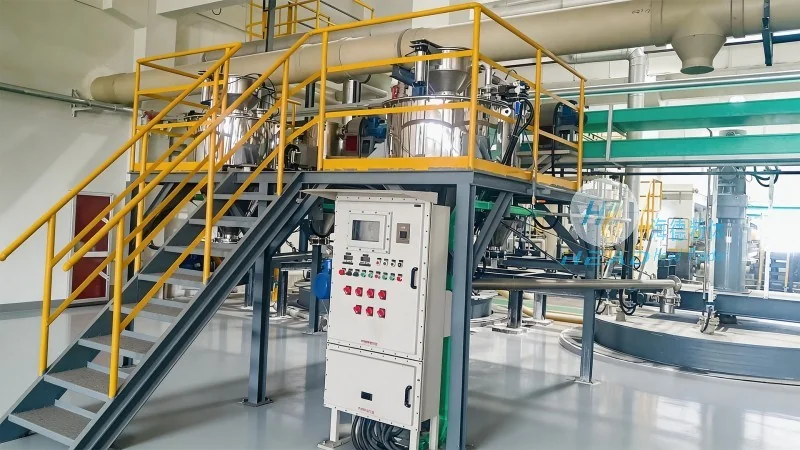
4. Energy Efficiency: Optimized air pressure and flow rates reduce energy consumption compared to traditional mechanical conveying methods, contributing to lower operational costs.
Optimization Strategies for Pneumatic Conveying in Organic Fertilizer Processing
Optimizing pneumatic conveying systems for organic fertilizer granules involves several strategic considerations to maximize efficiency and reliability. Shandong HeadPowder Engineering Co., Ltd. employs a systematic approach to ensure that each system is tailored to the client's specific needs. Key optimization strategies include:
1. System Sizing and Capacity Planning: Proper sizing of the conveying line, air compressor, and control valves is essential to match the production rate and material characteristics, preventing under or overloading.
2. Material Characterization Studies: Conducting thorough analysis of the granule size distribution, moisture content, and flow properties to select the most appropriate conveying method (e.g., dilute-phase or dense-phase) and system configuration.
3. Integration with Existing Infrastructure: Ensuring seamless integration with the client's current production and storage facilities, minimizing downtime and installation costs.
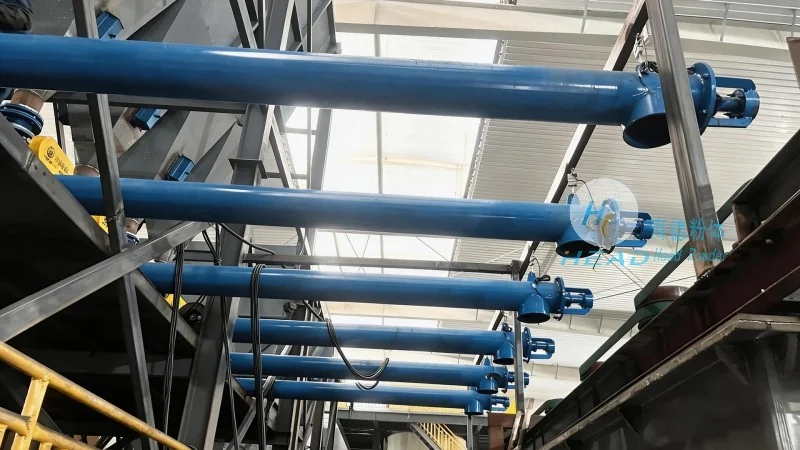
4. Regular Maintenance and Monitoring: Implementing preventive maintenance schedules and real-time monitoring systems to detect and address issues such as clogging or pressure drops promptly, maintaining system performance and extending equipment lifespan.
Benefits of Implementing Pneumatic Conveying Technology for Organic Fertilizer Granules
Adopting pneumatic conveying systems for organic fertilizer granules offers numerous benefits that enhance both operational efficiency and product quality. These advantages include:
1. Reduced Contamination Risk: The enclosed system prevents exposure to dust, moisture, and other environmental factors, maintaining the purity of the organic fertilizer.
2. Improved Safety: Eliminating the need for manual handling of granules reduces the risk of respiratory issues and other health hazards associated with organic materials.
3. Enhanced Process Control: Precise control over air pressure and flow allows for consistent granule velocity, ensuring uniform distribution and preventing segregation of different fertilizer components.
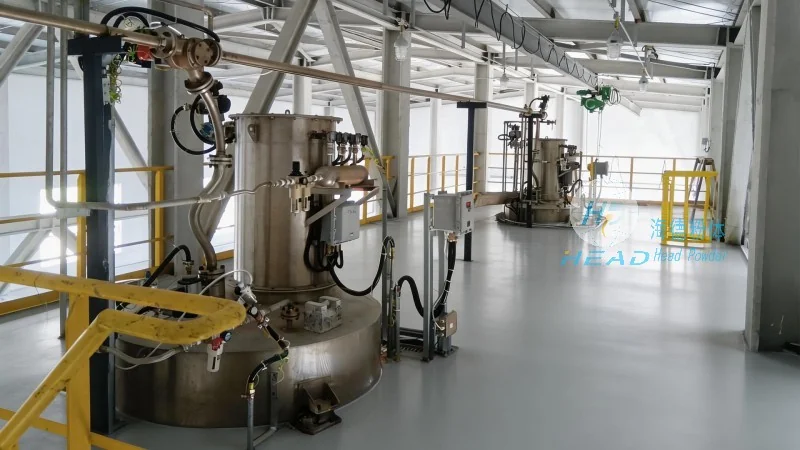
4. Increased Throughput: High-capacity pneumatic systems can handle large volumes of granules quickly, supporting higher production rates and meeting market demands efficiently.
5. Lower Maintenance Costs: The absence of moving parts in the conveying line reduces wear and tear, leading to lower maintenance expenses and extended equipment lifespan.
Case Study: Successful Implementation by Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd. has successfully implemented pneumatic conveying systems for several organic fertilizer manufacturers, delivering measurable improvements in operational efficiency and product quality. For example, one client, a leading producer of compost-based granules, experienced a 20% increase in production capacity after upgrading to a customized pneumatic conveying system. The system's optimized airflow control and pipeline design reduced material clogging and pressure losses, allowing for continuous operation without interruptions. Additionally, the enclosed system minimized contamination, resulting in higher product purity and improved customer satisfaction.
Conclusion and Future Directions
Pneumatic conveying technology continues to play a vital role in the efficient handling of organic fertilizer granules, offering a sustainable and reliable solution for modern agricultural operations. Shandong HeadPowder Engineering Co., Ltd. remains committed to providing innovative and optimized solutions tailored to the evolving needs of the organic fertilizer industry. By leveraging advanced engineering principles and customer-focused design, the company ensures that its pneumatic conveying systems not only meet current industry standards but also adapt to future technological advancements, supporting the long-term success of its clients.




