Pneumatic conveying technology has emerged as a critical solution for the efficient and reliable transport of cereal flakes, a key component in the food processing industry. As a specialized engineering firm, Shandong HeadPowder Engineering Co., Ltd. (referred to as HeadPowder) has dedicated significant resources to the research and development of advanced pneumatic conveying systems tailored for cereal flakes. This article explores the application and optimization strategies of such technology, highlighting the benefits and practical implementations in modern food processing operations.
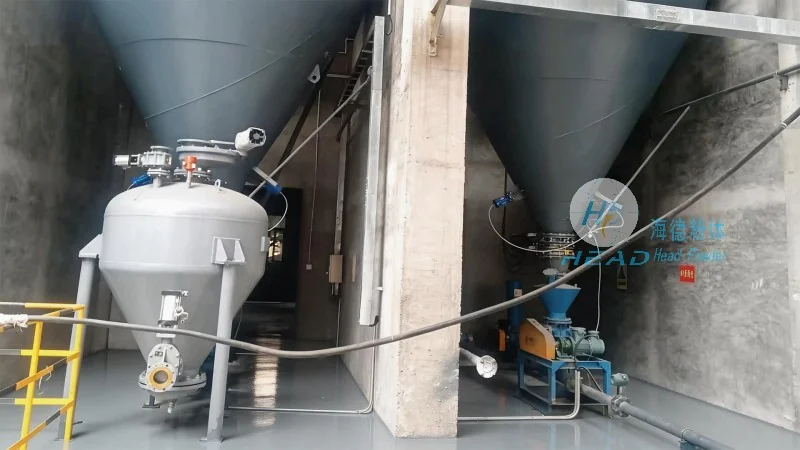
Key Benefits of Pneumatic Conveying for Cereal Flakes
Traditional transport methods for cereal flakes, such as belt conveyors or bucket elevators, often face challenges like product degradation, contamination risks, and operational inefficiencies. Pneumatic conveying systems, however, offer several advantages that address these issues. Firstly, they provide a closed system that minimizes exposure to external contaminants, ensuring the purity and quality of the product. Secondly, the technology allows for gentle handling of delicate cereal flakes, reducing breakage and maintaining their texture and nutritional value. Additionally, pneumatic conveyors can achieve high transport speeds and cover longer distances with fewer intermediate transfer points, enhancing overall operational efficiency. These benefits make pneumatic conveying an ideal choice for manufacturers seeking to improve the safety, quality, and productivity of their cereal flakes handling processes.
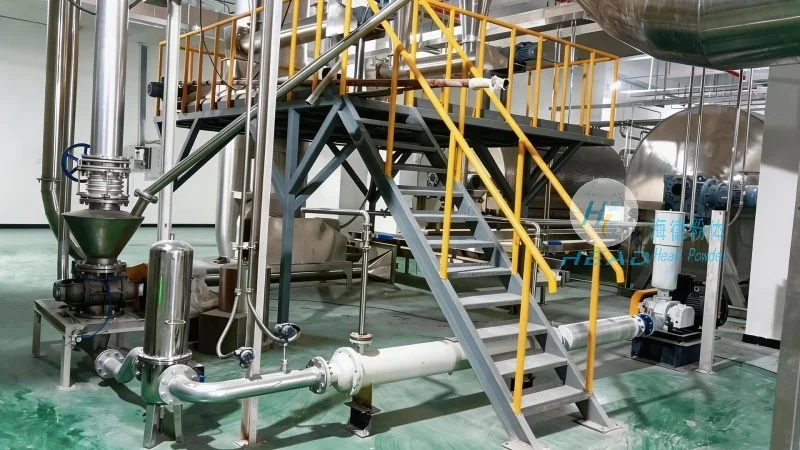
Optimization Strategies for Pneumatic Conveying Systems
Optimizing pneumatic conveying systems for cereal flakes involves a combination of technical adjustments and system design considerations. HeadPowder emphasizes several key strategies to maximize performance and minimize operational costs. One critical aspect is the selection of appropriate air velocity and pressure levels. The optimal air velocity must be balanced to ensure effective particle suspension without excessive energy consumption. HeadPowder engineers typically conduct thorough calculations based on the specific characteristics of the cereal flakes, such as particle size, density, and moisture content, to determine the most efficient air parameters. Another crucial factor is the design of the conveying line, including the use of appropriate pipe diameters, bends, and accessories. Properly sized and configured components reduce pressure losses and prevent blockages, ensuring smooth and continuous operation. Furthermore, the integration of advanced control systems allows for real-time monitoring and adjustment of conveying parameters, enabling operators to respond quickly to changes in production demands or system performance.
Case Study: Implementing Optimized Pneumatic Conveying in a Cereal Processing Plant
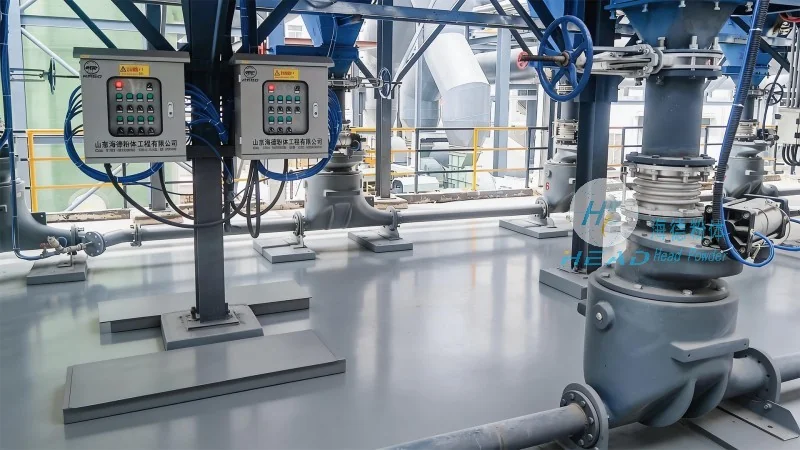
A recent project undertaken by HeadPowder involved the installation of an optimized pneumatic conveying system for a leading cereal manufacturer in Shandong, China. The client required a solution to replace an aging, inefficient belt conveyor system that was causing frequent product breakage and contamination issues. HeadPowder's team conducted a comprehensive analysis of the existing process, including material flow analysis and operational data collection. Based on the findings, a custom-designed pneumatic conveying system was developed, incorporating high-efficiency air compressors, specialized conveying pipes, and advanced control panels. The implementation phase involved careful installation and commissioning to ensure the system operated within the specified parameters. Post-implementation, the client reported significant improvements: product breakage reduced by over 60%, contamination incidents decreased by 90%, and overall transport efficiency increased by 30%. This case study exemplifies the effectiveness of optimized pneumatic conveying technology in enhancing product quality and operational performance.
Conclusion and Future Directions
Pneumatic conveying technology continues to evolve, with ongoing research focused on improving energy efficiency, reducing maintenance costs, and expanding the range of materials suitable for transport. HeadPowder remains committed to staying at the forefront of this technology, leveraging its expertise to develop customized solutions that meet the unique needs of its clients. By focusing on optimization and continuous improvement, the company aims to provide reliable, efficient, and cost-effective pneumatic conveying systems that contribute to the success of the food processing industry. For businesses seeking to enhance their cereal flakes transport operations, partnering with a specialized engineering firm like HeadPowder can lead to significant improvements in product quality, operational efficiency, and overall competitiveness.




