Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a professional manufacturer specializing in the design, development, and production of advanced powder conveying systems. With a strong focus on innovation and precision engineering, the company has established itself as a leading provider in the field of white carbon black handling solutions. HeadPowder is headquartered in Shandong, China, and serves a diverse range of industries including rubber, plastics, and chemical processing.
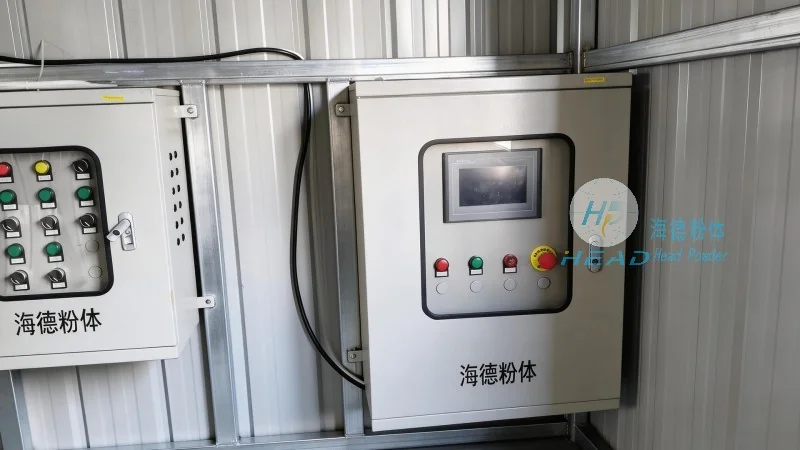
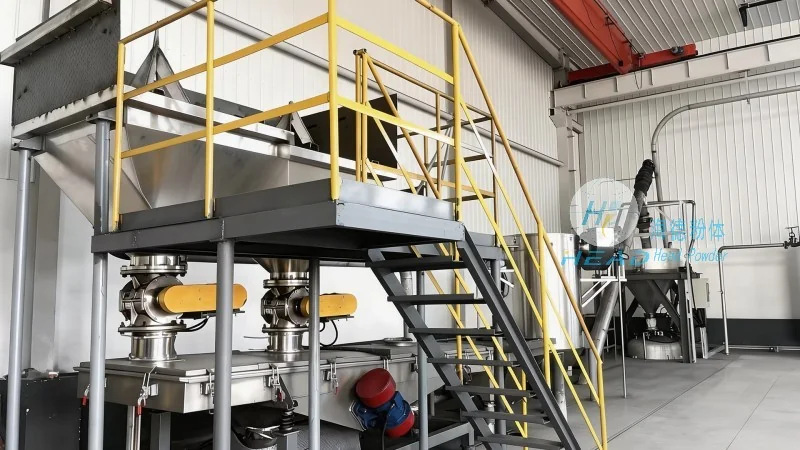
Overview of the White Carbon Black Powder Conveying System
The white carbon black powder conveying system is a specialized equipment designed to efficiently transport white carbon black, a critical filler material used in various industrial applications. This system addresses the unique challenges associated with handling fine powders, such as dust generation, material segregation, and flow control. By integrating advanced technologies and robust components, the system ensures reliable and safe powder transfer from storage to processing units. The design emphasizes durability, low maintenance, and high efficiency, making it suitable for both small-scale and large-scale production environments.
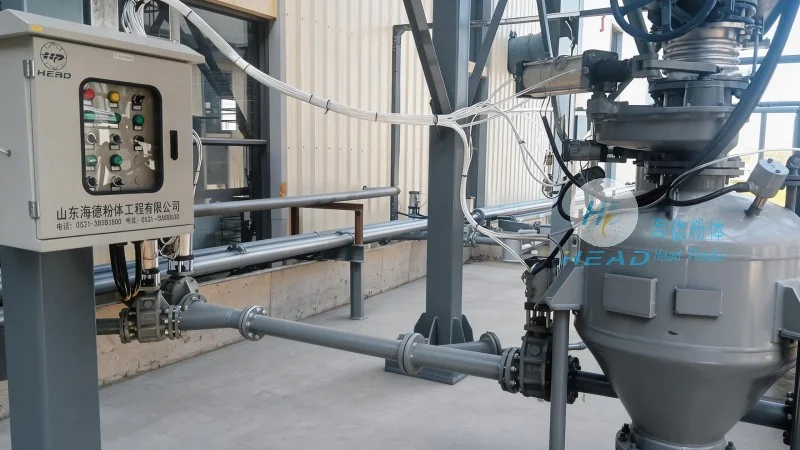
Structural Design and Working Principle
The white carbon black powder conveying system comprises several key components, each playing a vital role in the overall operation. The primary structure includes a hopper for material storage, a conveyor mechanism (such as a screw or pneumatic system), and a control unit for regulating flow. The hopper is typically equipped with a dust collection system to minimize airborne particles and maintain a clean working environment. The conveyor mechanism is engineered to handle the specific properties of white carbon black, including its fine particle size and potential for static electricity. The control unit monitors parameters like pressure, flow rate, and temperature, ensuring optimal performance and preventing system failures. The structural design of the system is optimized for the handling of fine, abrasive powders. The hopper is constructed from corrosion-resistant materials, such as stainless steel or high-density polyethylene, to withstand the chemical properties of white carbon black and prevent material degradation. The inlet and outlet are equipped with specialized valves to control the flow of material, ensuring smooth and controlled discharge. The conveyor mechanism, often a screw conveyor, is designed with a smooth, non-stick surface to prevent powder buildup and maintain consistent flow rates. The system also includes a pressure sensor and a flow meter to provide real-time monitoring of the conveying process. This data is transmitted to the control unit, which adjusts the system parameters to maintain optimal performance. The control unit may include programmable logic controllers (PLCs) and human-machine interfaces (HMIs) for easy operation and troubleshooting.
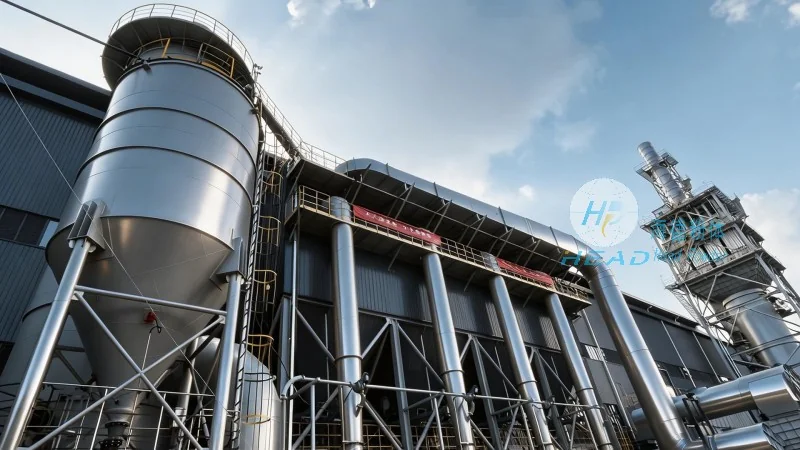
Advantages and Applications
The white carbon black powder conveying system offers several advantages that enhance operational efficiency and product quality. By reducing material loss and dust contamination, the system improves the purity of the conveyed powder, which is crucial for applications in rubber compounding and plastic manufacturing. The system's modular design allows for easy integration into existing production lines, minimizing downtime during installation and maintenance. Additionally, the use of advanced materials and engineering ensures long-term reliability, reducing the need for frequent repairs and replacements. HeadPowder's systems are widely used in industries where consistent and high-quality powder transfer is essential, such as tire manufacturing, rubber products, and plastic additives. One of the key advantages of the white carbon black powder conveying system is its ability to handle high volumes of material with minimal human intervention. The automated control system reduces the risk of operator error and ensures consistent product quality. The system's low energy consumption and low maintenance requirements contribute to cost savings over time. Additionally, the dust collection system integrated into the hopper helps maintain a safe working environment by capturing airborne particles, reducing the risk of respiratory issues and improving overall workplace safety. The modular design of the system allows for customization based on specific production needs, such as varying conveyor speeds or material capacities. This flexibility makes the system suitable for a wide range of applications, from small-scale laboratory testing to large-scale industrial production.




