

Introduction to Nitrogen-Protected Powder Handling and Conveying Systems: Structure and Working Prin
HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design and implementation of advanced powder handling solutions. This article provides an overview of the nitrogen-protected powder conveying system, detailing its structural design and operational principles to enhance safety and efficiency in industrial applications.
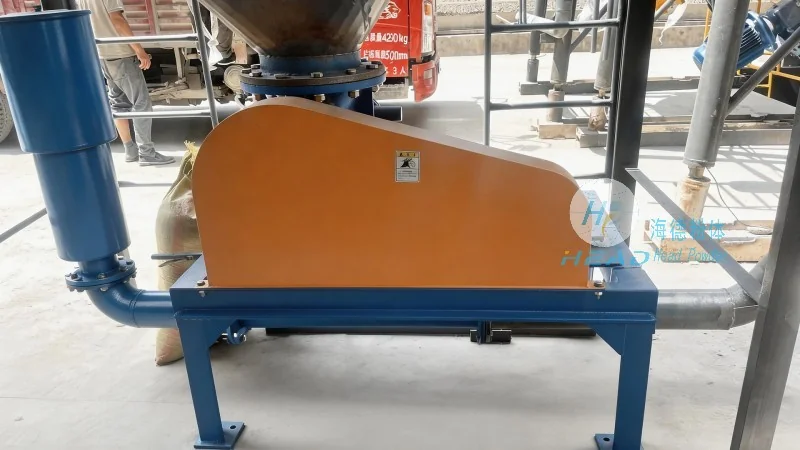
Company Overview and Core Expertise
HeadPowder Engineering Co., Ltd. is a professional enterprise dedicated to providing comprehensive powder processing technologies. With a focus on innovation and precision, the company has established itself as a key player in the field of powder handling systems. Based in Shandong, China, HeadPowder leverages local industrial resources and global expertise to deliver high-quality solutions tailored to diverse industrial needs.
Understanding Nitrogen-Protected Powder Conveying Systems
The nitrogen-protected powder conveying system is a critical component in industries where the integrity and purity of powders are paramount. This system is designed to maintain an inert atmosphere, typically using nitrogen gas, to prevent oxidation, moisture absorption, or contamination during the conveying process. Such systems are widely used in pharmaceuticals, food processing, and chemical manufacturing, where product quality and safety are non-negotiable.
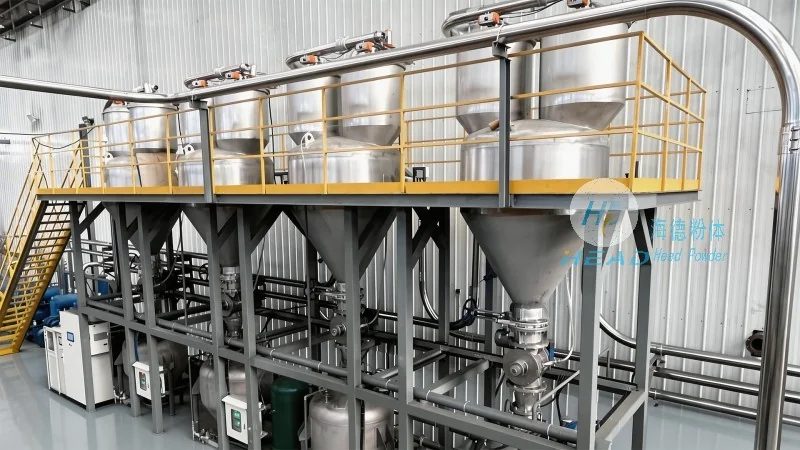
Structural Components and Design Principles
The system's structure is engineered to ensure seamless and safe powder transfer while maintaining the protective nitrogen environment. Key components include:
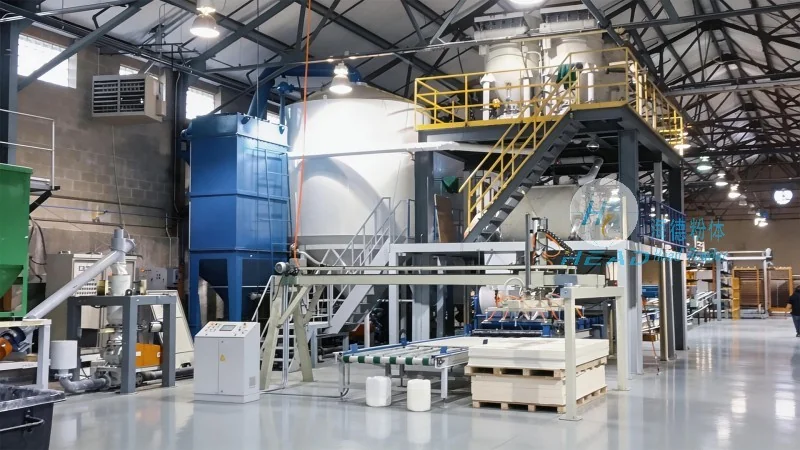
- Nitrogen Supply and Purification Unit: This unit generates and purifies nitrogen gas to ensure it meets the required purity standards, typically with low oxygen content. The system may incorporate filters and regulators to maintain consistent gas quality.
- Powder Hopper and Storage: The hopper is designed to store the powder under a nitrogen blanket, preventing exposure to ambient air. It often features a venting system that connects to the nitrogen supply to maintain an inert atmosphere.
- Pneumatic Conveying Pipeline: The pipeline is constructed from materials resistant to corrosion and chemical reactions, such as stainless steel or specialized plastics. It is equipped with valves, elbows, and other fittings to control the flow direction and speed of the powder.
- Control and Monitoring System: An integrated control panel allows operators to monitor and adjust the system parameters, including nitrogen flow rate, pressure, and powder feed rate. Sensors may be installed to detect any leaks or deviations from the desired conditions.
Working Principles and Operational Flow
The operational principle of the nitrogen-protected powder conveying system involves a sequence of steps to ensure safe and efficient powder transfer:
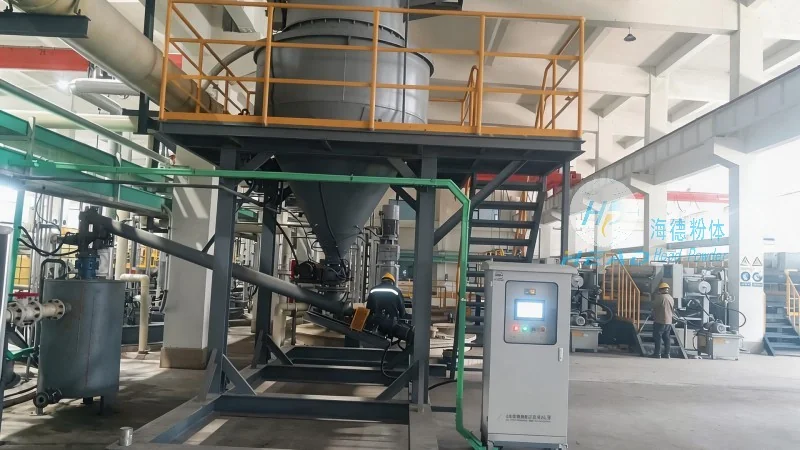
- Nitrogen Purging: Before starting the conveying process, the entire system is purged with nitrogen to displace any residual air and create an inert environment. This step is crucial to prevent oxidation or moisture contamination.
- Powder Loading: The powder is loaded into the hopper under the nitrogen blanket. The hopper's vent is connected to the nitrogen supply to maintain the protective atmosphere.
- Conveying Process: The powder is pneumatically conveyed through the pipeline using the nitrogen gas as the carrier medium. The gas flow is controlled to ensure a consistent and controlled powder flow rate, minimizing particle degradation or segregation.
- Discharge and Collection: The powder is discharged into the receiving container, which is also under a nitrogen blanket to maintain purity. The system ensures that the entire process remains sealed and protected from external contaminants.
Benefits and Applications
The nitrogen-protected powder conveying system offers several advantages, including enhanced product quality, improved safety, and increased operational efficiency. By maintaining an inert atmosphere, it prevents product degradation, extends shelf life, and ensures compliance with regulatory standards. The system is particularly beneficial in industries where product purity is critical, such as pharmaceuticals, food, and specialty chemicals.
Conclusion
HeadPowder Engineering Co., Ltd. provides advanced nitrogen-protected powder conveying systems that combine robust engineering with innovative design. By understanding the structural components and operational principles, industries can leverage these systems to enhance their production processes while maintaining the highest standards of product quality and safety. With a commitment to excellence and customer satisfaction, HeadPowder continues to lead in the development of cutting-edge powder handling solutions.