HeadPowder, a leading provider in the field of industrial material handling solutions, specializes in the design and manufacturing of advanced dust-free bulk bag loading stations. Based in Shandong, China, the company has established itself as a trusted partner for businesses seeking efficient and reliable equipment for handling bulk materials. This article delves into the core principles of dust-free bulk bag loading stations and highlights the key working scene characteristics that make them indispensable in modern industrial operations.
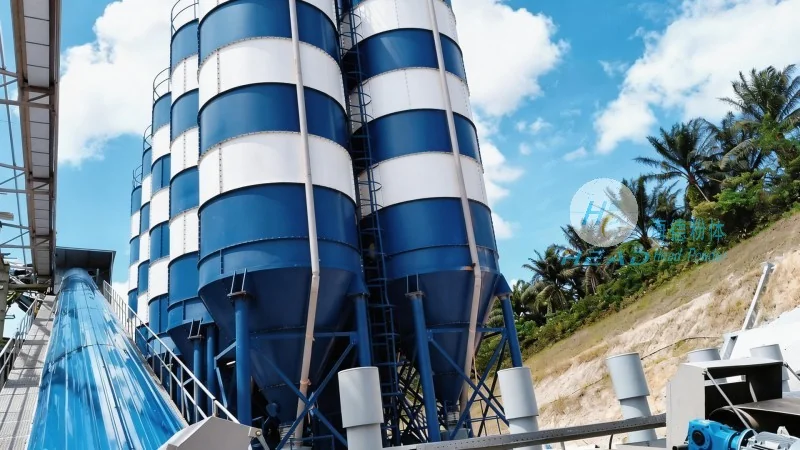
Understanding the Core Principles of Dust-Free Bulk Bag Loading Stations
The dust-free bulk bag loading station is engineered to handle large quantities of bulk materials from ton bags while maintaining a controlled, dust-free environment. The primary principle revolves around the use of sealed systems and advanced filtration technologies to prevent material contamination and environmental pollution. When a ton bag is placed on the loading platform, the system automatically seals the bag's opening, ensuring that material is discharged only through the designated outlet. This process minimizes dust generation and protects both the material and the surrounding environment. The equipment typically incorporates a hopper or a funnel that connects to the ton bag, allowing for smooth material flow. Additionally, the system may include a vacuum or pressure-assisted mechanism to regulate the discharge rate, ensuring precise control over the material output. The design also emphasizes safety features, such as emergency stop buttons and overload protection, to safeguard operators and prevent equipment damage.
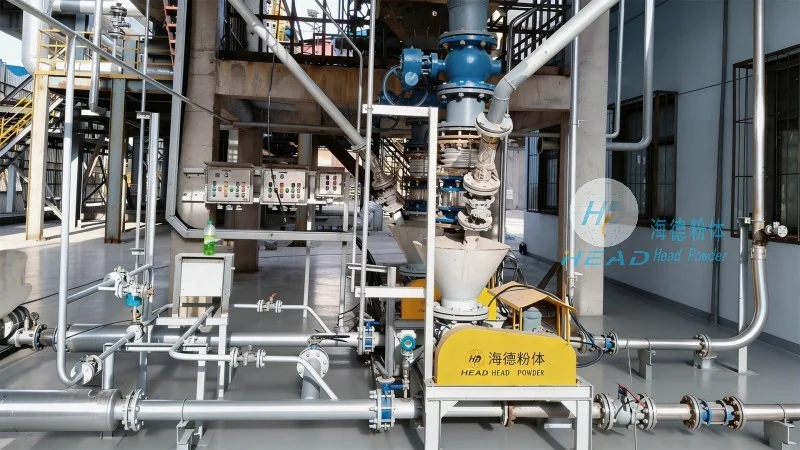
Key Working Scene Characteristics of Dust-Free Bulk Bag Loading Stations
The working scene characteristics of dust-free bulk bag loading stations are tailored to meet the diverse needs of industrial applications. These stations are commonly employed in sectors like chemical manufacturing, food processing, pharmaceuticals, and construction, where handling large volumes of powders or granules is essential. One of the most notable characteristics is their ability to handle various bulk materials, including dry powders, granules, and even wet materials, depending on the specific design. The stations are designed to be flexible, allowing for easy integration with existing production lines or material handling systems. This adaptability makes them suitable for both new installations and retrofits in existing facilities. Another key characteristic is their high efficiency in material throughput. By automating the loading process, these stations reduce manual labor and minimize downtime, leading to increased productivity. The dust-free design also contributes to a safer working environment, as it eliminates the risk of respiratory issues or material contamination that can arise from traditional, open-air handling methods. Furthermore, the stations are built with durability in mind, using high-quality materials and robust construction to withstand heavy usage and harsh conditions. This ensures long-term reliability and low maintenance costs for the end-user.
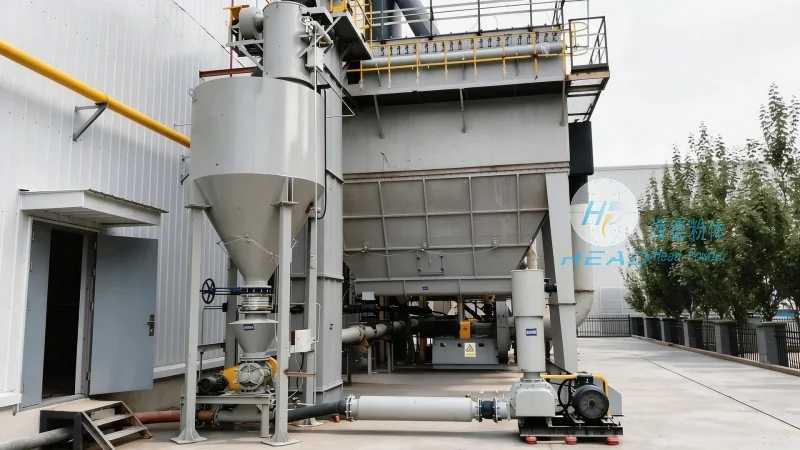
Application Examples and Industry Impact
HeadPowder's dust-free bulk bag loading stations have been successfully implemented in numerous industrial settings. For instance, in a chemical manufacturing plant, the equipment was used to handle hazardous powders, ensuring that the material was transferred safely without any exposure to the environment. In a food processing facility, the station was integrated into the production line to handle ingredients like flour and sugar, maintaining strict hygiene standards. The construction industry has also benefited from these stations, as they efficiently handle bulk materials like cement and sand, reducing the need for manual handling and improving operational efficiency. The impact of these stations extends beyond individual companies, as they contribute to overall industry standards by promoting safer and more sustainable material handling practices. By reducing waste and improving material quality, these systems help businesses achieve higher profitability and compliance with regulatory requirements.
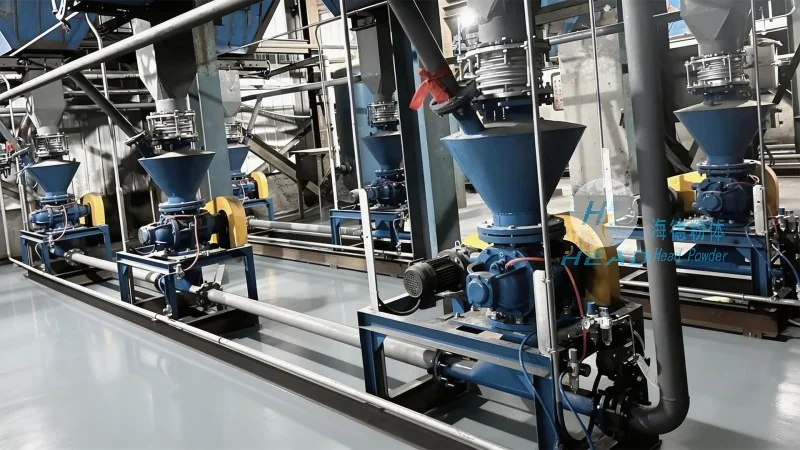
Conclusion and Future Outlook
In conclusion, dust-free bulk bag loading stations represent a significant advancement in industrial material handling technology. The principles of sealed systems, advanced filtration, and precise control make these devices highly effective in maintaining a clean and safe working environment. The working scene characteristics, including adaptability, efficiency, and durability, ensure that they are suitable for a wide range of applications across various industries. As industries continue to prioritize sustainability and operational efficiency, the demand for such equipment is expected to grow. HeadPowder, with its expertise and commitment to quality, remains at the forefront of this technology, providing reliable solutions that meet the evolving needs of modern industrial operations.




