Activated carbon material pneumatic conveying systems are advanced industrial equipment designed to transport activated carbon efficiently and safely. These systems utilize air or gas as the conveying medium to move bulk materials through pipelines, offering a reliable solution for various industrial applications. The core of such systems lies in their ability to handle fine powders like activated carbon, which are often challenging to transport using traditional methods.
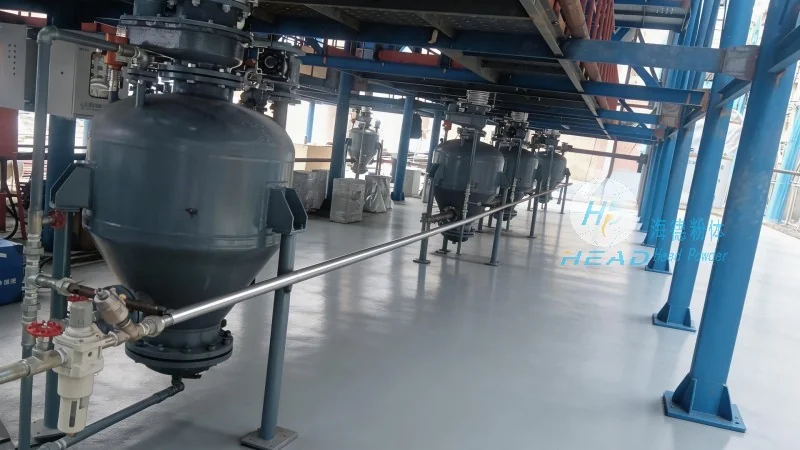
Working Principle of Activated Carbon Pneumatic Conveying Systems
The operation of activated carbon material pneumatic conveying systems is based on the principle of fluidization and air flow. In these systems, a fan or blower generates a high-pressure air stream that is introduced into the material feed point. The activated carbon particles are then drawn into the pipeline by the moving air, forming a dense or dilute phase flow depending on the system design. The conveying process involves several key components, including a hopper for material storage, a feeder to control the material flow rate, a pipeline network for transportation, and a receiver for material discharge. The air flow rate is carefully regulated to ensure optimal material transport without causing excessive pressure drops or particle degradation. The system may operate in either positive or negative pressure modes, with positive pressure systems being more common for long-distance or multi-point delivery, as they can maintain consistent air pressure throughout the pipeline and prevent dust leakage. Negative pressure systems, on the other hand, are often used for short-distance conveying or when the material needs to be collected from an open environment, as they create a vacuum that draws the material into the system.
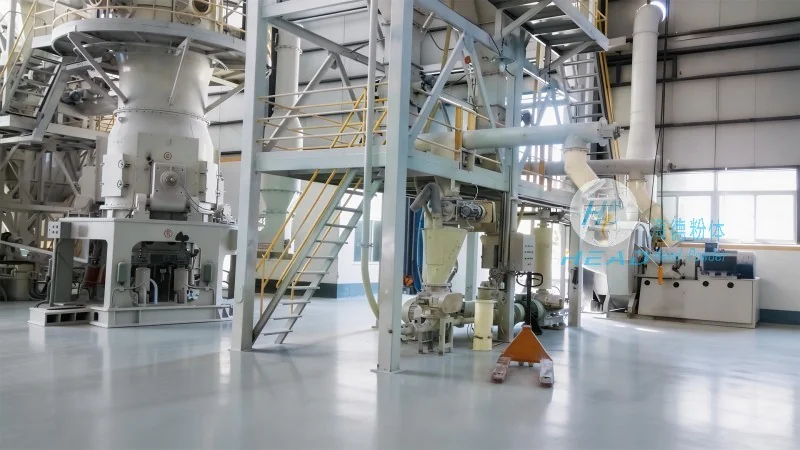
Key Features of Activated Carbon Pneumatic Conveying Systems
Activated carbon material pneumatic conveying systems offer several distinct advantages that make them ideal for industrial use. One of the primary features is their ability to handle fine, abrasive materials like activated carbon without causing significant wear on the equipment. The smooth pipeline surfaces and specialized materials used in the construction of these systems, such as stainless steel or PTFE-lined components, minimize friction and prevent particle buildup, ensuring long-term durability. Another important feature is the system's flexibility in terms of layout and configuration. Pneumatic conveying systems can be customized to fit various plant layouts, with the ability to add multiple inlets or outlets for material distribution. This flexibility allows for efficient integration into existing production lines, reducing the need for extensive modifications. Additionally, these systems provide excellent control over material flow, with adjustable air pressure and flow rates that can be fine-tuned to match the specific requirements of the activated carbon being transported. This precise control helps maintain consistent product quality and prevents over-conveying or under-conveying, which can affect downstream processes. Environmental considerations are also a key feature of modern activated carbon pneumatic conveying systems. Many systems are equipped with dust collection and filtration units to minimize air pollution and comply with environmental regulations. The enclosed pipeline design reduces dust emissions, making the operation safer for personnel and more environmentally friendly. Furthermore, the systems are designed to be energy-efficient, with optimized air flow and fan selection that reduces energy consumption while maintaining effective material transport. This energy efficiency not only lowers operational costs but also contributes to sustainable industrial practices.
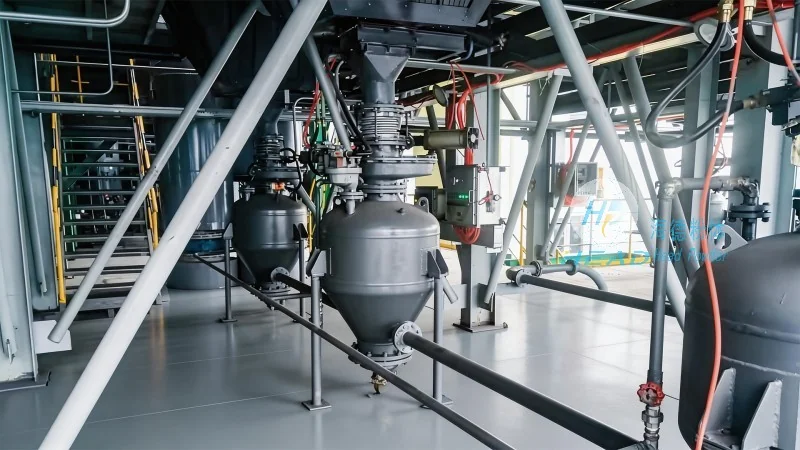
Applications and Benefits in Industrial Settings
Activated carbon material pneumatic conveying systems find widespread application in industries where activated carbon is a critical component, such as water treatment, air purification, and chemical processing. In water treatment facilities, these systems are used to transport activated carbon to filtration units, ensuring consistent and efficient water purification. The ability to handle large volumes of activated carbon quickly and reliably supports the high demand for water treatment in municipal and industrial settings. In air purification systems, the pneumatic conveying systems deliver activated carbon to adsorption towers, where it plays a crucial role in removing contaminants like volatile organic compounds (VOCs) and odors. The precise control over material flow in these systems helps maintain the optimal carbon loading in the adsorption towers, enhancing the efficiency of the air purification process. In chemical processing industries, activated carbon is often used as a catalyst or adsorbent in various reactions. The pneumatic conveying systems ensure that the activated carbon is delivered to reactors and processing units in a controlled manner, preventing contamination and ensuring consistent reaction conditions. The benefits of using these systems in these applications include improved process efficiency, reduced downtime due to material handling issues, and enhanced product quality. The reliability of pneumatic conveying systems also contributes to overall operational stability, as they minimize the risk of material blockages or spills that can occur with traditional handling methods. Additionally, the enclosed design of the systems reduces the risk of dust exposure for workers, improving workplace safety and compliance with occupational health standards.
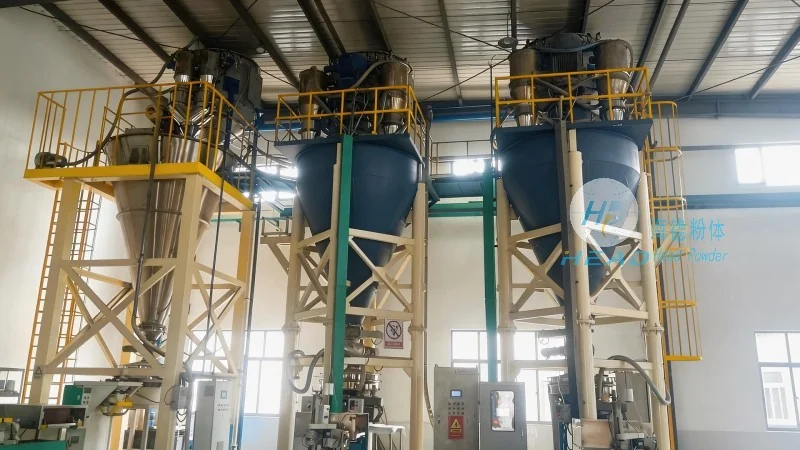
Company Overview: Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of industrial conveying systems, including activated carbon material pneumatic conveying solutions. With a strong focus on innovation and quality, HeadPowder has established itself as a trusted partner for businesses in various industries that require efficient and reliable material handling. The company is headquartered in Shandong, China, and has a team of experienced engineers and technicians dedicated to developing cutting-edge conveying technologies. HeadPowder's commitment to customer satisfaction is reflected in its comprehensive product range and customized solutions. The company offers a variety of pneumatic conveying systems tailored to the specific needs of different industries, ensuring that clients receive equipment that meets their operational requirements. HeadPowder's products are designed with durability and efficiency in mind, using high-quality materials and advanced manufacturing techniques to ensure long-term performance. The company also provides after-sales support, including maintenance services and technical assistance, to ensure that clients can maximize the lifespan and effectiveness of their conveying systems. HeadPowder's expertise in activated carbon material handling has made it a preferred choice for many clients, who appreciate the company's ability to deliver systems that are both effective and cost-efficient. The company's reputation for quality and reliability has helped it build a strong customer base, with clients ranging from small-scale operations to large industrial facilities. HeadPowder continues to invest in research and development to stay at the forefront of conveying technology, ensuring that its products remain competitive and aligned with the evolving needs of the industry.




