Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design, development, and production of advanced pneumatic conveying systems tailored for handling tonne bag materials. With a strong commitment to engineering excellence and customer satisfaction, the company has established itself as a trusted provider in the industry, delivering reliable solutions that meet the diverse needs of various sectors.
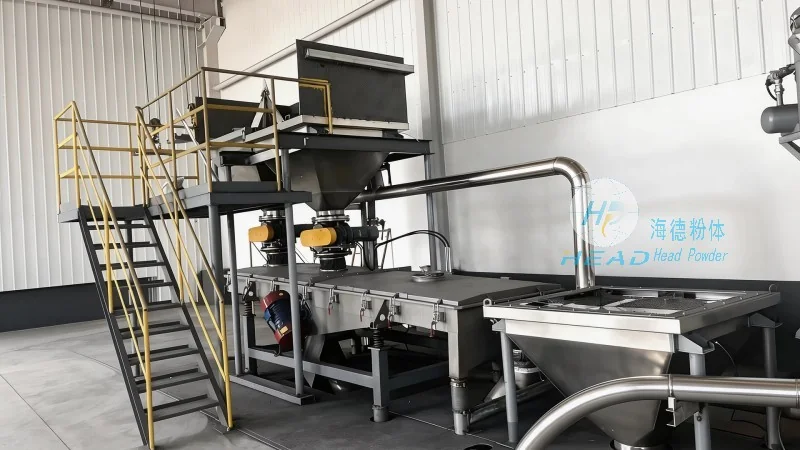
Working Principle of Tonne Bag Material Pneumatic Conveying Equipment
The tonne bag material pneumatic conveying equipment operates on the fundamental principle of using air to transport bulk materials from their original packaging (tonne bags) to a designated destination. This system typically employs a combination of vacuum or pressure to create a flow of air that draws or pushes the material through a network of pipes. The process begins with the material being loaded into a tonne bag, which is then connected to the inlet of the conveying system. As the air is introduced, it creates a low-pressure zone (in vacuum systems) or high-pressure zone (in pressure systems), causing the material to be entrained and carried along the pipeline. The equipment is equipped with specialized components such as rotary valves, filters, and dust collectors to ensure efficient and clean material transfer. The entire system is designed to handle a wide range of materials, including powders, granules, and bulk solids, with minimal loss and contamination. The working principle is based on the physics of fluid dynamics, where the air acts as a carrier medium, enabling the material to be transported without direct contact with the conveying equipment, thus reducing wear and tear and improving overall efficiency.
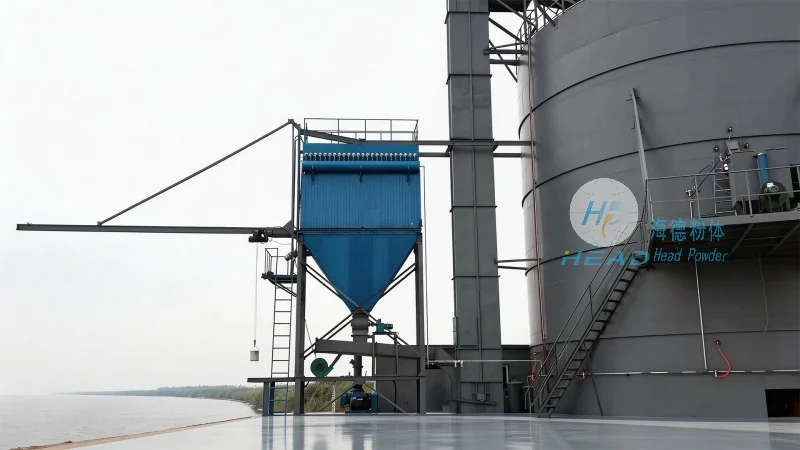
Key Features of Tonne Bag Material Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd.'s tonne bag material pneumatic conveying equipment is characterized by several notable features that enhance its performance and usability. Firstly, the system offers high efficiency in material handling, capable of processing large volumes of tonne bag materials in a short period. This is achieved through optimized air flow management and robust conveying components that ensure consistent and reliable operation. Secondly, the equipment is designed with a focus on environmental friendliness, incorporating dust collection and filtration systems that minimize air pollution and comply with environmental regulations. This feature is particularly important for industries where air quality is a concern, such as food processing, pharmaceuticals, and chemical manufacturing. Thirdly, the system exhibits excellent adaptability, as it can be customized to handle different types of tonne bag materials, including various particle sizes, densities, and moisture contents. The modular design allows for easy integration with existing production lines, reducing installation time and costs. Additionally, the equipment is equipped with advanced control systems that provide real-time monitoring and adjustment of operational parameters, ensuring optimal performance and preventing system failures. Another key feature is the low maintenance requirement, as the design minimizes moving parts and uses durable materials that resist corrosion and wear. This reduces downtime and maintenance costs, making the equipment a cost-effective solution for long-term material handling needs. Finally, the system is built with safety in mind, incorporating features such as emergency shut-off valves and overpressure protection to prevent accidents and ensure safe operation in industrial environments.
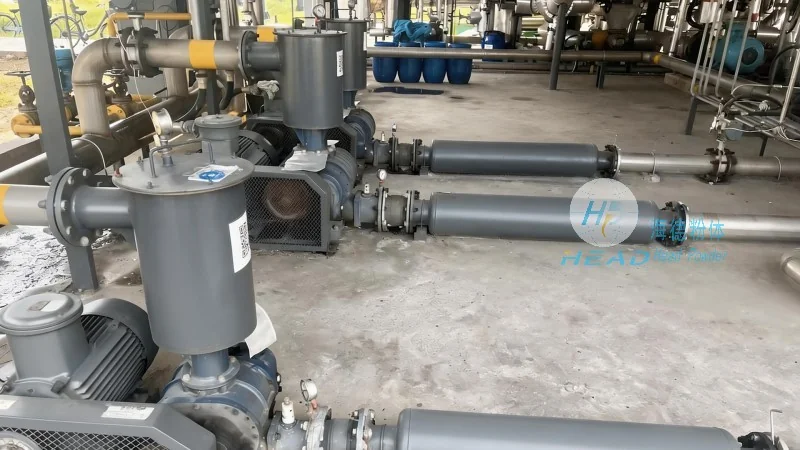
Application and Benefits in Industrial Settings
The tonne bag material pneumatic conveying equipment developed by Shandong HeadPowder Engineering Co., Ltd. finds extensive applications across various industries, including food and beverage, pharmaceuticals, chemicals, and mining. In the food industry, for example, the equipment is used to transport ingredients like flour, sugar, and spices from tonne bags to processing lines, ensuring hygienic and contamination-free handling. The pharmaceutical sector benefits from the system's ability to handle sensitive materials, as it maintains strict cleanliness and prevents cross-contamination. In the chemical industry, the equipment is employed to transport bulk chemicals, such as powders and granules, from storage to production areas, enhancing safety and efficiency. The mining industry utilizes the system for transporting raw materials like ores and minerals from tonne bags to processing plants, reducing manual labor and improving operational efficiency. The benefits of using this equipment include increased productivity, reduced labor costs, and improved product quality. By automating the material handling process, companies can achieve higher throughput and lower operational costs, while maintaining compliance with industry standards and regulations. The system's reliability and durability also contribute to long-term cost savings, as it requires minimal maintenance and has a long service life. Overall, the tonne bag material pneumatic conveying equipment is a versatile and efficient solution for industries that rely on bulk material handling, providing a reliable and sustainable method for transporting tonne bag materials.




