Automatic bulk bag unloading and pneumatic conveying equipment is a specialized system designed to efficiently handle the transfer of bulk materials from large flexible containers, such as super sacks or bulk bags, into processing facilities or storage areas. This equipment plays a crucial role in industries like food processing, chemical manufacturing, pharmaceuticals, and mining, where handling large volumes of powders and granules is essential for smooth production operations.
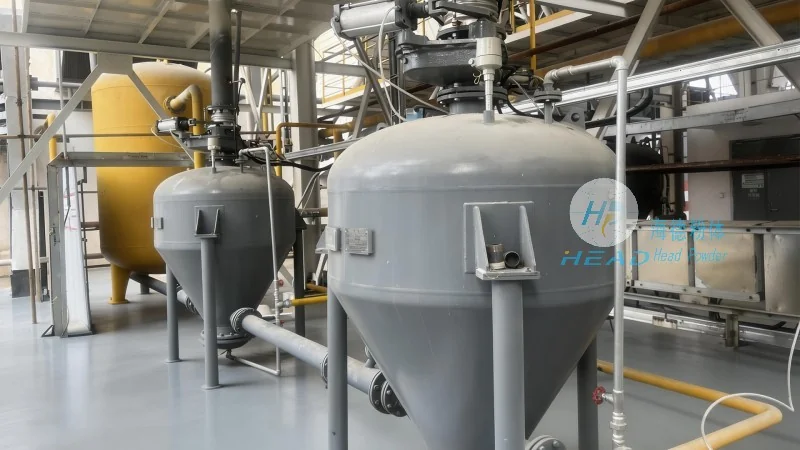
Overview of the Equipment System
The system typically consists of several key components that work in tandem to achieve seamless material transfer. These components include a bulk bag unloader, a hopper or surge bin, a pneumatic conveying pipeline, and a control system. The bulk bag unloader is responsible for opening the bag, discharging the material into the hopper, and then sealing the bag for disposal or reuse. The hopper acts as a buffer to regulate the flow of material into the conveying system, preventing overloading or underflow. The pneumatic conveying pipeline uses compressed air or other gases to transport the material from the hopper to the desired destination, such as a silo, mixer, or processing unit. The control system monitors and regulates the entire process, ensuring optimal performance and safety.
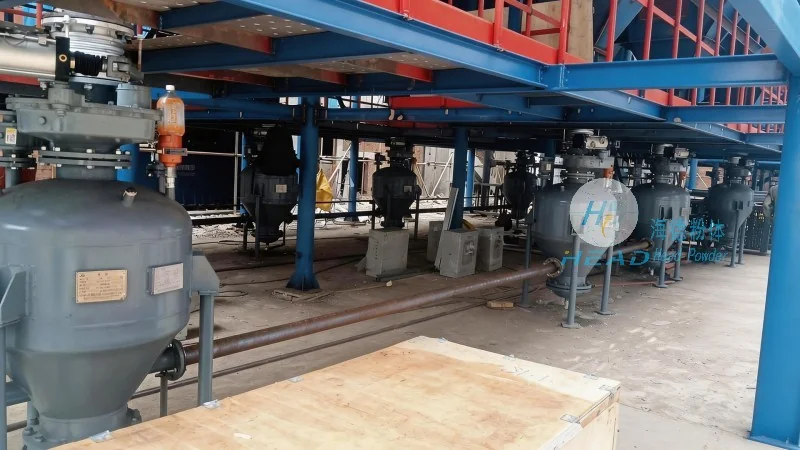
Working Principle of the Equipment
The working principle of automatic bulk bag unloading and pneumatic conveying equipment involves a series of automated steps that ensure efficient and safe material handling. The process begins with the placement of a bulk bag onto the unloader's frame. The unloader then uses mechanical or pneumatic mechanisms to open the bag's top, allowing the material to flow into the hopper. Simultaneously, the control system activates the conveying system, which draws the material from the hopper through the pipeline using compressed air. The air flow is controlled to maintain a consistent pressure and velocity, ensuring the material is transported without clogging or degradation. The material is then discharged from the pipeline into the receiving vessel, where it is stored or processed. After the bag is emptied, the unloader seals the bag and prepares it for removal, completing the cycle.
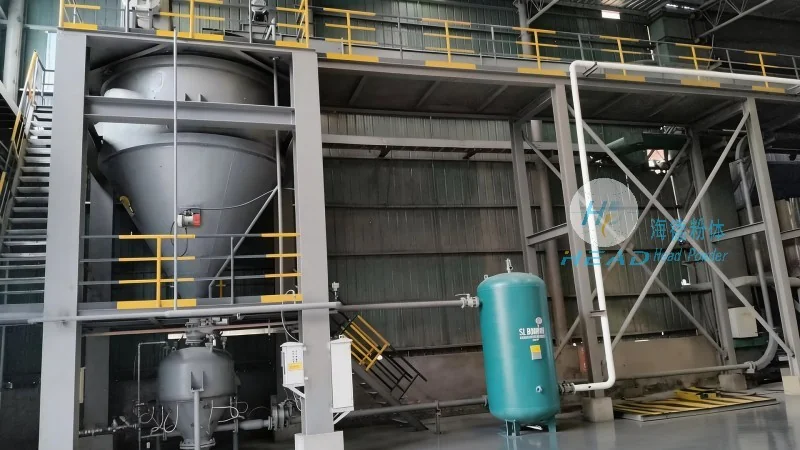
Key Features and Advantages
Automatic bulk bag unloading and pneumatic conveying equipment offers several key features and advantages that make it an ideal solution for industrial material handling. One of the primary advantages is its ability to handle large volumes of bulk materials with minimal human intervention, reducing labor costs and improving operational efficiency. The system is designed to be highly reliable and durable, with components that can withstand the rigors of continuous operation in demanding industrial environments. Another significant feature is its ability to maintain product integrity, as the equipment is designed to minimize material exposure to air, moisture, and contamination, which is critical for sensitive products like food, pharmaceuticals, and chemicals. The system also offers flexibility in terms of material handling, as it can be configured to handle a wide range of particle sizes and flow rates. Additionally, the equipment is equipped with safety features, such as pressure relief valves and emergency stop buttons, to ensure safe operation and protect personnel from potential hazards.
Application Scenarios
Automatic bulk bag unloading and pneumatic conveying equipment is widely used in various industries due to its versatility and efficiency. In the food industry, it is commonly used to handle ingredients like flour, sugar, and spices, ensuring a clean and hygienic transfer process. In the chemical industry, it is used to transport powders and granules such as fertilizers, pigments, and coatings, which require precise control over flow and moisture content. The pharmaceutical industry also relies on this equipment to handle active pharmaceutical ingredients (APIs) and excipients, where contamination control and product purity are paramount. Additionally, the mining and mineral processing industries use the system to transport raw materials like ores and minerals from bulk bags to processing plants, improving the overall efficiency of material handling operations.
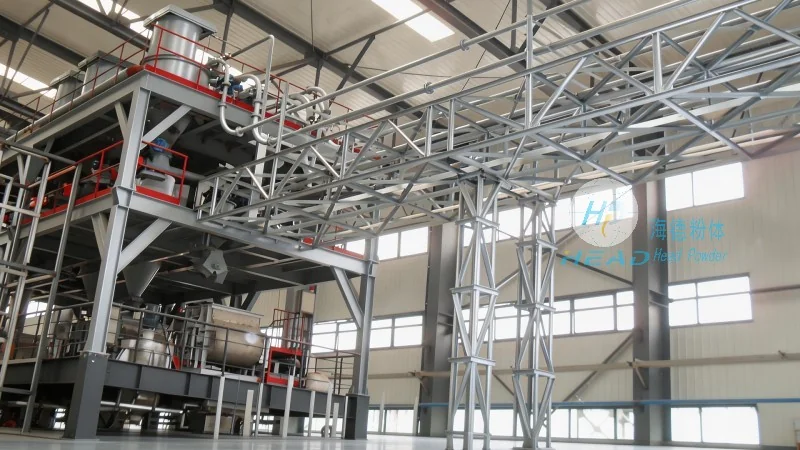
Company Information and Service
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of bulk bag unloading and pneumatic conveying equipment. With years of experience in the industry, HeadPowder specializes in designing and manufacturing high-quality, customized solutions tailored to the specific needs of its clients. The company's products are known for their durability, efficiency, and reliability, making them a trusted choice for industries worldwide. HeadPowder's team of engineers and technicians work closely with clients to understand their material handling challenges and develop solutions that meet their requirements. The company also provides comprehensive after-sales support, including installation, maintenance, and training, to ensure that clients can maximize the performance and lifespan of their equipment. HeadPowder is committed to providing innovative and sustainable solutions that help its clients improve their operational efficiency and reduce costs.




